CONNECTING APPAREL EMPOWERING TOMORROW
BUILDING THE FUTURE OF APPAREL
Product Development
From concept to creation
Material Sourcing
Right materials. Better products
Manufacturing
Reliable production partners
Quality Assurance
Standards you can trust
Logistics & Shipping
Global delivery support
Market Insights
Data for smarter decisions
Instant Access to Mission-Critical Engines
Direct cryptographic ingress to verified manufacturing capacity, raw material inventories, and quality control gates.
Fabric Marketplace
Physical GSM swatches, laboratory yarn counts & certified mill roll inventory.
Audited Mill Network
Physically inspected production lines, machine capacity & compliance dossiers.
Merchandising Workspace
13-stage order execution pipeline, tech-pack dossiers & mill telemetries.
Smart RFQ Matching
Algorithmic capacity fit, FOB target optimization & structured bid comparison.
Sample Lab-Dip R&D
D65 spectrophotometer spectral curves, lab-dip approvals & strike-off tracking.
Quality & AQL 1.5 Gate
Standardized defect classification, physical QA checkpoints & gate certificates.
Zero Trust Enclave
Verified factory performance history, quality records, transaction evidence & trust controls.
Production RFQ Ingress
Structured specification builder, target costing, MOQ logic & CAD ingress.
Do It Right the First Time.
Leadirftex was founded to transform the global textile and apparel ecosystemโfrom frontline workers on the factory floor to the global buyers sourcing finished goods.
At our core lies a single, guiding principle: Do It Right the First Time. This is far more than a quality control slogan; it is an organizational culture built on personal ownership. Every operator, technician, manager, and supplier must clearly understand their role, possess the training to execute it properly, and take genuine pride in getting it right from the start.
True quality originates with the individual performing the task. Principles like self-inspection, workplace safety, operational discipline, and continuous improvement should define daily operationsโnot serve as temporary measures trotted out for buyer audits.
Leadirftex bridges practical industry expertise with structured training, lean manufacturing principles, and modern digital automation. We empower factories to sustainably enhance product quality, throughput, and technical capability.
Powered by LX Intelligence, our platform delivers transparent, actionable analytics anchored in enterprise-grade data security. By bringing unprecedented visibility to end-to-end manufacturing processes, we help facilities uncover bottlenecks, eliminate hidden waste, and make informed decisions that foster a resilient, accountable ecosystem.
Our mission extends well beyond simply matching buyers with manufacturers. We are committed to building an apparel industry that is safer, smarter, and consistently capable of delivering right-first-time quality. In doing so, we help manufacturers secure long-term buyer trust while creating sustainable economic value for the workforce behind them.
To further support this community, Leadirftex also offers an accessible, zero-cost talent-matching layerโconnecting skilled professionals with career pathways in an evolving global workforce.
The Interchain Workflow Architecture
End-to-end industrial execution journey connecting upstream specifications to automated factory-floor verification gates.
Requirement Intake Protocol
Visual placeholder for intake specification ingestion, pattern archives normalization, and preliminary physical constraint verification.
Modular Engines Built for Precision Textile Execution
Four decoupled, high-performance engines working synchronously across your supply chain to eliminate manufacturing defects and settlement friction.
Neural Spec Matcher
Transforms complex multi-layered tech-packs into machine-readable yarn, weaving, and dying constraints with 99.4% parsing accuracy across 24 textile standards.
SpectroCloud Lab-Dip Engine
Cloud-integrated spectrophotometer lab-dip verification under D65, TL84, and CWF light sources with automated ฮE color difference calculation.
Interchain Smart Escrow
Multi-signature milestone financial escrow locking funds until certified third-party physical inspection reports and IoT loom data criteria are satisfied.
IoT Loom Mesh Network
Real-time sensor telemetry streaming from certified factory floor machinery tracking pick counts, loom RPM, tension variation, and ambient humidity.
Live 3D Fashion Design Interactive Showcase
Explore production-ready CAD patterns, Clo3D digital twins, and certified tech-packs with real-time FOB pricing and multi-mill manufacturing capacity.
ALL YOUR STYLES ARE HERE
Verified Interchain Corporate Signatures
Enterprise cryptographic identity and direct communication credentials for Leadirftex executive leadership, laboratory testing directors, mill compliance auditors, and trade settlement officers.
What Makes Leadirftex Beloved by Over 1,200 Global Enterprises?
Connect Your Supply Chain to the Interchain Infrastructure
Whether you are an international fashion house requiring guaranteed production execution or an accredited mill seeking high-volume enterprise orders, Leadirftex delivers end-to-end contractual certainty.
Creative Vision to Industrial Scale.
Bridge high-fashion runway couture and parametric Clo3D CAD blueprints directly to Tier-1 mill loom handoff. Explore physical swatches, verified tech packs, and automated FOB cost modeling.
Interactive Atelier Tablet Collection & Sample Lab
Touch, swipe, and scroll through verified couture collections, Clo3D digital twins, and physical fabric swatches. Tap any sample to inspect 3D parameters or order lab swatches.
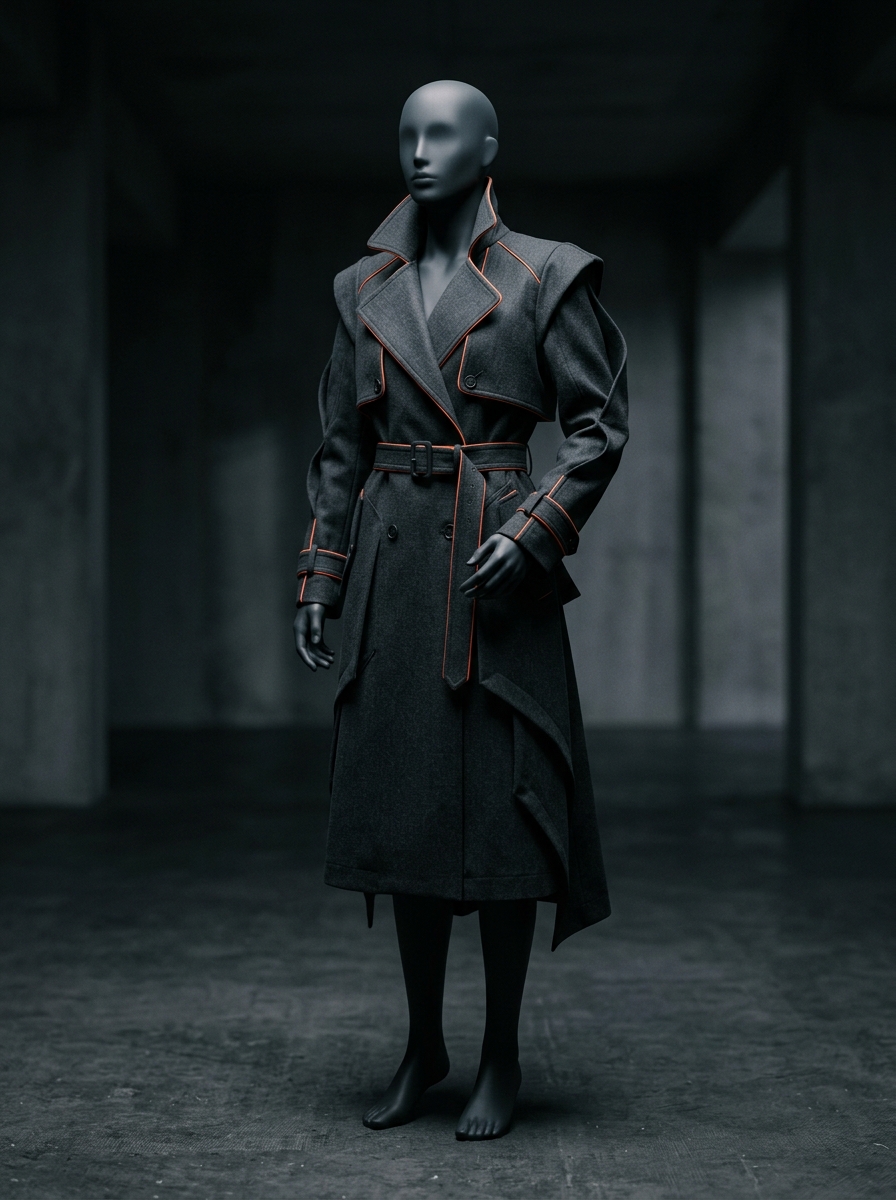
LDF-FW26-088: Architectural Hybrid Trench
14.5oz Japanese Wool-Cordura hybrid with articulated 3D sleeve darts, waterproof closures, and modular utility cargo panels.
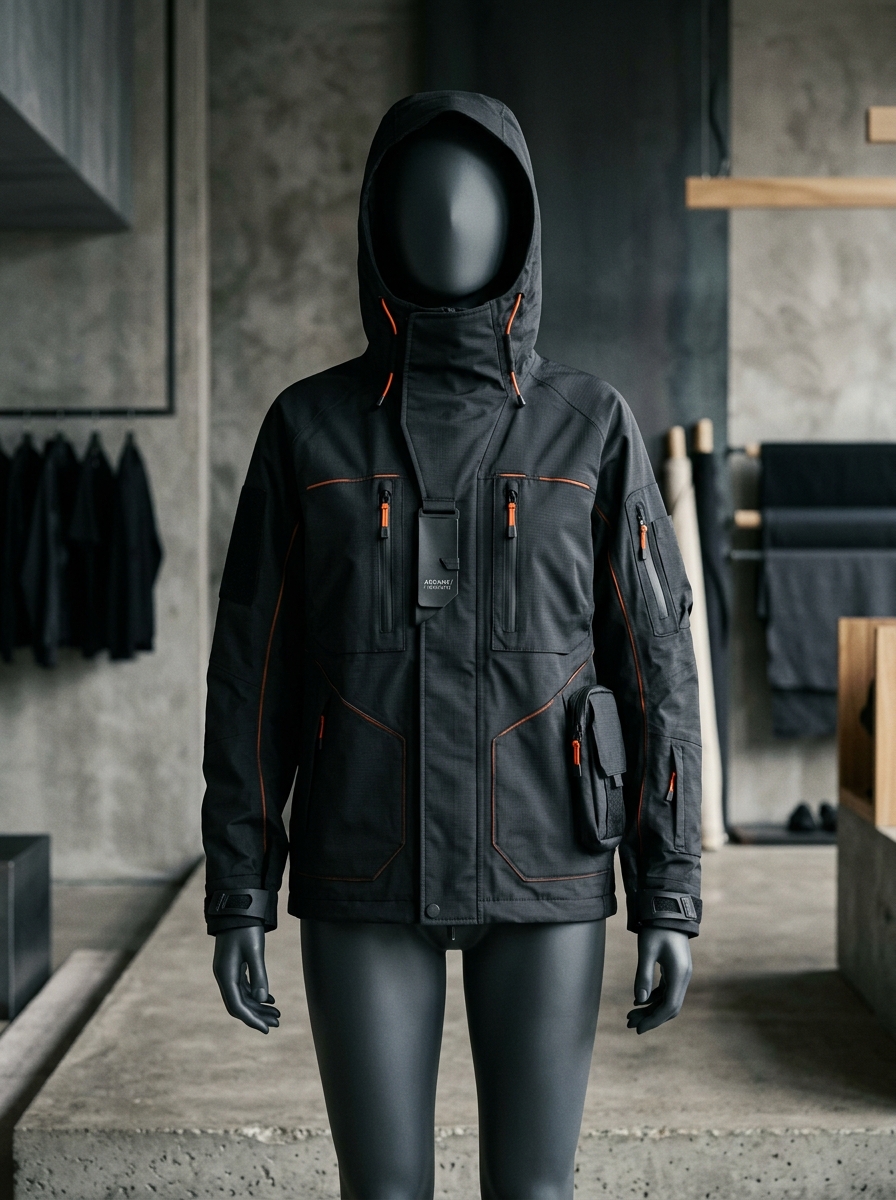
LDF-TECH-109: Storm-Shield Modular Parka
3-Layer bonded ripstop nylon with Fidlock magnetic storm closures and laser-welded heat-sealed seam tapes.
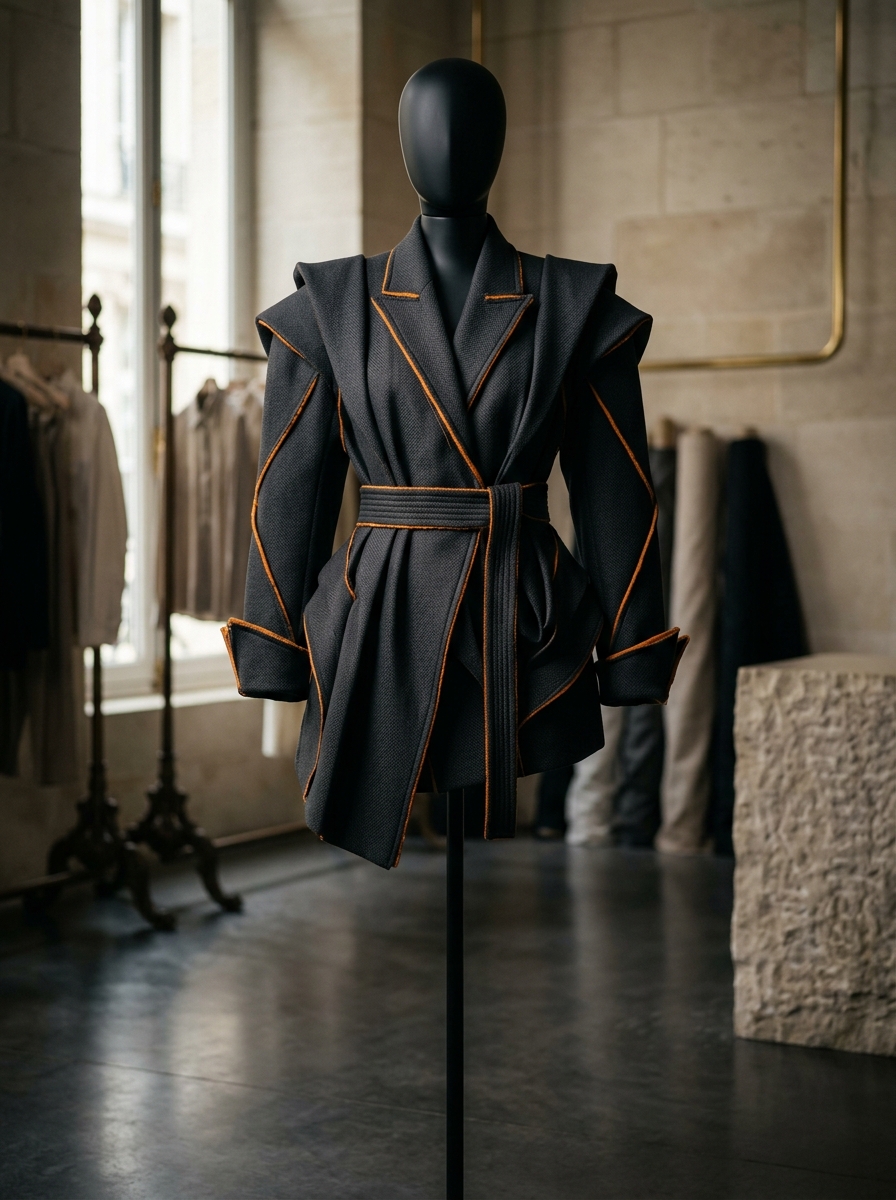
LDF-BIO-042: Sculptural Pleat Kimono Jacket
Fermented microbial bio-silk and organic cotton blend with sculptural architectural pleats and plant-derived charcoal pigment.
LDF-FW26-003: Double-Breasted Raw Edge Coat
Heavyweight Melton wool and recycled cashmere blend with raw laser-finished edges and Cupro anti-static lining.
LDF-ART-771: Parametric Fluid Silhouette Dress
Algorithmic drape geometry rendered in 120 FPS GPU cloth simulation. Liquid silk satin with elastomeric micro-filaments.
Latest Fashion Design Masonry Discovery
Pre-screened seasonal garments ready for immediate pattern nesting and loom execution.
Architectural Pleated Shroud
Double-layered bio-cellulose fabric engineered for zero-gravity drape dynamics and robotic needle placement.
Carbon-Weave Kinetic Parka
Modular weather-adaptive shell with graphene internal heating paths and electromagnetic seam seals.
Mycelium Structured Tunic
100% compostable bio-leather grown in closed-loop vats, dyed with natural fermented indigo and tannin.
Seasonal Color Palette & Surface Material Forecast
Color trend telemetry correlated with mill dyeing recipes and spectrophotometer spectral pass tolerances.
From Concept Sketch to Tier-1 Mill Loom Handoff
A rigorous 6-step computational gate ensuring 100% pattern integrity before yarn ever touches a warp beam.
Meet Leadirftex Verified Couturiers
Accredited pattern engineers and couture directors ready to take your seasonal brief to physical production.
Specializing in structural tailoring, hybrid Cordura outerwear, and Clo3D avatar drape optimization for luxury labels.
Technical outerwear pioneers utilizing bonded waterproof textiles, ultrasonic seam welding, and Fidlock integration.
Zero-waste computational patternmakers developing fermented microbial bio-cellulose garments and circular knitwear.
Ready to Translate Designs into Commercial Production?
Continue the seamless workflow across the 21-Hub Interchain. Source matched fabrics in Hub 05, order certified lab-dip swatches in Hub 11, or broadcast an RFQ in Hub 12.
LDF-FW26-088: Architectural Hybrid Trench
Japanese Wool-Cordura hybrid with articulated 3D sleeve darts, waterproof closures, and modular utility cargo panels.
Textile & Garment Learning Academy.
Professional engineering knowledge, production-floor practical mastery, work-study optimization, and accredited technical certifications for the global apparel ecosystem.
Core Learning Categories & Engineering Disciplines
Comprehensive curriculum developed by master textile technologists and industrial engineering leaders.
Textile Engineering
Fiber morphology, yarn count mathematics (Ne/Nm), woven/knitted fabric structures, and ASTM testing.
Garment Technology
Sewing machine kinematics, stitch types (ISO 4915), pattern engineering, and CAD grading.
Production Floor
Daily pitch time, hourly production board monitoring, bottle-neck clearing, and workstation layout.
Industrial Engineering
Time and motion study, standard minute value (SMV/SAM), line balancing efficiency, and GSD analysis.
Quality & Inspection
ISO 2859-1 AQL sampling plans, 4-point fabric inspection, inline audit checklists, and defect taxonomy.
Manufacturing Operations
Lean 5S manufacturing, cellular production systems, total productive maintenance (TPM), and quick changeovers.
Professional Training
Operator upskilling programs, shift supervisor leadership academies, and mechanical maintenance bootcamps.
Verified Certification
Formal capability assessments, practical floor examinations, and verified industry credentials.
High-Impact Technical Courses & Masterclasses
Structured modules designed for factory professionals, industrial engineers, and quality directors.
LEVEL: ADVANCED
Parametric Clo3D Digital Twin & Stress Analysis
Master 120 FPS GPU cloth simulation, avatar fit grading across European and US sizing standards, and computerized seam tension analysis.
LEVEL: INTERMEDIATE
High-Speed Sewing Line Balancing & SAM Math
Algorithmic operator allocation, bottleneck clearing techniques, and Standard Allowed Minute (SAM) calculation for multi-style lines.
LEVEL: PROFESSIONAL
ASTM/AATCC Textile Physical & Chemical Testing
Comprehensive laboratory protocols for tensile tear strength (ISO 13934), pilling resistance (Martindale), and spectrophotometer Delta-E color fastness.
Textile Engineering Fundamentals
Scientific exploration of natural and synthetic polymers, yarn spinning physics, and structural fabric geometry.
Garment Construction & Technology
Precision stitch mechanics, needle heat thermodynamics, automated CAD cutting, and industrial seam integrity.
Production-Floor Practical Operations & Line Balancing
Real-world manufacturing decisions on the sewing line. Moving beyond textbook theory into active workstation pacing, operator buffer management, and live hourly output tracking.
Industrial Engineering (IE) Methodologies
Time and motion analysis frameworks used across Tier-1 garment manufacturing hubs.
Real Industry Case Studies: Problem โ Root Cause โ Resolution
Authentic production-floor challenges resolved by Leadirftex senior technical auditors.
Resolving Severe Spirality in 240 GSM Single Jersey
Post-wash side seam twisting exceeded 9% tolerance, causing buyer audit rejections.
Residual torque from unbalanced single-ply rotor yarn during circular knitting without heat-setting.
Switched to S+Z dual feeder alternating loops and increased stenter vacuum steaming to reset yarn tension.
Needle Heat Puckering on High-Density Micro-Taffeta
Puckering along back yoke seam after high-speed 4,500 RPM lockstitch operation.
Frictional needle temperature exceeded 220ยฐC, melting synthetic filament fibers at needle penetration.
Installed pneumatic needle cold-air coolers and reduced sewing speed to 3,600 RPM with Teflon-coated needle size 65/9.
Boosting 5-Pocket Denim Line Efficiency from 51% to 74%
Severe bottleneck at back pocket decorative embroidery and waistband attachment stations.
Unequal cycle times: Pocket station SAM was 2.4x higher than neighboring flatlock operations.
Implemented dual automatic template jig clamp sewing for pockets, reducing SAM from 1.8 mins to 0.45 mins.
Professional Career Learning Pathways
Step-by-step competency roadmaps guiding learners from baseline principles to senior technical qualification.
Verified Industry Accreditations & Exams
Formal qualification programs recognized by international apparel manufacturing groups, export councils, and testing houses.
Certified Textile Technologist (CTT)
Covers physical testing, yarn science, and ASTM fabric inspection.
Certified Industrial Engineer (CIE)
Focuses on line balancing, SAM calculation, and GSD work measurement.
AQL Quality Assurance Auditor
ISO 2859-1 sampling plans, defect taxonomy, and CAPA audits.
Clo3D Master Pattern Engineer
Parametric grading, avatar drape verification, and Gerber DXF export.
Meet Leadirftex Master Instructors
Learn directly from seasoned production directors, textile researchers, and industrial engineers.
Prof. M. Rahman, Ph.D.
Engr. S. K. Roy, M.Sc.
N. L. Chen, Master Tailor
How Learning Connects to the 21-Hub Platform
Industrial capability acquired in Hub 02 translates directly into material selection, sampling precision, factory allocation, and quality verification.
Automated Machinery, Equipment & Spare-Parts Reserve Network
Authoritative industrial asset and equipment platform interconnecting bonded machine manufacturers, factory installations, serial tracking, OEM warranty lifecycle, spare-parts directories, and real-time Bangladesh local reserves.
Machine Company Bonding Authorization & Use-Lifetime Support
Formal business authorization architecture legally bonding machinery manufacturers to maintain guaranteed Bangladesh local spare-parts reserves, certified field engineering coverage, and warranty support for the entire operating lifecycle of supplied equipment.
Controlled Machine-Support Relationship Chain
Bonded OEM
Service Partner
Smart Lockstitch
Line 12 Station 08
Registered Asset
10-Yr Parts Bond
Machine Use-Lifetime Support Standards
When a factory purchases a machine through Leadirftex, the machine company is contractually bonded to identify and guarantee all consumable and structural spare parts for a minimum 10-year operating horizon (30,000 continuous production hours).
| Operating Lifecycle | 10 Years / 30,000 Operating Hours |
|---|---|
| Consumable Parts Guarantee | Continuous 24-hr local supply (Needles, loopers, blades) |
| Critical Spares Requirement | Motors, control boxes, mainboards held in Dhaka reserve |
| Service Response SLA | Within 4 hours for line-stop emergency dispatches |
Foreign Company Identity & Privacy Protection
In accordance with Leadirftex Security & Data Privacy standards, foreign corporate representative identity data and credentials are kept strictly confidential and masked in all public interfaces.
| Identity Verification Status | โ Foreign Company โ Identity Verified |
|---|---|
| Authorized Representative | Kenji Takahashi (Director of South Asia Operations) |
| Signatory Credential | Rep ID: *******4821 [Encrypted & Verified by Leadirftex] |
| Privacy Standard | Zero raw passport exposure in frontend, URLs, or API responses |
Bangladesh Local Reserve & Spare-Parts Continuity Dashboard
Reconciles mandatory local reserve quotas against active warehouse allocations across Dhaka and Chittagong depots. Prevents production halts by identifying stock deficits before critical parts run out.
| Machine Model | Component Name | Part Code | Required Reserve | Currently Reserved | Available in Depot | Reserve Gap | Depot Location | Reserve Health |
|---|---|---|---|---|---|---|---|---|
| Juki DDL-9000C | DLC Needle Bar Assembly | JK-SP-DDL-NDL-01 |
300 Units | 120 Units | 330 Units | 0 (Surplus +30) | Dhaka Depot, Bay 4B | HEALTHY |
| Mayer & Cie Relanit 3.2 | Relanit Sinker Ring Set | MC-SP-REL-SINK-48 |
120 Sets | 35 Sets | 145 Sets | 0 (Surplus +25) | Chittagong Port Hub | HEALTHY |
| Gerber Paragon VX | Solid Carbide Blade (72mm) | GB-SP-PAR-BLD-72 |
200 Blades | 80 Blades | 240 Blades | 0 (Surplus +40) | Dhaka Central Logistics | HEALTHY |
| Juki DDL-9000C | Titanium Full-Rotary Hook | JK-SP-HOOK-ROT-9 |
50 Units | 65 Units | 25 Units | -25 Shortfall | Dhaka Depot, Bay 2A | REORDER DISPATCHED |
| Yamato VG2700 | Differential Feed Looper | YM-SP-VG-LOOP-04 |
150 Sets | 45 Sets | 165 Sets | 0 (Surplus +15) | Dhaka Depot, Bay 1C | HEALTHY |
Machine Catalog & Database Auto-Import Console
Structured workflow allowing bonded machine manufacturers to upload or scan machine catalogs, automatically extracting model parameters, technical specifications, and authorized A-to-Z spare-parts directories into the Interchain registry.
Catalog Submission & Structured Extraction
Upload an OEM machine catalog, enter a catalog identifier code, or scan a catalog QR/Barcode to initiate automated schema validation. The system parses brand, machine type, model series, and compatible spare-parts matrices.
Juki DDL-9000C Series Smart Lockstitch
| OEM Brand | Juki Corporation (Japan) |
|---|---|
| Machine Type | Industrial High-Speed Direct-Drive Lockstitch |
| Model Series | DDL-9000C-SMS / FMS / WB |
| Applicable Parts Catalog | 48 Verified SKUs Mapped |
| Bangladesh Reserve Status | Mandatory Reserve Established (Dhaka Hub) |
| Validation Standard | ISO 9001:2015 & Juki OEM Authorized |
Machine Company Weekly Stock Update & Controlled Access
Authorized interface for machine companies to report current physical stock and reserved allocations. Enforces strict backend permission boundaries preventing unauthorized edits to historical records or calculated balances.
Stock Update Console (Week 37 - 2026)
Restricted Machine Company Permissions
To guarantee audit integrity, machine companies operate under strict role-based access control. Destructive edits and retroactive alterations are prohibited:
| Historical Submissions | Immutable โ Overwrites blocked; revisions append new audit entries |
|---|---|
| Verification Seals | System Controlled โ Only Leadirftex Verifiers can sign status |
| Machine Serial Registry | Read Only โ Serial ownership and factory links cannot be changed by OEM |
| Cross-OEM Isolation | Strict Sandbox โ OEMs cannot view or modify competitor inventories |
| Authoritative Calculation | Automatic โ Available Balance calculated server-side only |
Immutable Weekly Submission Audit History
โ AUDIT LOG SIGNED BY LEADIRFTEX| Cycle | Submission Date | Part Code | Reported Stock | Reserved | Available Balance | Authorized Submitter | Status |
|---|---|---|---|---|---|---|---|
WK-36-2026 |
04 Sep 2026 | JK-SP-DDL-NDL-01 |
450 Units | 120 Units | 330 Units | Engr. K. Rahman (Juki BD #41) | LEADIRFTEX VERIFIED |
WK-35-2026 |
28 Aug 2026 | MC-SP-REL-SINK-48 |
180 Sets | 35 Sets | 145 Sets | T. Weber (Mayer Liaison) | LEADIRFTEX VERIFIED |
WK-35-2026 |
28 Aug 2026 | GB-SP-PAR-BLD-72 |
320 Blades | 80 Blades | 240 Blades | S. Chowdhury (Gerber Tech) | LEADIRFTEX VERIFIED |
WK-34-2026 |
21 Aug 2026 | JK-SP-HOOK-ROT-9 |
90 Units | 65 Units | 25 Units (Low) | Engr. K. Rahman (Juki BD #41) | LEADIRFTEX VERIFIED |
Machine Company Network & Authorized Suppliers
Direct manufacturer partnerships verifying genuine machinery provenance, certified local service engineering networks, and authentic OEM spare-parts supply lines.
Juki Corporation
Global leader in smart industrial sewing technology, automated lockstitch units, overlockers, and programmable pattern sewing machines with NFC digital control.
| Installations | 840+ Units across Bangladesh |
|---|---|
| Warranty Coverage | 3 Years Direct Comprehensive |
| Parts Depot | Dhaka Central Warehouse (1,200 SKUs) |
Mayer & Cie. GmbH
High-precision circular knitting machinery with patented relative technology, electronic jacquard systems, and spun-knit elastomer synchronization.
| Installations | 160+ Units in Premium Mills |
|---|---|
| Warranty Coverage | 2 Years Mechanical & Cam Box |
| Parts Depot | Regional Hub Frankfurt & Chittagong |
Gerber Technology (Lectra)
Industrial automated cutting room solutions, high-ply automated spreading tables, Paragon CNC cutters, and cloud-integrated nesting software suites.
| Installations | 92+ Cutter Lines in Operation |
|---|---|
| Warranty Coverage | 2 Years CNC Motion & Vacuum |
| Parts Depot | Dhaka Technocenter (Carbide Blades) |
Machine Asset Profile & Unique Serial Tracking
Trace a machine's full lifecycle from OEM production in Japan/Germany through factory commissioning, maintenance records, warranty validity, and compatible replacement parts.
Juki DDL-9000C-SMS Intelligent Lockstitch
JK-2024-88492-BD
โ WARRANTY ACTIVE (2027)
Dec 2023
Jan 2024
14 Jan 2024
Exp: Jan 2027
Hook Replaced
100% In Stock
Technical Specifications
| Model Code | DDL-9000C-SMS-WB (Direct Drive) |
|---|---|
| Max Speed | 5,000 Stitches / Min (SPM) |
| Needle Bar Stroke | 30.7 mm (DBx1 #9 to #18) |
| Lubrication | Semi-dry oil head (zero fabric staining) |
| IoT Capability | NFC digital parameter setting & USB |
| Operating Hours | 4,820 Hours logged (Continuous) |
Factory Provenance & Service State
| Installed Facility | Horizon Knitwear & Apparels Ltd. |
|---|---|
| Location on Floor | Campus 2, Floor 3, Stitching Line 12, Station 08 |
| Primary Product Line | Heavyweight Fleece & Hoodies (Hub 16) |
| Next Preventive Service | 5,000-hr oil drain & calibration (Due in 180 hrs) |
| Authorized Servicer | Juki Bangladesh Service Center Ltd. |
| Assigned Technician | Engr. Tariq Mahmud (Cert #JK-881) |
Factory Machine Fleet Distribution & Warranty Registry
Real-time status overview of installed machine populations across audited manufacturing facilities in the Interchain network.
| Factory / Location | Machine Model | Serial Number | Commission Date | Warranty Term | Service Status | Health Score | Actions |
|---|---|---|---|---|---|---|---|
| Horizon Knitwear Ltd. (Line 12) | Juki DDL-9000C Lockstitch | JK-2024-88492-BD |
14 Jan 2024 | Active (Jan 2027) | Normal / Operating | 98.4 / 100 | |
| Horizon Knitwear Ltd. (Knitting Bay) | Mayer & Cie Relanit 3.2 II | MC-2023-11094-DE |
08 Nov 2023 | Active (Nov 2025) | Service Due in 12 Days | 92.0 / 100 | |
| EchoTex Green Plant (Cutting 01) | Gerber Paragon VX Cutter | GB-2025-04419-US |
02 Feb 2025 | Active (Feb 2027) | Normal / Calibrated | 99.1 / 100 | |
| Beximco Industrial Park (Line 4) | Yamato VG2700 Cylinder Flatlock | YM-2024-55021-JP |
19 Jun 2024 | Active (Jun 2026) | Normal / Active | 96.8 / 100 | |
| DBL Group Campus (Dyehouse) | Tonello ECOBIP Dyeing Drum | TN-2022-90112-IT |
10 Mar 2022 | Expired (Mar 2025) | Under Maintenance | 84.5 / 100 |
Spare Parts Availability & A-to-Z Applicable Directory
Complete applicable spare-parts catalog authorized by machine manufacturers with real-time stock balances across regional depots.
DLC Needle Bar Assembly
JK-SP-DDL-NDL-01Diamond-Like Carbon (DLC) coated needle bar for DDL-9000C series. Withstands 5,000 SPM with zero oiling requirement.
Relanit 3.2 II Sinker Ring Set
MC-SP-REL-SINK-48Precision hardened steel sinkers with relative movement geometry for flawless loop formation and lycra plating.
Solid Carbide Reciprocating Blade
GB-SP-PAR-BLD-72Ultra-hard micro-grain tungsten carbide cutting blade for Paragon VX cutters. Cuts up to 72mm compressed fabric plies.
Differential Feed Looper Assembly
YM-SP-VG-LOOP-04Precision titanium-nitride coated lower looper for Yamato VG2700 flatlock machines. Prevents skipped stitches at 6,500 SPM.
Titanium Full-Rotary Hook
JK-SP-HOOK-ROT-9Hardened titanium nitride rotary hook with micro-groove oil circulation for ultra-fine thread tension control.
Optical Thread Tension Sensor
OM-SP-OPT-TEN-12Sub-millisecond optical infrared sensor module detecting micro-breaks and measuring thread delivery tension in grams.
Part Code Scan & Barcode / QR Auto-Lookup
Simulate real-time hardware scanning or enter OEM part numbers to instantly fetch engineering datasheets, compatible models, and regional stock allocations.
DLC Needle Bar Assembly
JK-SP-DDL-NDL-01| Manufacturer | Juki Corporation (Tokyo, Japan) |
|---|---|
| Compatible Machines | DDL-9000C, DDL-8700-7, DDL-900B |
| Warehouse Location | Dhaka Central Logistics Depot, Bay 4B |
| Total Physical Stock | 450 Units |
| Reserved for Work Orders | 120 Units |
| Available Net Balance | 330 Units Ready to Ship |
Machine Service & Spare-Part Traceability Records
Chronological record linking maintenance events directly to machine serial numbers, certified technician signatures, and consumed spare-part serial allocations.
| Event ID | Machine Serial | Facility / Line | Issue Diagnosis | Part Replaced | Qty Used | Service Date | Status |
|---|---|---|---|---|---|---|---|
EV-2026-0411 |
JK-2024-88492-BD | Horizon Knitwear (Line 12) | Rotary hook thread clearance backlash | Titanium Rotary Hook (JK-SP-HOOK-ROT-9) |
1 Unit | 04 Sep 2026 | RESOLVED & VERIFIED |
EV-2026-0389 |
MC-2023-11094-DE | Horizon Knitting Bay 2 | 3,000-hr scheduled sinker ring alignment | Relanit Sinker Ring Set (MC-SP-REL-SINK-48) |
48 Sets | 28 Aug 2026 | MAINTENANCE COMPLETE |
EV-2026-0352 |
GB-2025-04419-US | EchoTex Cutting Room 1 | Carbide blade wear threshold reached | Reciprocating Carbide Blade (GB-SP-PAR-BLD-72) |
2 Blades | 15 Aug 2026 | REPLACED & ZERO-CAL |
EV-2026-0310 |
YM-2024-55021-JP | Beximco Line 4 Station 2 | Lower looper micro-burr causing friction | Differential Looper (YM-SP-VG-LOOP-04) |
1 Set | 02 Aug 2026 | CALIBRATED TO SPEC |
AI Spare-Parts Complaint Reminder & Automatic Escalation System
Autonomous monitoring engine tracking supplier fulfillment SLAs. Dispatches Stage-1 and Stage-2 automated reminders upon SLA breach, escalating unresolved parts shortages directly to global OEM Principal Headquarters under strict idempotency limits.
| Complaint ID | Machine & Serial | Factory / Line | Required Spare Part | Qty (Req / Del / Out) | SLA Deadline | Responsible Supplier | Escalation Stage | AI State | Actions |
|---|---|---|---|---|---|---|---|---|---|
CMP-2026-0819 |
Juki DDL-9000CJK-2024-88492-BD |
Horizon Knitwear Line 12 Station 08 |
Titanium Full-Rotary HookJK-SP-HOOK-ROT-9 |
2 / 0 / 2 Out | 31 Aug 2026 144h Overdue |
Juki Bangladesh Ltd. T. Mahmud (Cert #JK-881) |
STAGE 3: ESCALATED | โ PRINCIPAL NOTIFIED |
|
CMP-2026-0842 |
Mayer Relanit 3.2 IIMC-2023-11094-DE |
Horizon Knitwear Knitting Bay 02 |
Relanit Sinker Ring SetMC-SP-REL-SINK-48 |
4 / 0 / 4 Out | 05 Sep 2026 72h Overdue |
Mayer Regional Service K. Al-Hassan (Dhaka) |
STAGE 2: REMINDER | โ 2ND NOTICE SENT |
|
CMP-2026-0870 |
Gerber Paragon VXGB-2025-04419-US |
EchoTex Green Plant Cutting Room 01 |
Reciprocating Carbide BladeGB-SP-PAR-BLD-72 |
10 / 4 / 6 Out | 08 Sep 2026 24h Overdue |
Gerber Tech Technocenter S. Chowdhury |
STAGE 1: REMINDER | โ 1ST NOTICE SENT |
|
CMP-2026-0795 |
Yamato VG2700YM-2024-55021-JP |
Beximco Industrial Line 04 Station 02 |
Differential Feed LooperYM-SP-VG-LOOP-04 |
2 / 2 / 0 Out | 25 Aug 2026 Fulfilled on Time |
Yamato BD Service Center A. Siddique |
RESOLVED & CLOSED | โ AUTOMATION HALTED |
|
Case CMP-2026-0819 โ Juki DDL-9000C
Logged
Supplier Sent
Supplier Notice
Principal HQ
Pending
| Machine Serial | JK-2024-88492-BD (Horizon Knitwear Line 12) |
|---|---|
| Part Description | Titanium Full-Rotary Hook (JK-SP-HOOK-ROT-9) |
| Quantity Breakdown | Required: 2 | Delivered: 0 | Outstanding: 2 Units |
| Responsible Supplier | Juki Bangladesh Ltd. (Authorized Service Partner) |
| Principal OEM Contact | Juki Corporation Global Operations (Tokyo, Japan) |
| Current Escalation Rule | Exact 3-Stage Maximum: Case locked to ESCALATED; automated loops halted. |
TO: Kenji Takahashi <k.takahashi@juki.co.jp> (Juki Global HQ)
CC: Tariq Mahmud <service.bd@juki.com> (Local Supplier); Horizon Knitwear Admin
SUBJECT: [NOTICE STAGE 3 โ ESCALATION]: Unfulfilled Spare-Part Requirement โ Machine Serial JK-2024-88492-BD
In accordance with the Leadirftex Machine Company Bonding Authorization (#BD-OEM-2026-081), this communication is an automated Stage-3 Escalation regarding unfulfilled spare-part requirement CMP-2026-0819.
โข Machine Model: Juki DDL-9000C-SMS
โข Machine Serial: JK-2024-88492-BD
โข Installed Facility: Horizon Knitwear Ltd. (Line 12)
โข Required Spare Part: Titanium Full-Rotary Hook (JK-SP-HOOK-ROT-9)
โข Outstanding Quantity: 2 Units (0 Delivered)
โข Recorded SLA Deadline: 31 Aug 2026 (144 Operating Hours Overdue)
โข Prior Notice Log: Reminder 1 dispatched 02 Sep 2026; Reminder 2 dispatched 04 Sep 2026.
As the authorized local supplier has not fulfilled this critical component, this matter is formally submitted to Principal Headquarters for immediate inventory intervention from regional emergency depots.
Sincerely,
Leadirftex Interchain Automated Service Continuity Engine
21-Hub Interchain Educational & Machinery Integration
How Hub 03 (Automated Machinery & Equipment Complex) powers technical feasibility and spare-parts reserve, line efficiency, and certified machinery across the Leadirftex manufacturing pipeline.
Digital Production Technology, Smart Automation & OEE Intelligence
Authoritative cyber-physical manufacturing platform uniting smart factory IoT sensor grids, edge AI predictive analytics, autonomous robotics/AMRs, digital twins, and real-time Overall Equipment Effectiveness (OEE) optimization for high-velocity apparel manufacturing.
Latest Technology & Smart Automation Pillars
High-precision engineering technologies deployed across cutting rooms, knitting bays, and smart sewing lines to eliminate bottlenecks and optimize operational equipment effectiveness (OEE).
Robotics & Material Handling
6-axis robotic arms for automated fabric ply picking, automated guided vehicles (AGVs) for roll transfer, and zero-tension automated feeding to prevent knit distortion.
Predictive Maintenance Telemetry
High-frequency vibration sensors and FFT spectrum analysis detect bearing wear, looper misalignment, and thermal spikes 180 operating hours before breakdown.
Loom & Sewing Sensor Grids
Direct-drive IoT adapters capturing stitches per minute (SPM), seam thread tension in cN, needle penetration force, and real-time operator cycle time curves.
Automated Cutting Algorithms
Multi-ply automated vacuum cutting with dynamic knife sharpening, intelligent notch cutting, and automated marker nesting delivering up to 92.4% fabric utilization.
Smart Factory OEE & Production Intelligence Dashboard
Continuous edge telemetry aggregating Availability, Performance, and Quality across 18 connected manufacturing plants, providing instant bottleneck detection, micro-stoppage root causes, and line pacing analytics.
Connected Stitching Line Balancing & Efficiency
| Line ID & Facility | Garment Style | Target (pcs/h) | Actual (pcs/h) | Line Efficiency | Critical Station | WIP Buffer | Line Status |
|---|---|---|---|---|---|---|---|
| Line 01 (Horizon Campus) | Men's Piquรฉ Polo (Navy) | 450 | 462 | 102.6% | Op 12 (Placket Stitch) | 34 pcs (Optimal) | โ OPTIMAL PACING |
| Line 04 (Horizon Campus) | Heavy French Terry Hoodie | 320 | 318 | 99.4% | Op 08 (Rib Cuff Join) | 42 pcs (Optimal) | โ BALANCED |
| Line 07 (EchoTex Plant 2) | Active Performance Tee | 550 | 512 | 93.1% | Op 04 (Flatlock Armhole) | 68 pcs (High WIP) | โ WIP ADJUSTING |
| Line 09 (Beximco Unit 3) | Taped Seam Shell Jacket | 210 | 214 | 101.9% | Op 15 (Ultrasonic Sealing) | 18 pcs (Optimal) | โ OPTIMAL PACING |
| Line 12 (Horizon Campus) | Seamless Engineered Top | 380 | 376 | 98.9% | Op 06 (Neck Binding) | 28 pcs (Optimal) | โ BALANCED |
Automated Micro-Stoppage Ledger
Direct-drive motor feedback logs interruptions <60 seconds (thread breaks, bobbin swaps, needle re-threading) to identify recurring friction before major stoppages occur.
Digital Twin Shopfloor Mesh Topology
High-density industrial MQTT broker bridging 1,840 machine heads into an immutable digital twin representation with zero packet drop and sub-14ms propagation.
Robotics & AI Edge Predictive Intelligence
Real-time edge computing nodes running continuous telemetry algorithms to anticipate mechanical friction and auto-dispatch maintenance requests.
Edge IoT accelerometers mounted on needle bar bearings monitor micro-vibrations across 10 kHz bandwidth. Early harmonic distortion flags lubrication depletion before micro-galling occurs.
Autonomous Mobile Robots (AMRs) transport cut bundles from Gerber Paragon cutters directly to sewing line feeder buffers via SLAM lidar mapping, maintaining 100% bundle integrity.
AI Production Planning, SAM Balancing & Bottleneck Resolution
Algorithmic line balancing assigning operator skill profiles to Standard Allowed Minute (SAM) sewing operations, smoothing Work-in-Progress (WIP) flow and reducing changeover downtime.
Operation Sequence, Pitch Time & Skill Assignment
| Seq # | Operation Name | Machine Asset Class | Standard SAM | Target (pcs/h) | Assigned Operator | Skill Grade | Station Balance |
|---|---|---|---|---|---|---|---|
OP-01 |
Fuse Collar Band Interlining | Rotary Continuous Fusing | 0.48 min | 125 pcs | Fatema Khatun (ID-4402) | GRADE A+ | 98.2% Paced |
OP-02 |
Make & Turn Collar | Lockstitch with Edge Cutter | 0.52 min | 115 pcs | Nazmul Huda (ID-2189) | GRADE A | 96.8% Paced |
OP-03 |
Placket Box & Slit Cutting | Computerized Automatic Placket | 0.50 min | 120 pcs | Shahana Begum (ID-3310) | GRADE A+ | 99.1% Paced |
OP-04 |
Attach Collar to Body Neck | Direct-Drive Lockstitch DDL-9000C | 0.54 min | 111 pcs | Mizanur Rahman (ID-1904) | GRADE A | 100.0% Perfect Pitch |
OP-05 |
Shoulder Seam Join & Reinforce | 4-Thread Overlock High-Speed | 0.46 min | 130 pcs | Rina Akter (ID-5512) | GRADE B+ | 97.4% Paced |
OP-06 |
Sleeve Insertion & Side Seam | Direct-Drive Differential Overlock | 0.53 min | 113 pcs | Abul Kashem (ID-1108) | GRADE A | 98.6% Paced |
Production Technology & Specialized Garment Lab
Specialized technical production machinery engineered for high-performance athletic apparel, waterproof taped outerwear, and seamless tubular knits.
Santoni Top2 Fast Tubular Knitting
Body-size seamless technology with 8 feeds, individual needle selection, and integrated variable compression zones for activewear baselayers.
PFAFF 8312 Ultrasonic Seam Welding
Continuous rotary ultrasonic welding of technical laminates, creating zero-bulk, waterproof and air-impermeable seam joints without needle punctures.
Tonello Laserblaze & ECOBIP Ozone
High-speed digital laser marking and atmospheric ozone garment processing, replacing hazardous chemical bleaching and cutting water usage by 85%.
21-Hub Interchain Educational & Production Technology Integration
How Digital Production Technology & Automation powers real-time line telemetry, AI planning, and smart factory execution across the Leadirftex manufacturing pipeline.
Digital Production Technology & Automation Command Center
Centralized production intelligence platform uniting real-time shopfloor pacing, Overall Equipment Effectiveness (OEE), Non-Productive Time (NPT) loss management, AI line balancing, and dual executive/operational live monitor displays.
Production Command Overview
High-level operational overview synthesizing shift production targets, actual output, OEE scores, running lines, and top-priority losses across all 12 smart manufacturing bays.
Live Production Monitoring
Synchronized line-by-line hourly production telemetry across all 12 smart stitching lines, tracking target pacing, active variance, and progress toward shift quotas.
| Line ID | Product Style | Hourly Target | Current Hour | Shift Target | Shift Actual | Progress | Status | Efficiency |
|---|
OEE & Efficiency Intelligence
Comprehensive Overall Equipment Effectiveness (OEE) metrics decomposed into Availability, Performance Run Rate, and Quality Yield with line-by-line efficiency benchmarking.
Total unplanned downtime: 18 mins across 12 lines
Speed losses caused by fabric tension auto-trims
Defect rate: 0.13% (227 total rejected/reworked units)
NPT & Production Loss Management
Structured incident management for Non-Productive Time (NPT) categorized by root cause, affected workstation, lost minutes accumulator, and resolution lifecycle.
| Incident ID | Line & Workstation | Category | Root Cause Reason | Lost Mins | Severity | Status | Assigned Tech / Action |
|---|
Production Planning & Line Balancing
Industrial engineering mathematical line balancing, Standard Allowed Minutes (SAM) formula calculation, pitch-time allocation, and bottleneck mitigation matrix.
= [18.42 min รท (34 ร 0.54 min)] ร 100% = 94.2% Achieved
| Op Seq | Operation Name | Machine Asset Class | SAM | Target Pcs/Hr | Assigned Operator | Skill Grade | Pacing |
|---|---|---|---|---|---|---|---|
OP-01 |
Placket Creasing & Fusing | Hashima HP-450MS Press | 2.45 min | 185 | Farzana Yasmin (ID: 4091) | Grade A+ | 102% |
OP-02 |
Collar Band Stitching | Juki DDL-9000C Lockstitch | 3.10 min | 180 | Mohammad Al-Amin (ID: 4108) | Grade A | 100% |
OP-03 |
Collar Joining & Edge Topstitch | Brother S-7300A Direct-Drive | 3.80 min | 175 | Nasrin Sultana (ID: 4122) | Grade B+ | 94% (Bottleneck) |
OP-04 |
Shoulder Seam Overlock Joint | Pegasus M900 4-Thread Overlock | 1.85 min | 210 | Shahidul Islam (ID: 4145) | Grade A | 104% |
OP-05 |
Sleeve Hemming & Flatlock Stitch | Yamato VG2700 Cylinder Flatlock | 2.60 min | 190 | Roksana Begum (ID: 4158) | Grade A+ | 101% |
OP-06 |
Bottom Hem Twin Needle Stitch | Juki MF-7900 Coverstitch | 2.20 min | 195 | Abdul Mannan (ID: 4172) | Grade A | 100% |
Quality & Production Yield
Continuous inline quality assurance tracking Defects per Hundred Units (DHU), First Pass Yield (FPY), defect classification Pareto, and speed-to-quality correlation curves.
AI correlation engine monitors stitches per minute (SPM) against inline optical defect flags to prevent speed-induced stitch skipping.
Maintenance & Production Interruption
Production downtime analytics, breakdown diagnostics, Mean Time To Repair (MTTR), Mean Time Between Failures (MTBF), and scheduled preventative maintenance logs.
| Machine Asset | Line Location | Fault Classification | Downtime Logged | Assigned Tech | Resolution Status | Production Impact |
|---|---|---|---|---|---|---|
| Juki MO-6814S Overlock | Line 08 ยท Stn 14 | Looper thread guide snag & motor trip | 28 mins | K. M. Hossain | On-Site Diagnosis | Pacing throttled to 78% |
| Gerber Paragon Cutter | Cutting Bay 02 | Vacuum table micro-seal pressure drop | 12 mins | M. R. Talukder | Seal Replaced | Buffer absorbed delay |
Workforce & Factory Operations
Real-time floor attendance tracking, skill-specific operator shortage analysis, floater reallocation deployment, and workforce capacity impact on planned volume.
AI, Automation & Smart Factory Intelligence
High-frequency sensor telemetry, edge AI spectral vibration analysis, autonomous material transport robots (AMRs), and industrial digital twin shopfloor topologies.
AI Spectral Vibration FFT Analysis
10 kHz high-bandwidth piezoelectric accelerometers mounted on sewing drive shafts detect micro-wear 180 hours prior to mechanical failure.
SLAM Lidar AMR Fleet Synchronization
Fleet of 24 autonomous mobile robots transporting cut fabric plies from Gerber automated cutting bays directly to stitching line buffer stations.
Industrial MQTT Broker Telemetry
High-density industrial broker bridging 1,840 machine heads into an immutable digital twin representation with zero packet drop and sub-14ms propagation.
Reports & Analytics
Centralized industrial production report repository covering target achievement, OEE trends, NPT loss distribution, quality DHU records, and TPM maintenance logs.
Shift Production Performance & Quota Variance Audit
Aggregated shift metrics across 12 lines for Day Shift (06:00 - 14:00 BST).
Purchase-price optimization without technical and production-impact visibility can create higher total operating cost. A component with a lower purchase price may exhibit shorter durability, higher failure frequency, increased maintenance labor, and extended line downtimeโgenerating production losses that far exceed initial savings.
3 micro-friction sensor spikes logged in the last 30 days. Historical inspection reveals tolerance variance from using sub-grade bobbin cases (ยฑ0.035mm vs OEM ยฑ0.005mm), leading to thread tension instability.
Titanium Full-Rotary Hook Assembly
JK-SP-HOOK-ROT-9Zero micro-burrs; precision heat treatment maintains needle clearance and tension equilibrium at 5,000+ SPM without skipped stitches or heat galling.
Click any component to inspect grade specifications & durability:
Authoritative Machine Parts Table (Excel-Style Technical View)
All discoverable spare parts mapped to Juki DDL-9000C-SMS. Filter by code, name, or functional group:
| # | Photo | Part Code | Part Name & Category | Technical Specification & Material | Source & Availability | Public Price | Actions |
|---|
Fabric Marketplace โ PHYSICAL MILL VERIFICATION AUTHORIZED
โFind the Fabric Before You Find the Problem.โ
Direct industrial B2B material discovery, running shade lot inspection, shrinkage verification, and laboratory certified swatch sampling across vetted textile mills.
Technical Specification Sheet โ PHYSICALLY VERIFIED
SKU: LTX-FAB-380-FT | Apex Textile Mills Ltd. | Laboratory Certificate: ITS-2026-BD-8842
Order Physical Swatch & Lab Kit
Direct dispatch from accredited mill testing laboratory
Side-by-Side Fabric Specification Matrix
Direct technical evaluation across compositions, GSM, running shade stability, and shrinkage
๐ญ Register Fabric Lot for Verification (Mill Listing)
Accredited textile mills submit production lots with spectrophotometer ฮE & lab reports
๐ฌ Optional Optical Spectrophotometer & Scanner Tool
Supplementary physical hardware tool โ Standard sourcing proceeds directly without scanning
Connect via USB-C / Bluetooth spectrophotometer or optical sensor for real-time EPI/PPI thread density and CIELAB color coordinate extraction.
Laboratory Technical Audit Dossier
| Fabric Type / Construction | 3-End French Terry Circular Knit (24 Gauge) |
| Weight / Tolerance | 380 GSM ยฑ 3% (ISO 3801 Standard) |
| Fiber Composition | 100% Combed Ring-Spun Organic Cotton (GOTS Scope Certificate #92817) |
| Dyeing & Chemistry | Low-impact reactive dyeing, ZDHC Level 3 certified, OEKO-TEX Standard 100 Class I |
| Tensile / Bursting Strength | Bursting Strength > 420 kPa (ASTM D3786) |
| Pilling Resistance | Grade 4.0 after 2,000 cycles (Martindale Method ISO 12945-2) |
| Packaging & Roll Length | 50-meter rolls on 3-inch cardboard core, wrapped in 2-ply biodegradable polybag |
"Ordered the physical swatch kit first via DHL, arrived in 3 days. Loop consistency and brushing softness are exceptional. We then placed an escrow order for 12,000 kg. Shinkage tested at exactly 2.4% well within spec. Zero lot-to-lot color drift across 6 dye vats."
"Heavy handfeel with superior diagonal loop alignment. Perfect for our heavyweight Autumn 2026 luxury streetwear hoodie line. Swatch arrived hermetically sealed with original mill QA tags."
Frequently Sampled Together
Matching rib knits, poplins, and organic linings certified for export
Wash, Dry Processing & Chemical โ ENVIRONMENTAL ETP AUDIT AUTHORIZED
Engineered Surface, Color & Texture Intelligence.
End-to-end industrial B2B ecosystem connecting garment washing, laser dry processing, continuous dyeing, rotary printing, functional finishing, and certified ZDHC Level 3 textile chemicals with verified service providers.
Process Engineering Specification Sheet โ ZDHC LEVEL 3 AUDITED
Service Code: PRC-WASH-ENZ-01 | Apex Sustainable Washing Ltd. | Dhaka Export Zone
๐ Submit Processing Order / RFQ
Direct requirement routing to accredited washing, dyeing & finishing facilities
Side-by-Side Processing Facility Comparison
Direct evaluation across machinery fleet, daily output, chemical compliance, and lead times
๐ฌ Optional Process & Chemical QR Scanner Tool
Supplementary hardware verification tool โ Standard processing discovery proceeds without scanning
Direct integration with warehouse barcode readers or camera input for batch traceability and recipe verification.
Retail Marketplace โ VERIFIED MULTIVENDOR COMMERCE
Scalable Multi-Category Retail Network.
Direct consumer and wholesale purchasing across brand flagships, authorized retailers, and independent verified sellers. Multi-seller offers per product, real-time inventory, and seller-grouped fulfillment.
Heavyweight 380 GSM Organic Loopback Hoodie โ 3 SELLER OFFERS
SKU: LTX-RET-001 | Apex Brand Direct โข Nordic Apparel โข Urban Stockist
Apex Brand Flagship Store
Official Verified Brand โข Dhaka Export Zone โข 99.4% On-Time Fulfillment
โ๏ธ Leadirftex Seller Center Console
Multivendor Catalog, Real-Time SKU Inventory & Order Fulfillment Pipeline
| SKU Code | Product Title | Variant (Size / Color) | Available Stock | Reserved | Offer Price | Fulfillment Status |
|---|
๐ Multivendor Shopping Cart
Orders grouped by verified seller with independent fulfillment & tracking
๐ Multivendor Checkout Protocol
Consolidated Escrow Payment โข Independent Seller Dispatch
Side-by-Side Product Comparison Matrix
Direct technical evaluation across materials, GSM, size availability, and seller offers
Horizon Knitwear Ltd.
๐ 11 Discrete Performance Dimensions (Uncollapsed & Explainable)
๐ฆ Verified Transaction & Shipment History (CargoView IA)
| PO# & Contract ID | Counterparty | Product / Style | Quantity | Promised Delivery | Actual FOB Date | Quality / AQL | Shipment Status | Claim Status | Score Impact |
|---|
Official Business Email Claim & Dispute Adjudication Workflow
Anti-Retaliation Architecture: Submitting a claim does not automatically deduct factory score points. Every claim must pass registered corporate email validation, transaction matching, factory counter-evidence review, and Leadirftex QA adjudication. Disputed claims remain marked CLAIM DISPUTED with score impact pending.
โฑ๏ธ Verified Milestone Timeline
๐ Score Change Audit Log (Server-Authoritative)
| Event ID | Type | Dim | Old → New | Adjudicator | Time |
|---|
Horizon Knitwear Ltd. Compliance & ESG Intelligence
Integrated multi-body audit intelligence across labor standards, fair living wages, fire & structural safety, chemical management, and environmental certifications. 100% verified third-party audit reports with cryptographic registrar seals.
๐๏ธ Interactive Organization Compliance Cards (Touch to Slide Out)
Partner With Leadirftex Interchain Compliance Network
Connect your standard, audit protocols, or ESG certification directly into Leadirftex. Enable automated factory record verification, issue cryptographic audit seals, and provide international fashion brands with authoritative ground-truth compliance intelligence.
Horizon Knitwear & Apparels Ltd.
Premier export-oriented vertical apparel manufacturing facility specializing in sustainable circular knitwear, heavy fleece outerwear, and organic combed jersey. Delivering verified production integrity to top global retail brands across the European Union, North America, and United Kingdom.
Product Capability & Garment Construction
Dedicated production teams trained in high-density knitwear, precision flatlock activewear, and heavy brushed fleece.
Heavyweight Fleece & Hoodies
360โ480 GSM 3-end fleece, custom diagonal loopback terry, double-layered articulated hoods with bar-tack pocket reinforcements.
Engineered Luxury T-Shirts
180โ260 GSM single jersey & interlock in combed organic ring-spun cotton. Enzymatic bio-polish with pre-shrunk anti-torque finish.
Technical Joggers & Sweatpants
320โ420 GSM brushed sweatpants with ergonomic knee articulation, zippered waterproof pocket inserts, and ribbed bungee cuffs.
Seamless & Activewear Layers
Recycled micro-polyester and elastane blend compression tops with Yamato 4-needle flatlock seams and moisture-wicking channels.
Verified Production Capacity Allocation
Current manufacturing pipeline for Q3 / Q4. Real-time factory floor allocation verified through daily production logs and telemetry.
Commercial Ordering Parameters
Machinery Inventory & Automated Production Floor
Audited machinery inventory operating with computerized maintenance management systems and IoT telemetry.
Audited Certifications & Global Accreditations
All certifications are authenticated through third-party audits with issuing bodies.
WRAP Gold Certificate
Worldwide Responsible Accredited Production
BSCI Social Audit
Business Social Compliance Initiative
OEKO-TEX Standard 100
Product Class 1 (Safe for Infants)
GOTS Organic Cotton
Global Organic Textile Standard
HIGG Index FEM / FSLM
Facility Environmental & Labor Module
Factory Safety & Social Compliance
Rigorous adherence to international occupational health, fire prevention, and fair labor conventions.
Environmental & Sustainability Telemetry
Quantified environmental investments reducing carbon emissions and industrial water intensity.
Verified Factory Information
"Verified factory performance history, quality records, transaction evidence & trust controls."
Factory Evidence & Compliance Audit Records
| Document Record Name | Issuing Authority | Audit Period | Verification State | Action |
|---|---|---|---|---|
| SGS Comprehensive Facility Audit Report (68 Pages) | SGS Bangladesh Ltd. | Jan 2026 โ Jan 2027 | โ Verified Pass | |
| Accord / RSC Structural & Fire Remediation Cert | RMG Sustainability Council | Current โข Valid | โ Verified Pass | |
| Department of Environment (DoE) ETP Discharge Analysis | Ministry of Environment | Q1 2026 Batch Test | โ Verified Pass | |
| ISO 9001:2015 Quality Management Scope Certificate | Bureau Veritas | 2024 โ 2027 | โ Verified Pass |
Contextual Factory Interchain Connectivity
Connect Horizon Knitwear directly to material sourcing, prototype sample development, buyer RFQ tenders, and order execution.
Structured Buyer Procurement Specification
Eliminate vague inquiries. Input comprehensive parameters to receive guaranteed, comparable factory bids.
Supports Adobe Illustrator (.AI), Gerber Pattern (.DXF), Tech-Pack (.PDF), Spec Sheet (.XLSX) up to 100MB
AI Factory & Supplier Matching Engine โก 3 Qualified Matches Found
Matched against 420 audited mills using machine RPM compatibility, certified capacity, and FOB price fit.
Horizon Knitwear & Apparels Ltd.
โ On-Site Audited- 100% capacity fit on Mayer & Cie 24-gauge circular knitting
- FOB Target fit: Historical average $5.90 - $6.15 for 380 GSM fleece
- WRAP Gold and GOTS certification active through 2026
Apex Textile Mills Ltd.
โ On-Site Audited- In-house spinning and knitting lines for vertical lead-time reduction
- OEKO-TEX 100 Class 1 verified lab swatch #8812 available
- Dispute rate: 0.0% across 48 verified Leadirftex purchase orders
Surat Spun & Apparels Tech
โ On-Site Audited- Specialized heavy cotton enzyme washing and laser distressing
- Target FOB estimate: $6.05 / pc
Quotation Analysis & Cost Breakdown 3 Binding Quotations Received
Side-by-side transparent breakdown across Fabric, Cut & Make, Trims, and FOB freight.
| Bidding Factory | Fabric Cost (FOB) | Cut & Make (CM) | Trims & Accessories | Washing & Finish | Total FOB Price | Sample SLA | Action |
|---|---|---|---|---|---|---|---|
|
Horizon Knitwear Ltd.
โ
RECOMMENDED (97% Match)
|
$3.10 / pc | $1.65 / pc | $0.65 / pc | $0.45 / pc | $5.85 / pc | 7 Days | |
|
Apex Textile Mills
Tier 1 Verified Mill
|
$3.25 / pc | $1.80 / pc | $0.60 / pc | $0.45 / pc | $6.10 / pc | 10 Days | |
|
Surat Spun Tech
Tier 1 Verified Mill
|
$3.40 / pc | $1.75 / pc | $0.70 / pc | $0.50 / pc | $6.35 / pc | 12 Days |
Pre-Production (PP) Gold Seal Sample Review
Measurement Tolerance Verification Table (Size L)
| Measurement Point | Spec Sheet (cm) | Sample Actual (cm) | Tolerance (ยฑ cm) | Variance (cm) | Status |
|---|---|---|---|---|---|
| Chest Width (1" below armhole) | 62.0 | 62.2 | ยฑ 1.0 | +0.2 | PASS |
| Body Length (from HPS) | 74.0 | 74.1 | ยฑ 1.0 | +0.1 | PASS |
| Sleeve Length (from shoulder) | 66.5 | 66.3 | ยฑ 0.5 | -0.2 | PASS |
| Hood Height | 38.0 | 38.0 | ยฑ 0.5 | 0.0 | PASS |
Heavyweight French Terry Pullover Hoodie
End-to-end merchandising pipeline connecting buyer specifications, tech-pack tolerances, material BOM, garment costing, and factory production readiness.
๐ Garment CAD Spec & Visual
3D WIREFRAMESize Grading & Inspection Variance (Size L Baseline)
Standard: ISO 2859-1 Physical On-Site Tolerance Calibration| Measurement Point | Spec (cm) | Sample Actual | Tolerance | Variance | Verdict |
|---|---|---|---|---|---|
| Chest Width (1" below armhole) | 62.0 | 62.2 | ± 1.0 cm | +0.2 cm | PASS |
| Body Length (from HPS) | 74.0 | 74.1 | ± 1.0 cm | +0.1 cm | PASS |
| Sleeve Length (from shoulder seam) | 66.5 | 66.3 | ± 0.5 cm | -0.2 cm | PASS |
| Hood Height (along crown curve) | 38.0 | 38.0 | ± 0.5 cm | 0.0 cm | PASS |
| Across Shoulder (seam to seam) | 56.0 | 56.3 | ± 0.8 cm | +0.3 cm | PASS |
| Bottom Rib Hem Height | 7.0 | 7.0 | ± 0.3 cm | 0.0 cm | PASS |
Comprehensive Bill of Materials (BOM)
Certified components, yarn origins & environmental compliance| Component | Specification & Composition | Supplier / Mill | Audit Status |
|---|---|---|---|
| Primary Shell | 380 GSM 100% Combed Ring-Spun Cotton French Terry | Horizon Knitwear (Dhaka) | PHYSICAL PASS |
| 2x2 Heavy Rib | 450 GSM 95% Cotton / 5% Spandex (Cuff & Waistband) | Horizon Knitwear (Dhaka) | D65 MATCHED |
| Pocket Lining | 160 GSM 100% Cotton Single Jersey Pocketing | Shandong Textile Group | BATCH VALID |
| Braided Drawcord | 100% Cotton Round Tubular with Matte Gunmetal Aglets | YKK Trim Division | PULL TEST 150N |
| Thread Package | Gรผtermann Tera 40/80 Core-Spun Polyester | Gรผtermann SE (Germany) | COLOR CERTIFIED |
| Branding Labels | High-Density Damask Woven Main Label + Interchain QR Seal | Avery Dennison RBIS | QR VERIFIED |
Apparel Cut-Make-Trim (CMT) & Consumption Costing
Transparent factory floor manufacturing yield and FOB quotation breakdown| Cost Center Item | Basis / Yield Parameter | Unit Cost (USD) | Total (15,000 Pcs) |
|---|---|---|---|
| Shell Fabric (380 GSM) | 0.85 KG consumption including 5% cutting wastage @ $6.20/kg | $5.27 | $79,050.00 |
| Rib & Pocket Lining Package | 0.15 KG 2x2 Rib + 0.05 KG Jersey lining | $0.95 | $14,250.00 |
| Trims, Labels & Aglets | Drawcords, woven labels, polybags, export cartons (24 pcs/ctn) | $0.95 | $14,250.00 |
| Cut, Make & Trim (CMT) Labor | Dedicated Line 12 & 14 Juki direct drive automated stitching | $3.20 | $48,000.00 |
| Bio-Enzyme Wash & Finishing | Tonello eco-wash finishing, pre-shrinkage tumble dry, steam press | $1.10 | $16,500.00 |
| TOTAL TARGET FOB (FOB CHITTAGONG) | 15,000 Units โข 3 Colorways | $11.47 | $172,050.00 |
Sample Approval Loop & Gold Seal Verification
Physical audit trail with tamper-proof laboratory timestampsโก Production Readiness Index
84% READY๐ฌ Tri-Party Merchandising Chat
3 PARTICIPANTSAQL Inspection Defect Log
| Defect Category | Tolerance Allowed | Defects Discovered | Defect Details | Result |
|---|---|---|---|---|
| Critical Defects | 0 Allowed | 0 | No broken needles, sharp points, or safety hazards detected | PASSED |
| Major Defects | Max 14 Allowed (AQL 2.5) | 3 Found | 2x Minor shade variation on pocket, 1x Skip stitch on waistband | PASSED |
| Minor Defects | Max 21 Allowed (AQL 4.0) | 8 Found | Untrimmed threads > 1cm, minor wrinkle press marks | PASSED |
Enterprise Security, Trust & Biometric Identity
Unified physical ground-truth verification, multi-factor biometric authentication, and immutable cryptographic audit ledgers securing global interchain transactions.
Facial Recognition Scan
Biometric Ridge Scan
Enterprise Document Audit
Zero Trust Security Architecture
Never trust, always verify. Every mill transaction, fabric tech-pack inspection, and financial escrow disbursement undergoes continuous mutual hardware authentication.
Protected Data & HSM Vault
Proprietary apparel tech-packs, CAD DXF patterns, and financial payment parameters are protected inside isolated cryptographic enclaves.
Canonical Ground-Truth Verification
To prevent supply chain fraud, Leadirftex strictly demarcates physical audits from algorithmic scores and self-reported declarations.
Physically Verified Data
Audited in person by Leadirftex staff or accredited inspection firms (SGS, TรV, BV). Stored with cryptographic hashes and auditor timestamps.
AI-Assessed Predictions
Algorithmic pattern recognition, NLP tech-pack extraction, and historical delay risk forecasting.
Factory Self-Reported Claims
Self-declared factory capacity, preliminary price quotes, and unverified mill certificates pending third-party review.
Deploy Your Supply Chain on Verified Infrastructure
Eliminate intermediary risk, counterfeit certifications, and settlement disputes with Leadirftex's cryptographically verified sourcing architecture.
Executive Operations & Sourcing Cockpit
Global supply chain intelligence across Bangladesh, India, Vietnam & China production hubs.
โ๏ธ 21-Hub Interchain Pipeline
Live Sequence ActiveActive Manufacturing Contracts
3 POs In Production| PO Hash | Style / Construction | Factory & Mill | Volume | Production Progress | Ex-Factory | Action |
|---|---|---|---|---|---|---|
| #LTX-88219 |
380 GSM Heavy Hoodie
100% French Terry Brushed
|
Horizon Knitwear Ltd. (BD) | 15,000 Pcs |
|
Nov 15, 2026 | |
| #LTX-88194 |
Organic Combed T-Shirts
180 GSM Single Jersey Bio-Washed
|
Apex Textile Mills (BD) | 40,000 Pcs |
|
Dec 02, 2026 | |
| #LTX-87941 |
Selvedge Denim Jeans
13.5 oz Raw Ring-Spun Indigo
|
Nahar Denim Mills (IN) | 8,000 Pcs |
|
Oct 28, 2026 |
Find Your Next Textile Career.
Build a Professional CV for Free.
Functional discovery inspired by NextJobz with multi-facet filters, verified company specifications, and direct external application. Build an ATS-optimized CV across 10 print-safe A4 templates with zero paywall.
Free Professional CV Builder & LX Intelligence OCR
Create, review, and print ATS-optimized CVs formatted specifically for textile mills, buying houses, and garment factories.
Click or drop document to run LX Intelligence (Test Pipeline) extraction & data review.
NextJobz Functional Model + Authorised Ingestion Pipeline
Leadirftex does not perform unauthorized scraping. Job data is ingested strictly via authorized API feeds, normalized to the canonical Leadirftex schema, deduplicated using composite source cryptographic hashes, and published with mandatory company provenance and external redirect anchors.
Zero Server Retention & Candidate Privacy Policy
Leadirftex Interchain is strictly a job discovery and free CV creation tool. We do not operate an employer ATS, we do not store your uploaded CV or generated resume on our servers, and we never sell candidate information to recruitment agencies. When you click [View & Apply], you are redirected to the verified job source to submit your application directly using your own account.
Job Title
Role Overview & Key Responsibilities
Educational & Technical Criteria
Job Title
Company Name
Verify Extracted Information Before Generation
Review and correct any extracted fields below. Items marked with โ ๏ธ Needs Review require candidate confirmation to prevent OCR misinterpretations.
Free Textile CV Builder Workspace
Unified with Page 23 Job Feed • 10 Print-Safe A4 Templates
Complete 21-Hub Platform Registry
Canonical architectural mapping for all 21 Leadirftex Interchain hubs.
Interactive 3D Clo3D models, CAD DXF patterns, and live garment carousel.
Textile engineering, garment technology, IE & line balancing.
Bonded machine manufacturers, serial tracking, warranties & local reserves.
Industry 4.0, real-time OEE, robotics/AMRs, AI line balancing & telemetry.
Ne/Nm counts, combed cotton, synthetic filament.
Knit, woven, denim with verified physical swatches.
Circular knitting, stenters, sewing machinery.
Enzyme washing, ozone distressing, ETP audit.
Zippers, buttons, interlinings, care labels.
ZDHC Level 3 dyes, biodegradable polybags.
DXF patterns, 3D Clo3D models, grading.
Proto review, fit samples, lab-dip spectral tracking.
Structured RFQ wizard, target FOB, MOQ rules.
Algorithmic capacity fit, bid comparisons.
13-stage order pipeline, daily logs, telemetry.
Dyeing units, testing laboratories, trims.
Horizon Knitwear campus, machinery, compliance & verified records.
AQL defect analysis, QA sign-offs, certificates.
Bill of Lading checks, freight forwarders.
Verified cancelled shipments, excess inventory & factory surplus liquidation.
Multivendor finished apparel and future multi-category catalog.
Verified transaction-based trust, 11 score dimensions & claim adjudication.
Figma-grade compliance dashboard, 8 accredited standards & interactive organization cards.
Authorised industry job discovery, external apply, and 10 print-safe A4 CV templates.
Leadirftex Global Fluid Design & Auto-Spacing Architecture
Authoritative mathematical spatial system governing all 16 platform modules: CONTENT โ AUTO SIZE โ FLEX / GRID โ GAP โ CONTAINER โ RESPONSIVE GUTTER โ VIEWPORT
Global Container & Fluid Responsive Gutters
100% fluid ≤ 1440px
Authoritative 4px Rhythm Spacing Scale
--space-3xs (4px)
Micro Badges & Status Dots
--space-2xs (6px)
Header Nav Button Gap
--space-xs (8px)
Input Padding & Icon Gap
--space-sm (12px)
Card Internal Elements
--space-md-sm (14px)
6-Col Gap & Hero Icons
--space-md (16px)
Mobile Gutter & Compact Pad
--space-lg-sm (20px)
Tablet Gutter & 4-Col Gap
--space-lg (24px)
Desktop Gutter & 3-Col Gap
--space-xl (32px)
Large Card & Split Gap
--space-section (64px)
Standard Section Rhythm
--space-section-lg (80px)
Flagship Showcase Rhythm
Fluid Typography Hierarchy (CSS Clamp Scaling)
--font-hero: clamp(34px, 4vw, 48px);
--font-h1: clamp(26px, 3vw, 36px);
--font-h2: clamp(22px, 2.5vw, 30px);
--font-h3: clamp(17px, 2vw, 20px);
--font-body-lg: 16px;
--font-body: 14px;
--font-eyebrow: 11px;
Reusable Global Grid Primitives (Auto-Responsive)
Fabric Marketplace
Certified mill swatch orders and yardage stocklots with escrow safety.
Factory Network
2,400+ verified garment manufacturers with live SMETA compliance audit trails.
AI Neural Matching
Automated tech-pack requirement decomposition with instant line capacity discovery.
Zero-Trust Enclave
Cryptographic milestone release and immutable purchase order execution.
Enterprise Brand Sourcing
Direct cryptographic access to tier-1 mills, automated sample rounds, and bulk production tracking.
Mill & Factory Operating OS
Capacity utilization dispatch, live machine telemetry feeds, and international buyer RFQ bidding.
Quality & Lab Inspection
Digital AQL defect logging, physical fabric roll testing sign-offs, and container pre-shipment seals.
Tactile 3D Button Hierarchy & Specular Bevels
Content-Driven Auto-Layout Test Bench
Comprehensive Multi-Line Architectural Heading Demonstrating Auto Vertical Flow Without Manual Margins
This test card verifies that whether the text block is 1 line or 5 lines, the entire surrounding layout automatically accommodates it using intrinsic sizing and flex/grid gap. No elements overlap, no fixed heights clip content, and zero manual coordinate adjustments are needed.
Production Floor Solution
Unified production-floor command interface consolidating executive oversight, department dashboards, NPT tracking, sewing operations, quality metrics, maintenance status, IE line balancing, attendance, machine monitoring, cutting, store management, and compliance reporting.
Executive Wall Production
NPT Live Report TV
Store & Materials
Machines Status
IE & Line Balancing
Attendance Status
Employees & Skills
Performance Index
Zone 02 • Operational Analytics Overview
Zone 03 • HR Reports & Workforce Structure
Zone 04 • Management Reports & Audit Logs
Zone 06 • LX Intelligence Anomaly Diagnostics
Zone 05 • Operational Trends & Opportunities
Zone 07 • Factory Improvement & Suggestions
๐ Executive Command & Strategy Console
Authoritative executive operational intelligence consolidating factory health, production cadence, line variance, OEE parameters, quality compliance, loss economics, and strategic action directives across Plant TX-CHITTAGONG-01.
01. Executive Overview
Plant TX-CHITTAGONG-01 demonstrates robust performance during Shift 01 with a composite health index of 93.8 / 100. Factory production pace is executing at 94.0% (17,290 / 18,400 Pcs) with active line recovery in effect for Line 08. Floor efficiency tracks closely to plan at 84.6% (target 85.0%), while overall plant quality remains superior at 1.42% DHU with zero critical quality holds. 482 of 500 rostered workers are present on-floor (96.4% presenteeism) and 14 floaters are actively redeployed to sustain takt pacing.
02. Factory Snapshot
03. Production Status
04. Efficiency KPI
05. OEE Summary
06. Quality Status
07. NPT & Loss
08. Line Performance
| Line ID | Running Style | Target Pcs | Actual Pcs | Pacing % | Efficiency % | Operational Status |
|---|---|---|---|---|---|---|
| Line 01 | LTX-POLO-88 | 1,500 | 1,532 | 102.1% | 88.2% | NORMAL |
| Line 04 | LTX-ACTIVE-42 | 1,600 | 1,702 | 106.4% | 91.2% | TOP PACE |
| Line 08 | LTX-POLO-88C | 1,440 | 1,128 | 78.4% | 74.8% | BOTTLENECK |
| Line 11 | LTX-BASIC-02 | 1,550 | 1,336 | 86.2% | 81.4% | RESTRICTED |
09. Workforce Status
10. Machine Status
11. Capacity & Flow
12. Shipment Status
13. Compliance Status
14. Critical Alerts
15. Management Decisions
Reallocate 2 Grade A floaters from Line 04 (operating at 106.4% pacing) to Line 08 Station 14 & 16 to accelerate post-repair assembly.
APPROVED • IN EXECUTIONAuthorize internal express transfer of French Terry lot #FL-9023 from Apex Dyehouse to maintain the 48-hour cutting buffer intact.
APPROVED • DISPATCHEDPre-approve 30 minutes of selective post-shift overtime for Line 08 if shift actual deficit exceeds 250 garments by 16:30 BST.
AUTHORIZED CONDITIONAL16. Action Status
| Action Item Description | Designated Owner | Priority | Workflow Status | Target Completion |
|---|---|---|---|---|
| Mount spare Pegasus looper #JK-SP-LP-900 on Line 08 | K. M. Hossain (Lead Mechanic) | P1 - HIGH | 85% Complete (Testing) | 15:45 BST |
| Central Store runner delivery of thread #T-882 to Line 11 | Central Store Dispatch | P2 - MED | In Transit (ETA 15m) | 15:50 BST |
| Pre-stage 14 needle sets for Style #P-88 QCO changeover | Engr. Tariq Mahmud (IE Lead) | P3 - NORM | 100% Complete | 16:00 BST |
| Verify export carton barcoding for Nordic PO-88920 | Finishing Supervisor | P4 - AUDIT | Verified & Staged | 16:30 BST |
17. Executive Summary
Operational stability across Plant TX-CHITTAGONG-01 is established at 93.8 / 100 composite health. Factory execution pacing of 94.0% (17,290 Pcs) satisfies shipment security for lead export order PO-88920. Mechanical containment on Line 08 is entering final verification with zero risk of order default. Factory floor efficiency is holding at 84.6%, OEE stands at 87.4%, and quality standards exceed buyer specification at 1.42% DHU. Executive authorization for floater redeployment and overtime buffering protects full shift commitment.
๐ Floor Operations Dashboard Console
Consolidated real-time operational dashboard synthesizing production volume, quality throughput, manpower staffing, equipment telemetry, NPT loss analysis, and target achievement across all 12 operational sewing lines at Plant TX-CHITTAGONG-01.
01. Dashboard Overview
Overall factory pulse, active lines, operational status score, and shift pacing telemetry across Plant TX-CHITTAGONG-01.
02. Factory Snapshot
Core plant footprint, active line count, running garment styles, and shift operating mode.
03. Production Summary
Shift target vs actual volume, run rate per hour, day cumulative output, and overall volume pacing.
| Department / Zone | Target Output | Actual Output | Variance | Achievement % | Pacing Trend | Status |
|---|---|---|---|---|---|---|
| Sewing Floor (Lines 01-12) | 10,080 Pcs | 9,842 Pcs | -238 Pcs | 97.6% | ON TRACK | |
| Cutting Bay 01 & 02 | 11,500 Pcs | 11,280 Pcs | -220 Pcs | 98.1% | SYNCHRONIZED | |
| Finishing & Pressing | 9,800 Pcs | 9,510 Pcs | -290 Pcs | 97.0% | ON TRACK | |
| Packing & Cartoning | 9,200 Pcs | 8,940 Pcs | -260 Pcs | 97.2% | DISPATCH READY |
04. Quality Summary
End-line inspection volume, pass rate percentage, rework count, defect count, and primary defect pareto.
05. Manpower Summary
Total on-duty headcount, line operators, helpers, quality checkers, mechanics, and presenteeism rate.
06. Machine Status
Machine fleet inventory, active sewing heads, idle reserve units, and breakdown status.
07. NPT Summary
Non-Productive Time accumulation across sewing, cutting, maintenance, and material supply chains.
| Loss Category | Total Downtime | Average Per Line | Garment Output Impact | Root Cause Pareto | Mitigation Status |
|---|---|---|---|---|---|
| Mechanical Breakdown | 63 Mins | 5.25 Mins | -184 Pcs | Pegasus Looper Friction & Trimmer Jam | TECH DISPATCHED |
| Material & Trim Wait | 48 Mins | 4.00 Mins | -140 Pcs | Navy Spun Poly Thread Staging Delay | RESOLVED (<10m) |
| Line Balancing Loss | 42 Mins | 3.50 Mins | -122 Pcs | Station 04 Collar Attach Pitch Variance | HELPER ASSIGNED |
| Quick Changeover (SMED) | 32 Mins | 2.67 Mins | -94 Pcs | Staggered Batch Needle Gauge Swap | WITHIN SMED TARGET |
08. Line Status
Line-by-line operational health matrix across all 12 operational sewing lines.
09. Efficiency Overview
Factory labor efficiency index, standard SAM vs actual time, and line-level efficiency distribution.
10. OEE Snapshot
Overall Equipment Effectiveness composite score: Availability, Performance, and Quality yield rates.
11. Output Status
Hourly production cadence against target curve with cumulative variance tracking.
12. Target Achievement
Shift target achievement rate per line with on-time delivery projection and fulfillment status.
13. Capacity Status
Installed vs utilized sewing capacity, bottleneck work centers, and load balancing factors.
14. Material Status
Fabric cut pieces availability, trim and thread readiness, WIP buffer health, and stockout alerts.
15. Maintenance Status
Active corrective maintenance tickets, planned PM compliance, fleet MTTR, and MTBF.
16. Attendance Status
Departmental attendance ratios, planned vs actual operator staffing, and critical skill coverage.
17. Shipment Status
Buyer order commitments, packed carton audit, audit clearance status, and shipping schedule.
18. Critical Alerts
P1 & P2 priority alerts requiring immediate production management and supervisory intervention.
Looper micro-friction detected at 14:12 BST. Mechanic K. M. Hossain deployed. Looper set replaced, 18 test seams verified. Line restart in progress.
Line 03 thread buffer down to 35 cones. Store feeder issued fresh lot #TH-889B from central supply. Transit delivery estimated <10 minutes.
19. Operational Alerts
Floor coordination notices, upcoming style transition alerts, and component replenishment updates.
Next running style LTX-POLO-88C pre-setting 91.7% completed. 14 needle gauges and 120 pre-wound bobbins staged at workshop bay.
Pneumatic central feed operating stably at 6.2 bar. Vacuum tables on cutting bay reporting 100% suction integrity.
20. Performance Trends
Hourly and weekly production velocity, efficiency trends, and quality progression metrics.
21. Daily Summary
Consolidated daily production figures, aggregate SAM earned, lost minutes, and net efficiency.
| Metric Indicator | Shift Plan | Actual Shift Output | Variance / Delta | Compliance % |
|---|---|---|---|---|
| Gross Production Output | 10,080 Pcs | 9,842 Pcs | -238 Pcs | 97.6% Compliance |
| Total Standard Minutes Earned | 185,673 SAM | 181,289 SAM | -4,384 SAM | 97.6% Compliance |
| Non-Productive Time (Total Floor) | ≤ 180 Mins | 185 Mins | +5 Mins | 97.3% Compliance |
| First-Time-Through Quality Rate | ≥ 95.0% | 96.4% | +1.4% | 101.5% Compliance |
22. Consolidated KPI
Executive KPI scorecard summarizing volume, quality, cost efficiency, safety, and compliance.
23. Management Snapshot
Executive summary, shift health score, key decisions executed, and next shift handover priorities.
โฑ๏ธ Non-Productive Time (NPT) Status Console
Real-time operational downtime intelligence synthesizing floor stoppages, incident queues, lost minute economics, root cause diagnostics, and escalation tracking across all 12 operational sewing lines at Plant TX-CHITTAGONG-01.
01. NPT Overview
Plant-wide Non-Productive Time (NPT) telemetry, cumulative floor loss minutes, pacing variance, and overall floor disruption index across Plant TX-CHITTAGONG-01.
02. NPT Live Status
Real-time active downtime broadcast across all 12 operational lines, current lost time pacing, and live mitigation response status.
03. Active Queue
Live triage dispatch queue of active floor stoppage events, assigned technical responders, and target resolution ETAs.
| Queue ID | Line / Station | Problem Description | Severity | Downtime | Assigned Responder | ETA to Clear |
|---|---|---|---|---|---|---|
| #NPT-0814 | Line 08 • Stn 14 | Pegasus Overlock M900 looper micro-friction | P1 CRITICAL | 28 Mins | K. M. Hossain (Senior Mechanic) | < 5 Mins (Test Seams) |
| #NPT-0301 | Line 03 • Stn 01 | Navy Tex 24 spool lot restock buffer warning | P2 WARNING | 12 Mins | S. Alam (Material Feeder) | < 8 Mins (In Transit) |
04. Incident Summary
Shift incident ledger consolidating event count, average duration, affected workstations, and departmental distribution.
05. Lost Minutes
Cumulative shift lost time accounting per line, per section, and variance against allowable industrial engineering allowances.
| Department / Line Zone | Standard Allowance | Actual Lost Minutes | Variance | Lost Piece Equivalent | Compliance |
|---|---|---|---|---|---|
| Lines 01 - 04 (Front Section) | 60 Mins | 42 Mins | -18 Mins Favorable | -136 Pcs | PASS (70%) |
| Lines 05 - 08 (Mid Section) | 60 Mins | 88 Mins | +28 Mins Over | -286 Pcs | INVESTIGATE |
| Lines 09 - 12 (South Section) | 60 Mins | 55 Mins | -5 Mins Favorable | -178 Pcs | PASS (92%) |
06. NPT Category
Categorical classification across Mechanical, Electrical, Material/Trim Shortage, Line Balancing, Quality Rework, and Utility causes.
07. Severity Status
Incident severity categorization (P1 Critical Production Halt, P2 Degraded Speed, P3 Localized Buffer Warning).
08. Line Impact
Line-by-line downtime impact ranking, lost garment output correlation, and recovery pacing schedules across Lines 01-12.
| Line Number | Shift Lost Minutes | Output Lost | Current Pacing | Recovery Plan | Status |
|---|---|---|---|---|---|
| Line 08 | 44 Mins | -142 Pcs | 108 Pcs/Hr | Floater operator + fast helper feed | RECOVERING |
| Line 03 | 22 Mins | -72 Pcs | 116 Pcs/Hr | Direct store cart dispatched | STABILIZING |
| Line 11 | 18 Mins | -58 Pcs | 119 Pcs/Hr | Bobbin winder tension calibrated | NORMALIZED |
| Lines 01, 02, 04, 05, 06, 07, 09, 10, 12 | ≤ 12 Mins avg | -26 Pcs avg | 122 - 128 Pcs/Hr | Standard cadence running | OPTIMAL |
09. Workstation Status
Workstation and machine head status ledger highlighting active stoppage locations, operator relief, and repair status.
10. Root Cause
Verified 5-Why root cause analysis determining primary failure mechanisms and systematic preventative countermeasures.
11. Active Problems
Detailed operational diagnosis of unresolved stoppage events currently impacting live sewing floor throughput.
Technician K. M. Hossain replacing looper set. Calibration tolerance 0.04mm verified. Seam test underway.
Central store feeder dispatched cart #TH-44. Line buffer has 12 minutes remaining before operational impact.
12. Open Incidents
Comprehensive work order tracking for active mechanical and technical incidents undergoing floor diagnosis.
| Incident Ticket | Reported Time | Location | Classification | Status | Assigned Tech |
|---|---|---|---|---|---|
| #INC-202609-08 | 14:12 BST | Line 08 Station 14 | Mechanical • Overlock Looper | UNDER REPAIR (85%) | K. M. Hossain |
| #INC-202609-09 | 14:28 BST | Line 03 Station 01 | Material • Thread Supply | IN TRANSIT | S. Alam |
13. Resolved Incidents
Shift resolved incident archive with start times, clearance timestamps, total elapsed duration, and post-repair FTQ verification.
| Incident Ticket | Line / Station | Resolved Time | Total Downtime | Resolution Action | QA Verification |
|---|---|---|---|---|---|
| #INC-202609-01 | Line 01 • Stn 06 | 09:18 BST | 6 Mins | Replaced worn needle #DBx1 Size 11 | PASSED FTQ |
| #INC-202609-03 | Line 04 • Stn 11 | 10:44 BST | 11 Mins | Adjusted buttonhole trimmer carbide blade | PASSED FTQ |
| #INC-202609-05 | Line 11 • Stn 04 | 11:32 BST | 14 Mins | Calibrated bobbin winder clutch engagement | PASSED FTQ |
14. Pending Actions
Pending corrective maintenance actions, preventative overhaul schedules, and scheduled spare parts changeovers.
15. Response Status
Maintenance and supervisory response time metrics: Mean Time to Respond (MTTResp), dispatch latency, and floor coverage.
16. Escalation Status
Multi-tier floor escalation protocol (Level 1 Line Supervisor, Level 2 Floor Maintenance Head, Level 3 Factory Operations Director).
17. NPT Trend
Hourly downtime pacing trend versus standard allowance curve, historical daily comparison, and weekly reduction progress.
18. Loss Summary
Direct production volume loss, labor cost impact of lost minutes, and capacity efficiency deduction calculations.
19. Problem Priority
Prioritized action matrix ranking current and potential floor risks by production impact, severity, and mitigation urgency.
| Priority | Risk Description | Impact Severity | Probability | Mitigation Protocol | Owner |
|---|---|---|---|---|---|
| P1 High | Overlock looper thermal expansion | High (Line Stoppage) | Low (Periodic) | Synthetic high-temp oil change | Maintenance Head |
| P2 Medium | Aisle congestion during shift changes | Medium (Material Lag) | Medium (Recurring) | Demarcate dedicated feeder corridors | Floor Supervisor |
| P3 Low | Placket folding manual cycle stretch | Low (Micro-stoppage) | High (Continuous) | Deploy pneumatic placket folder | IE Lead |
20. Action Tracking
Accountability ledger tracking remediation commitments, responsible departmental heads, deadlines, and containment audits.
21. NPT Summary
Consolidated shift NPT performance sign-off, net downtime compliance rate, floor stability grade, and next shift handover directives.
๐งต Sewing Floor Operations & Line Control Console
Comprehensive operational telemetry synthesizing sewing line throughput, target vs actual pacing, line-wise efficiency distribution, WIP buffer health, and cut-panel feeding across all 12 sewing lines at Plant TX-CHITTAGONG-01.
01. Sewing Overview
Plant-wide sewing floor operational pulse, total active sewing lines, shift target fulfillment, aggregate floor efficiency, and running garment styles across Plant TX-CHITTAGONG-01.
02. Sewing Floor Status
Real-time production rhythm across all 12 operational sewing lines, floor supervisor coverage, active takt compliance, and overall floor synchronization index.
03. Line-wise Production
Comprehensive line-by-line shift output ledger comparing theoretical target, actual output, hourly cadence, and variance across Lines 01 through 12.
| Line ID | Running Style | Hourly Target | Hourly Actual | Shift Cumulative | Efficiency | Status |
|---|---|---|---|---|---|---|
| Line 01 | LTX-POLO-88 | 120 Pcs | 122 Pcs | 854 Pcs | 88.2% | OPTIMAL |
| Line 04 | LTX-POLO-88 | 120 Pcs | 128 Pcs | 896 Pcs | 94.2% | BENCHMARK |
| Line 08 | LTX-POLO-88 | 120 Pcs | 108 Pcs | 756 Pcs | 78.4% | RECOVERING |
| Line 12 | LTX-POLO-88 | 120 Pcs | 121 Pcs | 847 Pcs | 86.5% | OPTIMAL |
| Lines 02,03,05,06,07,09,10,11 | LTX-POLO-88 | 960 Pcs total | 939 Pcs total | 6,489 Pcs | 84.1% avg | STABLE |
04. Line Target
Engineered line target allocation, standard SAM calculations, takt time benchmarks, and daily shift commitment per line.
05. Line Actual
Live actual completed piece counts verified at end-line inspection stations, pacing rates, and hour-by-hour production tally.
06. Target vs Actual
Variance analysis comparing engineered shift target against verified actual output with positive/negative volume differentials.
| Line Zone | Target Volume | Actual Volume | Volume Variance | Fulfillment Rate | Trend Visual |
|---|---|---|---|---|---|
| Lines 01 - 04 (Front) | 3,360 Pcs | 3,330 Pcs | -30 Pcs | 99.1% | |
| Lines 05 - 08 (Mid) | 3,360 Pcs | 3,232 Pcs | -128 Pcs | 96.2% | |
| Lines 09 - 12 (South) | 3,360 Pcs | 3,280 Pcs | -80 Pcs | 97.6% |
07. WIP Status
Work-in-Progress (WIP) buffer health tracking between workstations, line input buffer, in-line bundle health, and end-line clearance.
08. Style Tracking
Active running style allocation across lines, purchase order references, fabric types, SAM parameters, and upcoming style changeovers.
09. Hourly Output
Hour-by-hour output distribution curve across the 8-hour shift, identifying peak pacing hours and shift transition lulls.
10. Line Efficiency
Labor and line efficiency ratings calculated from earned standard minutes versus actual operator attendance minutes.
11. Line Performance
Composite performance ranking evaluating output volume, efficiency compliance, defect rate, and downtime resilience across all lines.
12. Line Status
Operational operational health classification: Optimal Pacing, Minor Recovery, or Diagnostic Intervention across Lines 01-12.
13. Running Lines
Detailed audit of fully operational sewing lines running at or above 95% target capacity with zero blocking bottlenecks.
| Line | Supervisor | Active Operators | Running SAM | Current Pacing | FTQ Quality |
|---|---|---|---|---|---|
| Line 01 | R. K. Roy | 14 / 14 | 18.42 | 122 Pcs/Hr | 97.2% |
| Line 04 | A. H. Munshi | 14 / 14 | 18.42 | 128 Pcs/Hr | 98.4% |
| Line 12 | M. A. Siddique | 14 / 14 | 18.42 | 121 Pcs/Hr | 96.8% |
14. Idle Lines
Audit of unassigned or non-operational line space, planned maintenance reserves, and setup changeover windows.
15. Bottleneck Lines
Focus diagnosis on lines exhibiting workstation flow impedance, localized bundle buildup, or cycle time standard deviation.
16. Output Progress
Cumulative shift output progress against the linear production plan with projected end-of-shift volume completion.
17. Production Balance
Line balancing efficiency, pitch time uniformity, operator cycle time standard deviation, and station balancing loss.
18. Feeding Status
Input feeding synchronization from cutting room, cut panel bundle availability, trim supply staging, and feeding buffer hours.
19. Critical Alerts
Immediate production alerts highlighting active machine breakdowns, feeding shortages, or severe pitch bottlenecks requiring intervention.
Looper replaced by K. M. Hossain. Test seam in progress. Line restart expected at 14:45 BST.
Feeder cart in transit to Station 01. Line operating safely from local 12-minute buffer.
20. Sewing Summary
Executive sewing floor sign-off, shift volume fulfillment rate, average floor efficiency, stability rating, and Shift 2 handover directives.
๐ฌ Sewing Quality & Defect Analytics Console
Authoritative quality assurance telemetry consolidating in-line roving inspections, end-line DHU metrics, First-Pass Yield (FPY), defect pareto distributions, and CAPA resolution tracking across all 12 operational sewing lines at Plant TX-CHITTAGONG-01.
01. Quality Overview
Plant-wide sewing quality intelligence, overall factory DHU, First-Pass Yield (FPY), total inspected garments, and AQL 1.5 audit compliance across Plant TX-CHITTAGONG-01.
02. Sewing Quality Status
Live operational quality health status across all 12 operational sewing lines, active quality controllers (QC) staffing, and inspection checkpoint coverage.
03. Line-wise DHU
Defects Per Hundred Units (DHU) tracking matrix per sewing line comparing actual defect rate against the 3.0% threshold across Lines 01 through 12.
| Line ID | Inspected Pcs | Defect Count | DHU % | Benchmark (3.0%) | Quality Status |
|---|---|---|---|---|---|
| Line 04 | 896 Pcs | 16 Def | 1.8% | -1.2% Favorable | EXCELLENT |
| Line 01 | 854 Pcs | 19 Def | 2.2% | -0.8% Favorable | OPTIMAL |
| Line 12 | 847 Pcs | 21 Def | 2.5% | -0.5% Favorable | OPTIMAL |
| Line 08 | 756 Pcs | 26 Def | 3.4% | +0.4% Over Threshold | MONITOR |
| Lines 02,03,05,06,07,09,10,11 | 6,489 Pcs | 176 Def | 2.7% avg | -0.3% Favorable | CONTROLLED |
04. Line-wise FPY
First-Pass Yield percentage per line measuring garments passing end-line inspection without requiring alteration or re-stitch.
05. Inspection Quantity
Volume tally of garments presented, in-line roaming checked, 7-point checked, and certified at end-line inspection tables.
06. Pass vs Fail
Direct volumetric ratio comparing first-time certified units against altered and defective units with shift acceptance percentages.
07. Defect Analysis
Deep dive into root failure mechanisms: stitch tension, skipped stitches, broken needle cuts, puckering, uneven placket, and raw edge runs.
| Defect Type | Category | Count | % of Total | Primary Station | Remediation Status |
|---|---|---|---|---|---|
| Skipped Stitch | Workmanship | 68 | 26.4% | Station 14 Overlock | LOOPER REPLACED |
| Uneven Placket Stitch | Workmanship | 54 | 20.9% | Station 04 Collar Attach | FOLDER TUNED |
| Puckering Seam | Machine Tension | 42 | 16.3% | Station 06 Bottom Hem | TENSION ADJUSTED |
| Broken Thread / Run | Material / Thread | 38 | 14.7% | Station 02 Front Prep | NEW LOT ISSUED |
08. Defect Category
Categorical classification across Workmanship (48%), Material/Yarn Imperfections (24%), Machine Calibration (18%), and Measurement Out-of-Tolerance (10%).
09. Defect Rate
Real-time rolling defect rate calculations across morning, post-lunch, and afternoon runs showing trend variances.
10. Major Defects
Audit of high-risk defects that fail buyer acceptance: open seams, skipped stitches on collar band, broken SPI, and needle holes.
11. Defect Pareto
Pareto 80/20 distribution ranking defect occurrences to target highest frequency operational interventions.
12. Line-wise Rejection
Total rejected scrap pieces beyond repair per line with fabric defect and cutting shade correlation.
13. Line-wise Hold
Garment bundles placed on technical hold pending quality manager review, shade matching verification, or measurement audit.
14. Pending Inspection
In-flight inspection buffer queue at end-line tables awaiting roving auditor stamp and clearance to finishing.
15. Quality Trend
Hourly and weekly DHU/FPY quality trajectory showing continuous improvement against historical benchmarks.
16. Style-wise Quality
Defect rate and FPY metrics by specific running product style (e.g. LTX-POLO-88 Mens Pique Polo vs upcoming LTX-POLO-88C).
17. Order-wise Quality
Buyer purchase order quality audit ledger (Next Retail UK PO #LTX-9942) verifying final AQL compliance.
18. Critical Quality Issues
Immediate priority quality alerts requiring mechanical readjustment, needle replacement, or operator re-training.
Technician replaced looper set and needle plate. 18 test seams verified with zero skipped stitches. Re-certified for production.
Fresh Navy thread cones lot #TH-889B checked for friction tension. Dial tension adjusted to 42g standard.
19. Corrective Action Status
CAPA (Corrective and Preventive Action) tracking log documenting root cause elimination, action owners, and verification sign-offs.
20. Quality Summary
Executive quality assurance sign-off, shift AQL 1.5 pass certification, overall floor quality grade, and finishing clearance release.
โ๏ธ Machine Maintenance & Fleet Reliability Console
Authoritative machine telemetry consolidating active breakdowns, MTTR, MTBF, preventative maintenance compliance, spare parts inventory, and technician performance across 188 active production machines at Plant TX-CHITTAGONG-01.
Consolidated plant machine telemetry across 12 sewing lines (188 active machines). Real-time tracking of active breakdowns, mean time to repair, preventative servicing, technician dispatch, spare parts consumption, and machine reliability cadence.
| Machine ID & Model | Location | Problem Mechanism | Downtime | Severity | Technician |
|---|---|---|---|---|---|
| #PEG-M900-0814 Pegasus M900 4-Thd Overlock |
Line 08 • Stn 14 | Looper thermal trip & upper knife timing | 28 mins | CRITICAL | K. M. Hossain |
| #JK-DDL-1104 Juki DDL-9000C Lockstitch |
Line 11 • Stn 04 | Thread tension drift & trimmer knife play | 11 mins | MODERATE | S. Alam |
Mechanic Performance Evaluation Console
Objective 39-point industrial skills appraisal, machine competency audit, and verified supervisor evaluation.
Consolidated appraisal confirms K. M. Hossain (#MEC-104) exceeds operational standards in mechanical diagnostics, preventive maintenance discipline, and rapid floor dispatch. Recommended for Senior Factory Maintenance Specialist certification upon completion of module ELEC-402.
| Part Description | Machine | Req | Status |
|---|---|---|---|
| Pegasus Looper Set #JK-SP-LP-900 |
Line 08 Overlock | 1 Set | MOUNTED |
| Carbide Trimming Knife #JK-SP-KN-9000 |
Line 11 Lockstitch | 1 Pc | ISSUED |
| PTFE Presser Foot #FT-SP-PTFE-42 |
Line 04 Activewear | 2 Pcs | RESERVED |
Thermal motor overload triggered by upper looper timing friction. Unit taken offline for 28 mins. Reserve assembly mounted. Sr. Mechanic Hossain completing synchronizer verification.
| Event Date & Time | Machine Asset | Location | Fault Classification | Action & Spare Consumed | Downtime | Lead Tech | Verification Status |
|---|---|---|---|---|---|---|---|
| Today • 14:22 BST | Pegasus M900 Overlock | Line 08 • Stn 14 | Looper thermal trip & bearing play | Mounted looper set #JK-SP-LP-900 | 28 mins | K. M. Hossain | Testing (85%) |
| Today • 11:40 BST | Juki DDL-9000C Lockstitch | Line 11 • Stn 04 | Thread trimming clearance play | Replaced knife edge & zeroed sensor | 11 mins | S. Alam | Closed |
| Today • 09:15 BST | Gerber Paragon Cutter | Cutting Bay 02 | Vacuum table micro-seal pressure drop | Replaced polyurethane micro-seal | 12 mins | M. R. Talukder | Closed |
| Today • 08:30 BST | Brother S-7300A Lockstitch | Line 03 • Stn 07 | Electronic feed pulse latency | Stepping motor encoder re-synced | 8 mins | A. Siddique | Closed |
| Today • 07:45 BST | Yamato VG2700 Interlock | Line 05 • Stn 11 | Oil wiper spring tension fatigue | Installed OEM wiper spring #WPR-27 | 14 mins | K. Rahman | Closed |
Factory machine fleet operates with strong overall availability at 98.9% (186 of 188 units operational). Cumulative shift downtime of 63 minutes is dominated by the Line 08 Pegasus M900 thermal trip (28 mins), which is currently at 85% repair completion with looper swap verified. Machine-induced volume loss of -418 pcs will be recovered through post-repair pacing and buffer reserves. MTTR remains healthy at 18.2 minutes (<20.0m target) and MTBF stands at 168.4 hours. PM compliance is 98.2% with 0 overdue tasks. All technical labor is fully deployed and zero critical parts shortages exist.
๐ IE | Line Balancing & Quick Changeover (QCO) Console
Consolidated industrial engineering telemetry encompassing standard allowable minutes (SAM), pitch balance distributions, bottleneck operation tracking, operator skill matrix, changeover tooling preparation, and technical line release auditing across 12 sewing lines.
IE | Line Balance | QCO Report Floor Intelligence
Industrial Engineering Telemetry • Line Balancing Optimization • Quick Changeover (QCO) Engineering Console
| Section / Phase | Standard Time (SAM) | Allowance % | Allocated SAM | Op Count | Target Pcs/Hr | Variance vs Benchmark |
|---|---|---|---|---|---|---|
| Collar & Placket Prep | 5.20 min | 12.5% | 5.85 SAM | 4 Ops | 103 pcs | -0.12 SAM (Optimized) |
| Front & Back Assembly | 4.80 min | 13.0% | 5.42 SAM | 4 Ops | 111 pcs | 0.00 SAM (Parity) |
| Sleeve & Side Seam | 4.10 min | 12.0% | 4.59 SAM | 3 Ops | 130 pcs | -0.08 SAM (Optimized) |
| Bottom Hem & Trim Finishing | 2.25 min | 14.0% | 2.56 SAM | 3 Ops | 234 pcs | +0.20 SAM (Minor Lag) |
| TOTAL GARMENT SAM | 16.35 min | 12.7% (Avg) | 18.42 SAM | 14 Ops | 120 pcs/hr | Verified Target Benchmark |
| Station | Assigned Operation | Machine Type | Op SAM | Theoretical Output | Allocated Operator | Status |
|---|---|---|---|---|---|---|
| WS-01 | Fuse Interlining on Placket | Continuous Fusing Press | 1.15 SAM | 52 pcs/hr | Nazmul Huda (ID-2189) | Normal Flow |
| WS-02 | Make Collar Leaf & Turn | 1-Needle Lockstitch UBT | 1.45 SAM | 41 pcs/hr | Shahana Begum (ID-3310) | Normal Flow |
| WS-03 | Join Shoulder with Clear Elastic | 4-Thread Overlock (Direct Drive) | 1.20 SAM | 50 pcs/hr | Mizanur Rahman (ID-1904) | Normal Flow |
| WS-04 | Attach Collar to Body Neck (Critical) | 1-Needle Lockstitch UBT | 1.72 SAM (0.54 min) | 35 pcs/hr | Fatema Khatun (ID-4402) | Bottleneck Watch |
| WS-05 | Attach Ribbed Sleeve Cuff | 4-Thread Overlock High-Speed | 1.30 SAM | 46 pcs/hr | Rina Akter (ID-5512) | Normal Flow |
| WS-06 | Hem Bottom Sweep & Side Slits | Interlock Flatlock Cylinder Bed | 1.25 SAM | 48 pcs/hr | Abul Kashem (ID-1108) | Normal Flow |
Low variance across non-critical stations indicates uniform task loading.
Theoretical maximum efficiency 100% - 84.6% achieved = 15.4% idle loss.
| Line ID | Line Name | Allocated SAM | Cycle Time | Balancing Eff. % | Line Status | Pacing vs Target |
|---|---|---|---|---|---|---|
| L-01 | Polo Line 01 (Core Knit) | 18.42 SAM | 31.8s | 88.2% | Optimum Balance | +3.2% vs Plan |
| L-04 | Polo Line 04 (High Performance) | 18.42 SAM | 29.4s | 94.2% | Top Factory Performer | +9.2% vs Plan |
| L-08 | Polo Line 08 (Feeders Constrained) | 18.42 SAM | 36.1s | 78.4% | Action Required | -6.6% vs Plan |
| L-12 | Polo Line 12 (Export Dedicated) | 18.42 SAM | 32.0s | 86.5% | Stable Run | +1.5% vs Plan |
| Severity | Station ID | Operation Name | Observed Cycle | Takt Target | WIP Buffer Accumulation | Root Cause Factor |
|---|---|---|---|---|---|---|
| CRITICAL | WS-04 | Attach Collar to Body Neck | 32.4 sec | 30.0 sec | 34 pcs upstream queue | Curved seam handling & collar notch alignment |
| MODERATE | WS-02 | Make Collar Leaf & Turn | 30.8 sec | 30.0 sec | 18 pcs upstream queue | Manual corner trimming before turn |
| MONITOR | WS-06 | Bottom Hem & Slit Tack | 29.5 sec | 30.0 sec | 8 pcs upstream queue | Fabric curl on single jersey batch #401 |
| Emp ID | Operator Name | Assigned Line | Primary Operation | Rating | Secondary Capability | Skill Score |
|---|---|---|---|---|---|---|
| ID-4402 | Fatema Khatun | Line 04 | Attach Collar to Body Neck | Grade A | Placket Topstitch & Box | 94% |
| ID-2189 | Nazmul Huda | Line 01 | Fuse Interlining on Placket | Grade A | Fusing Machine Maintenance | 91% |
| ID-3310 | Shahana Begum | Line 04 | Make Collar Leaf & Turn | Grade B | Cuff Hemming | 85% |
| ID-1904 | Mizanur Rahman | Line 08 | Join Shoulder with Elastic | Grade B | Side Seam Joining | 82% |
| ID-5512 | Rina Akter | Line 01 | Attach Ribbed Sleeve Cuff | Grade A | Sleeve Setting Overlock | 93% |
| ID-1108 | Abul Kashem | Line 12 | Bottom Hem & Slit Tack | Grade B | Flatlock Binding | 84% |
| Line ID | Hourly Target | Actual Output (Pcs/Hr) | Productivity Ratio | Variance | Efficiency % | Benchmark Status |
|---|---|---|---|---|---|---|
| Line 01 | 120 pcs | 122 pcs | 101.6% | +2 pcs | 88.2% | Above Target |
| Line 04 | 120 pcs | 128 pcs | 106.7% | +8 pcs | 94.2% | High Achiever |
| Line 08 | 120 pcs | 108 pcs | 90.0% | -12 pcs | 78.4% | Under Pacing |
| Line 12 | 120 pcs | 121 pcs | 100.8% | +1 pc | 86.5% | On Schedule |
| Department | Nominal Capacity | Utilized Capacity | Buffer Headroom | Utilization Rate | Risk Factor |
|---|---|---|---|---|---|
| Cutting Room Auto-Spreading | 14,500 pcs/day | 12,800 pcs/day | 1,700 pcs/day | 88.3% | Low Risk |
| Sewing Lines Assembly | 12,000 pcs/day | 11,344 pcs/day | 656 pcs/day | 94.5% | Optimal Load |
| Thread Trimming & Washing | 13,000 pcs/day | 11,200 pcs/day | 1,800 pcs/day | 86.2% | Low Risk |
| Final Pressing & Poly-Packing | 12,500 pcs/day | 11,100 pcs/day | 1,400 pcs/day | 88.8% | Low Risk |
Evaluated across 14 workstations. Zero prolonged inter-station starvations observed.
Ideal operational buffer range: 12 – 18 pcs per station.
| Milestone | Scheduled BST | Owner / Lead | Action Item | Readiness % | Stage Status |
|---|---|---|---|---|---|
| T-2 Hours | 14:00 BST | Engr. Tariq Mahmud | Machine staging & specialized folder verification | 100% | Completed |
| T-1 Hour | 15:00 BST | K. M. Hossain | Pre-cut panels & trim package dispatch to line buffer | 95% | On Schedule |
| T-0 Switch | 16:00 BST | R. Kabir & Team | Thread swap, gauge adjustment & mock trial piece | 85% | Ready for Trigger |
| T+28 Mins | 16:28 BST | Quality Lead & IE Lead | First piece approval & line release to bulk | -- | Pending Switch |
| Machine Category | Current Active | Required for Style #P-88 | Delta / Net Machine Shift | Sourcing Origin | Availability |
|---|---|---|---|---|---|
| 1-Needle Lockstitch UBT | 8 Machines | 7 Machines | -1 Machine (Standby) | Floor Active | 100% Ready |
| 4-Thread High Speed Overlock | 4 Machines | 4 Machines | 0 Change | Floor Active | 100% Ready |
| Flatlock Cylinder Bed | 2 Machines | 2 Machines | 0 Change | Floor Active | 100% Ready |
| Button Sewer & Holer Combo | 0 Machines (Central) | 1 In-line Unit | +1 Machine (Transfer) | Maintenance Central Pool | Staged at Line Bay |
| Name | Role | Department | Specialty | Assigned QCO Line | Contact / Radio |
|---|---|---|---|---|---|
| Engr. Tariq Mahmud | Lead IE Engineer | Industrial Engineering | SMED Methodology & Line Balance | Factory-Wide Lead | Radio Ch 01 |
| K. M. Hossain | Senior Maintenance Tech | Plant Engineering | Pneumatics & Electronic Motors | Lines 01 - 04 | Radio Ch 02 |
| R. Kabir | Specialist Sewing Mechanic | Mechanical Maintenance | Lockstitch & Overlock Gauge Set | Lines 05 - 08 | Radio Ch 02 |
| S. Alam | Folder & Attachment Tech | Tooling & Attachments | Custom Piping & Hemming Guides | Lines 09 - 12 | Radio Ch 03 |
| Technician | Current Floor Location | Current Task | Readiness Status | ETA to Line 08 Switch |
|---|---|---|---|---|
| Engr. Tariq Mahmud | IE Control Station / Line 04 | SMED Time-Study Verification | Ready on Call | Immediate |
| K. M. Hossain | Line 02 Mechanic Bay | Pre-aligning folders for contrast rib | Ready on Call | 2 mins |
| R. Kabir | Line 08 Sub-station | Needle bar height check on WS-04 | On-Site Active | 0 mins (On-Site) |
| S. Alam | Tooling & Attachments Room | Testing placket guide clearance | Pre-staging Complete | 3 mins |
| Setup Phase | Tasks Included | Target Progress | Actual Progress | Visual Bar | Status |
|---|---|---|---|---|---|
| 1. External Setup (SMED) | Material prep, tooling staged, mock test | 100% | 100% | Finished | |
| 2. Mechanical Calibration | Stitch density, looper timing, needle gauge | 90% | 92% | Ahead | |
| 3. Trial Run & Mock Garment | 1st piece run through all 14 stations | 80% | 83% | In Progress |
Lines 01-04 switch at 16:00, Lines 05-08 switch at 16:45 to prevent technical resource bottlenecks.
All thread threading, folder bolting, and bobbin loading done before line stop.
Reaching 100% standard rate (120 pcs/hr) by Hour 3.
| Operation ID | Stitch Type (ISO) | Needle Spec | SPI (Stitches / Inch) | Thread Tension Top/Bottom | Differential Feed |
|---|---|---|---|---|---|
| OP-01 (Fuse Placket) | Thermal Bonding | N/A | 140°C @ 3.5 bar | Dwell: 12 sec | Belt: 4.2 m/min |
| OP-02 (Make Collar) | ISO 301 Lockstitch | Groz-Beckert #10 SES | 14 - 15 SPI | Tension: 35g / 22g | Neutral 1:1 |
| OP-03 (Join Shoulder) | ISO 514 Overlock | Organ DCx27 #11 | 16 SPI | Tension: 20g / 15g | Gathering 1:1.2 |
| OP-04 (Attach Collar) | ISO 301 Lockstitch | Groz-Beckert #11 SES | 14 SPI | Tension: 38g / 25g | Neutral 1:1 |
| Folder Code | Target Station | Attachment Description | Material Guide Width | Setup Status | Verified By |
|---|---|---|---|---|---|
| FLD-PLK-04 | WS-01 / WS-02 | Double Fold Contrast Placket Folder | 28 mm Finished | Mounted & Aligned | S. Alam |
| FLD-COL-08 | WS-04 | Collar Notch Centering Guide Attachment | Elastic insert 6 mm | Calibrated | S. Alam |
| FLD-HEM-12 | WS-06 | Bottom Hem Flatlock Hemmer with Guide | 20 mm Hem Fold | Mounted & Tested | R. Kabir |
Placket fusing, collar leaf stitch, turn & press, shoulder join.
Attach collar band, stitch neck tape, topstitch placket box.
Attach sleeve flat, close side seam, attach rib sleeve cuff.
Bottom slit binding, hem bottom sweep, bartack & label.
| Log ID | Sub-assembly | Reported Technical Issue | Severity | Corrective Action Implemented | Status |
|---|---|---|---|---|---|
| TI-QCO-01 | WS-04 (Collar Join) | Minor fabric pucker on collar curve during high speed | MODERATE | Presser foot pressure lowered from 4.5kg to 3.2kg; silicone lubricant pad added | Resolved |
| TI-QCO-02 | WS-01 (Fusing Press) | Temperature fluctuation ±8°C on outer heating zone | MODERATE | Thermocouple probe recalibrated by K. M. Hossain; temperature verified stable | Resolved |
| Line ID | Current Production Run | Pre-Release Signoff | Technical Lead Approval | Release Authorization |
|---|---|---|---|---|
| Line 01 - 04 | Finalizing batch run LTX-POLO-88 | Signed (QA Lead) | Signed (IE Lead) | AUTHORIZED (16:00 BST) |
| Line 05 - 08 | WIP tail clearance in progress | Signed (QA Lead) | Pending Final Check | SCHEDULED (16:45 BST) |
| Line 09 - 12 | Standard bulk progression | Under Preparation | Scheduled | SCHEDULED (17:30 BST) |
Relocating thread nippers to magnetic chest mounts saved 1.8 seconds per cycle on Collar Preparation.
Eliminated manual bundle handoffs between Station 03 and Station 04, reducing idle wait by 4.2%.
| Rec # | Focus Station | IE Proposed Action | Projected Impact | Implementation Cost | Priority |
|---|---|---|---|---|---|
| REC-01 | WS-04 (Collar) | Install synchronized pneumatic edge-guide | Cycle time reduced from 32.4s to 29.8s | $180 / station | P1 - Immediate |
| REC-02 | WS-02 (Collar Turn) | Deploy automated mechanical point turner | Cycle time reduced from 30.8s to 27.5s | $240 / station | P2 - Next Shift |
| REC-03 | Factory Floor | Expand digital takt pacing lights to all lines | Overall balancing efficiency +2.1% | $650 total floor | P3 - Weekend |
Cycle time exceeds takt by 2.4s; causes upstream buffer of 34 pcs and throttles Line 08 efficiency to 78.4%.
Relieves operator Fatema Khatun from manual notch alignment, bringing effective cycle to 29.5s.
Floor balancing efficiency steady at 84.6% (target 85.0%). Line 04 paces at 94.2% while Line 08 bottleneck is actively mitigated.
Style #P-88 (LTX-POLO-88C) transition cleared for 16:00 BST release with 6 technicians assigned and all folders pre-mounted.
Industrial Engineering Floor Dispatch • Ext: 4410 • Leadirftex Central IE
๐ฅ Factory Attendance & Manpower Intelligence Console
Authoritative workforce telemetry consolidating biometric gate swipes, daily attendance ratios, absenteeism diagnostics, departmental staffing allocations, overtime authorizations, and floater deployment tracking across Plant TX-CHITTAGONG-01.
Real-time biometric turnstile badge telemetry at main entry portals (Gates 01, 02 & Technical Portal).
| Department | Roster Headcount | Actual Present | Absent | Floater In | Effective Strength | Status |
|---|---|---|---|---|---|---|
| Sewing Operations | 240 | 232 | 8 | +6 | 238 / 240 | 99.2% Balanced |
| Cutting & Spreading | 54 | 52 | 2 | +2 | 54 / 54 | 100% Balanced |
| Washing & Finishing | 72 | 69 | 3 | +2 | 71 / 72 | 98.6% Balanced |
| Quality Assurance | 42 | 41 | 1 | +1 | 42 / 42 | 100% Balanced |
| Plant Maintenance | 18 | 18 | 0 | 0 | 18 / 18 | 100% Balanced |
| Store & Materials | 34 | 33 | 1 | +1 | 34 / 34 | 100% Balanced |
| Packaging & Dispatch | 40 | 37 | 3 | +2 | 39 / 40 | 97.5% Pacing |
| Leave Classification | Yearly Entitlement | Used Year-to-Date | Remaining Balance | Current Shift Active | Compliance Audit |
|---|---|---|---|---|---|
| Earned / Annual Leave (EL) | 16 Days / Yr | 8.4 Days Avg | 7.6 Days | 0 Today | Fully Audited |
| Casual Leave (CL) | 10 Days / Yr | 4.2 Days Avg | 5.8 Days | 7 Today | Approved |
| Medical / Sick Leave (SL) | 14 Days / Yr | 3.8 Days Avg | 10.2 Days | 4 Today | Doctor Certified |
| Festival / Statutory Leave | 11 Days / Yr | 6.0 Days YTD | 5.0 Days | 0 Today | Gazette Compliant |
| Department | Planned | Present | Absent | Attendance % | Late Clock-ins | Action |
|---|---|---|---|---|---|---|
| Sewing Operations | 240 | 232 | 8 | 96.7% | 4 | |
| Cutting & Spreading | 54 | 52 | 2 | 96.3% | 1 | |
| Washing & Finishing | 72 | 69 | 3 | 95.8% | 1 | |
| Quality Assurance | 42 | 41 | 1 | 97.6% | 0 | |
| Plant Equipment & Maintenance | 18 | 18 | 0 | 100.0% | 0 | |
| Store & Raw Materials | 34 | 33 | 1 | 97.1% | 1 | |
| Packaging & Dispatch | 40 | 37 | 3 | 92.5% | 1 |
Detailed physical line distribution of direct operators and station helpers across lines 01 to 12.
| Sewing Line | Running Style | Target Operators | Present Operators | Helpers | Line Strength | Coverage Status |
|---|---|---|---|---|---|---|
| Line 01 | LTX-POLO-88 | 20 | 20 | 4 | 24 / 24 | 100% Full |
| Line 02 | LTX-POLO-88 | 20 | 19 | 4 | 23 / 24 | +1 Floater Active |
| Line 03 | LTX-TEE-04 | 20 | 20 | 4 | 24 / 24 | 100% Full |
| Line 04 | LTX-HOOD-12 | 20 | 20 | 4 | 24 / 24 | 100% Full |
| Line 05 | LTX-TEE-04 | 20 | 19 | 4 | 23 / 24 | +1 Floater Active |
| Line 06 | LTX-JOG-09 | 20 | 20 | 4 | 24 / 24 | 100% Full |
| Line 07 | LTX-POLO-88 | 20 | 20 | 4 | 24 / 24 | 100% Full |
| Line 08 | LTX-POLO-88 | 20 | 18 | 4 | 22 / 24 | +2 Floaters Deployed |
| Lines 09–12 | Various Styles | 80 | 78 | 16 | 94 / 96 | Floater Buffer Active |
| Employee ID | Employee Name | Department | Clock-In Time | Minutes Late | Supervisor Action |
|---|---|---|---|---|---|
| #OP-1048 | R. Sultana | Sewing (Line 08) | 08:18 BST | +18 mins | Verbal Warning Recorded • Shift Extended |
| #OP-1092 | M. Hasan | Sewing (Line 02) | 08:22 BST | +22 mins | Transit Delay Verified • Grace Granted |
| #OP-1140 | B. Akhter | Cutting (Bay 01) | 08:16 BST | +16 mins | Verbal Warning Recorded |
| #OP-1205 | J. Mia | Packaging (Bay 02) | 08:25 BST | +25 mins | Shift Extended 30m |
01 Machines Overview
Consolidated floor machine inventory, running vs idle state, active breakdowns, and baseline equipment health telemetry.
02 Factory Machine Inventory
Complete factory-wide equipment asset register with serial numbers, asset tags, and commissioning timestamps.
| Asset Tag | Serial Number | Machine Category | Model Series | Assigned Line | Status | Condition | Last Serviced |
|---|---|---|---|---|---|---|---|
LTX-M-0104 |
JK-2024-88492-BD |
Lockstitch Single-Needle | Juki DDL-9000C-SMS | Line 04 (Front Placket) | Running | Grade A (Optimal) | 12 Sep 2026 |
LTX-M-0219 |
PG-2023-41098-JP |
Overlock 4-Thread | Pegasus M952-54 | Line 02 (Side Seam) | Running | Grade A (Optimal) | 10 Sep 2026 |
LTX-M-0308 |
YM-2024-55021-JP |
Flatlock Cylinder Bed | Yamato VG2700 | Line 08 (Collar Join) | Breakdown | Grade B (Looper Issue) | Active Work Order #991 |
LTX-M-0412 |
BR-2025-11029-JP |
Direct-Drive Lockstitch | Brother S-7200C | Line 03 (Sleeve Hem) | Breakdown | Grade B (Needle Bar) | Active Work Order #992 |
LTX-M-0588 |
JK-2024-77102-BD |
Electronic Bartack | Juki LK-1900BN | Line 06 (Pocket Bartack) | Running | Grade A (Optimal) | 14 Sep 2026 |
LTX-M-0604 |
JK-2023-99014-BD |
Overlock 5-Thread | Juki MO-6814S | Buffer Reserve (Bay B) | Idle Standby | Grade A (Ready) | 08 Sep 2026 |
03 Machine Category
Distribution of machine fleet across Lockstitch, Overlock, Flatlock, Buttonhole, Bartack, and Specialized units.
| Machine Category | Total Count | Running | Idle Standby | Breakdown | Utilization Rate | Primary Operations |
|---|---|---|---|---|---|---|
| Lockstitch (Single & Double Needle) | 148 Units | 144 Units | 3 Units | 1 Unit | 97.3% | Collar Join, Placket, Topstitch, Hemming |
| Overlock (4-Thread & 5-Thread) | 84 Units | 82 Units | 2 Units | 0 Units | 97.6% | Side Seam, Sleeve Join, Overedge |
| Flatlock / Interlock (Cylinder & Flat) | 46 Units | 43 Units | 2 Units | 1 Unit | 93.5% | Bottom Hem, Sleeve Rib, Coverstitch |
| Specialized (Bartack, Buttonhole, Button Attach) | 22 Units | 21 Units | 1 Unit | 0 Units | 95.5% | Pocket Reinforcement, Button Attach, Eyelet |
| Finishing & Cutting Auxiliary Support | 12 Units | 12 Units | 0 Units | 0 Units | 100.0% | Band Knife, Thread Sucker, Snap Fastener |
04 Machine Model
Model-level inventory specifications including Juki DDL-9000C, Brother S-7200C, Pegasus M952, and Yamato VG2700.
05 Machine Location
Floor physical location tracking across Shed 01, Shed 02, Mezzanine Level, and Central Technical Workshop.
06 Section-wise Machine
Workstation and section allocation across Collar, Sleeve, Body Assembly, Hemming, and Finishing prep.
07 Line-wise Machine
Sewing line equipment distribution and active running density across all 12 operational production lines.
| Sewing Line | Allocated Fleet | Active Running | Idle | Down | Line OEE | Target Style |
|---|---|---|---|---|---|---|
| Line 01 | 26 Units | 26 | 0 | 0 | 98.2% | LTX-POLO-01 |
| Line 02 | 26 Units | 26 | 0 | 0 | 97.8% | LTX-POLO-02 |
| Line 03 | 26 Units | 25 | 0 | 1 | 92.4% | LTX-TEE-03 (Needle Bar Jam) |
| Line 04 | 26 Units | 26 | 0 | 0 | 96.5% | LTX-TEE-04 |
| Line 05 | 26 Units | 26 | 0 | 0 | 98.0% | LTX-HOOD-05 |
| Line 06 | 26 Units | 26 | 0 | 0 | 97.1% | LTX-HOOD-06 |
| Line 07 | 26 Units | 26 | 0 | 0 | 98.4% | LTX-PANT-07 |
| Line 08 | 26 Units | 25 | 0 | 1 | 91.8% | LTX-POLO-88C (Looper Trip) |
| Line 09 | 25 Units | 25 | 0 | 0 | 96.9% | LTX-SPORT-09 |
| Line 10 | 25 Units | 25 | 0 | 0 | 97.5% | LTX-SPORT-10 |
| Line 11 | 25 Units | 25 | 0 | 0 | 96.0% | LTX-JACK-11 |
| Line 12 | 25 Units | 25 | 0 | 0 | 97.2% | LTX-JACK-12 |
| TOTAL LINES | 308 Units | 302 Units | 0 | 2 Units | 96.8% Composite | Fleet + 4 Workshop Units |
08 Machine Quantity
Total verified machine count verification ledger: 312 installed production units across the plant.
09 Running Machines
Active live operational machinery generating earned standard minutes on the sewing lines (302 units / 96.8%).
10 Idle Machines
Buffer standby and changeover stage machinery ready for operator reassignment (8 units).
11 Breakdown Machines
Active equipment failures under emergency mechanical or electrical intervention (2 units: Line 08 & Line 03).
12 Available Machines
Total functional machinery available for immediate line allocation or capacity expansion (310 units).
13 Layout-ready Machines
Calibrated buffer fleet configured with attachments and folders for incoming style changeovers (14 units).
14 Machine Allocation
Workstation-to-machine assignment mapping aligning theoretical pitch with machine availability.
15 Line Capacity
Rated hourly and shift standard minute capacity based on active installed machine fleets per line.
16 Machine Utilization
Overall equipment effectiveness (OEE) and operational run-time ratios across production shifts (96.8%).
17 Machine Condition
Physical health classification: Grade A (Excellent: 248), Grade B (Good: 58), Grade C (Fair: 6).
18 Machine Lifecycle
Asset depreciation, lifecycle stage tracking, and planned capital replacement horizon indicators.
19 Installation Status
Anchoring, pneumatic line coupling, electrical busbar connection, and IoT gateway telemetry status.
20 Age & Usage
Operating hour accumulation meters and calendar service age since commissioning date.
21 Machine History
Historical service logs, preventive maintenance cycles, technician sign-offs, and breakdown records.
22 Repair-required Machines
Machines tagged with work orders requiring scheduled mechanical servicing or part change.
23 Parts-required Machines
Machines pending component replacement with requisition orders logged in the Central Store.
24 Required Spare Parts
Critical spare component requisition register including rotary hooks, needles, loopers, and sensors.
| Part Number | Description | Applicable Machine | Store Stock | Required | Deficit | Priority |
|---|---|---|---|---|---|---|
JK-SP-HOOK-ROT-9 |
Titanium Full-Rotary Hook Assembly | Juki DDL-9000C | 4 Units | 2 Units | 0 (Stocked) | Routine |
YM-SP-LOOP-LW-27 |
Precision Lower Looper (Hardened Steel) | Yamato VG2700 | 1 Unit | 2 Units | -1 Unit | High / Urgent |
BR-SP-NBAR-72 |
Needle Bar Assembly with Clamp Screw | Brother S-7200C | 3 Units | 1 Unit | 0 (Stocked) | In Transit |
PG-SP-FEED-DOG-54 |
Differential Feed Dog Set (Fine Tooth) | Pegasus M952 | 6 Sets | 2 Sets | 0 (Stocked) | Routine |
25 Parts Availability
Central maintenance store inventory levels for high-wear sewing attachments and electronics.
26 Parts Shortage
Deficit inventory alerts on critical parts with automated supplier replenishment escalation.
27 Repair Readiness
Technician squad staging, tool cart readiness, and spare part staging for pending work orders.
28 Maintenance Dependency
Cross-functional dependency log linking machine status to the Machine Maintenance department schedule.
29 Machine Replacement Status
End-of-life replacement pipeline, decommission schedules, and new asset procurement status.
30 Critical Machines
High-impact single-point-of-failure equipment with zero line redundancy requiring 24/7 priority monitoring.
| Critical Asset | Process Function | Redundancy Factor | Line Risk Exposure | Health Index | Mitigation Contingency |
|---|---|---|---|---|---|
| PFAFF 8312 Ultrasonic Seam Welder | Bonded Waterproof Seams (Lines 11 & 12) | Single Point | High (Style Halt Risk) | 98.2% | Dedicated Workshop Spare Ultrasonic Transducer |
| Juki APW-896 Automatic Pocket Welter | Jacket Welt Pocket Automation | Single Point | High (Manual fallback slows line 60%) | 96.5% | OEM Local Technical Standby Contract |
| Lectra Vector Automated CNC Cutter | Central Cutting Room Bulk Feed | Dual Unit (2x) | Critical (All 12 Lines Dependent) | 99.1% | Blade calibration and preventive service weekly |
31 Factory Machine Summary
Executive machine health summary, central maintenance dispatch contacts, and plant engineering sign-off.
01 Overview
Consolidated cutting floor performance, shift cut output, pending volume, spreading readiness, and sewing feeding buffer status.
02 Cutting Plan
Master cutting production plan by table, shift, style, and fabric lot allocation across operational cutting tables.
| Plan ID | Cutting Table | Style Number | Fabric Lot # | Target Pcs | Cut Pcs | Variance | Status |
|---|---|---|---|---|---|---|---|
CP-2026-091 |
Table 01 (Gerber Paragon) | LTX-POLO-88C | FAB-LOT-992A |
8,500 | 8,200 | -300 Pcs | Cutting |
CP-2026-092 |
Table 02 (Lectra Vector) | LTX-TEE-04 | FAB-LOT-881B |
7,000 | 6,100 | -900 Pcs | Cutting |
CP-2026-093 |
Table 03 (High-Ply Spreader) | LTX-HOOD-05 | FAB-LOT-774C |
6,750 | 5,150 | -1,600 Pcs | Spreading |
03 Order & Style
Active style cutting matrix featuring LTX-POLO-88C, LTX-TEE-04, LTX-HOOD-05, and PO delivery commitments.
04 Cut Quantity
Total pieces cut to date: 19,450 pcs across all active styles with verified piece-count barcode validation.
05 Target vs Actual
Daily cutting target (22,250 pcs) vs actual cut achievement (19,450 pcs / 87.4% shift progression).
06 Cutting Progress
Real-time lay-by-lay and style-by-style cutting completion progress meters against hourly line feeding schedules.
07 Marker Status
CAD marker creation, nesting approval, digital plotter queue, and automated nesting optimization ledger.
08 Marker Efficiency
Overall marker fabric utilization percentage: 86.8% achieved (exceeding standard 85.5% baseline target).
09 Fabric Readiness
Fabric relaxation, roll shade lot inspection, shrinkage testing, and spreading table staging readiness (98.2%).
10 Fabric Allocation
Roll issuance register from Central Raw Materials Store to Cutting Room with batch numbers and shade codes.
11 Lay Plan
Multi-ply fabric spreading layout plans specifying ply counts (120 plies), table length (14.5m), and color mix.
12 Cutting Schedule
Hour-by-hour cutting table schedule coordinating spreader tables, CNC cutter passes, and bundle ticketing.
13 Pending Quantity
Remaining uncut garments required to fulfill active cutting work orders (2,800 pcs across active POs).
14 Cutting Queue
Prioritized queue of upcoming production styles waiting for CAD marker release and fabric staging.
15 Feeding Status
Buffer status of cut bundles feeding operational sewing lines: 1.8 shifts feeding reserve established.
| Sewing Line | Fed Style | Ready Bundles | Feeding Buffer | Transit Mode | Line Feeding Status |
|---|---|---|---|---|---|
| Line 01 | LTX-POLO-01 | 140 Bundles | 2.1 Shifts | AMR Automated | Normal |
| Line 02 | LTX-POLO-02 | 125 Bundles | 1.9 Shifts | AMR Automated | Normal |
| Line 04 | LTX-TEE-04 | 110 Bundles | 1.8 Shifts | Overhead Conveyor | Normal |
| Line 08 | LTX-POLO-88C | 115 Bundles | 1.7 Shifts | Overhead Conveyor | Normal |
| Line 11 | LTX-JACK-11 | 95 Bundles | 1.4 Shifts | Manual Cart | Replenishing |
16 Bundle Preparation
Numbering, ticketing, fusing, sorting, and bundle packaging with RFID lot tags for AMR floor transfer.
17 Cutting Line Status
Real-time status of Cutting Tables 01 to 06, automatic CNC knives, manual band knives, and end cutters.
18 Shortage Status
Fabric roll deficit or pattern piece recut ledger for damaged fabric plies with rapid recut resolution.
19 Delay Alerts
Cutting obstacle alerts, machine blade overheating warnings, fabric defect flags, and resolution dispatches.
| Alert Code | Severity | Trigger Description | Affected Unit | Impact | Mitigation Status |
|---|---|---|---|---|---|
ALT-CUT-01 |
Normal / Cleared | Cutting buffer cleared; 1.8 shifts feeding reserve established | All 12 Sewing Lines | Nominal | 0 QA lots on hold • Feeding active |
ALT-CUT-02 |
Notice | Line 11 bundle buffer low (<15 bundles remaining in buffer rack) | Line 11 Buffer Rack | Low | Priority AMR dispatch staged from Table 04 |
20 Cutting Summary
Executive cutting floor scorecard, shift handover sign-off, and Central Cutting Floor Dispatch ledger.
01 Store & Materials Overview
Consolidated warehouse stock health, fabric buffer status, trims matching ratio, line feeding coverage, and shortage alerts.
02 Fabric Status
In-warehouse fabric inventory tracking (100% available with 48h buffer) across single jersey, pique knit, and heavy french terry.
| Fabric Lot # | Fabric Type & Composition | Allocated Style | Warehouse Stock | Reserved Cutting | Free Balance | Status |
|---|---|---|---|---|---|---|
FAB-LOT-992A |
100% Combed Cotton Single Jersey (180 GSM) | LTX-POLO-88C | 14,200 kg | 8,500 kg | 5,700 kg | 100% Ready |
FAB-LOT-881B |
95/5 Cotton/Elastane Rib Knit (220 GSM) | LTX-TEE-04 | 9,800 kg | 6,100 kg | 3,700 kg | 100% Ready |
FAB-LOT-774C |
380 GSM Heavy French Terry Knit (Compact Combed) | LTX-HOOD-05 | 18,500 kg | 11,200 kg | 7,300 kg | 100% Ready |
03 Fabric Availability
Physical stock availability verified against cutting room release orders (Zero fabric starvation across all 12 lines).
04 Fabric Allocation
Fabric roll issuance ledger from Central Raw Materials Store to Cutting Tables 01 to 06 with lot and shade numbers.
05 Trims Status
Trims and labels matching readiness score: 98.4% matched across main labels, care labels, hangtags, and polybags.
| Trim Item Code | Description | Associated Order | Required Qty | Matched In Store | Match Rate | Readiness |
|---|---|---|---|---|---|---|
TRM-LBL-MAIN-88 |
Damask Woven Main Brand Label | LTX-POLO-88C | 8,500 Pcs | 8,500 Pcs | 100.0% | Matched |
TRM-LBL-CARE-04 |
Satin Printed Care & Size Label | LTX-TEE-04 | 7,000 Pcs | 7,000 Pcs | 100.0% | Matched |
TRM-DRW-HOOD-05 |
Round Braided Cotton Drawcord (120cm) | LTX-HOOD-05 | 6,750 Pcs | 6,500 Pcs | 96.3% | Replenishing |
06 Accessories Status
Sewing and finishing accessories inventory: 96.2% verified across zippers, buttons, rivets, and drawcords.
07 Material Availability
Consolidated floor material availability index: 99.1% stocked across all raw material classifications.
08 Material Shortage
Active material deficit tracking: 1 non-critical shortage logged (Sewing Thread spool #T-882 pending delivery).
| Material Code | Material Description | Affected Line | Deficit Quantity | Buffer Run-out | Current Status | Priority Level |
|---|---|---|---|---|---|---|
TH-SP-882-GRN |
Spun Polyester Sewing Thread 40/2 (Forest Green #882) | Line 11 | 12 Spools | 1.5 Hours | In Transit (ETA 42 min) | Medium Priority |
09 Shortage Priority
Deficit prioritization ledger: High/Medium/Low criticality rankings based on sewing line buffer run-out hours.
10 Reserve Stock
Strategic safety inventory reserve maintaining 14 days safety stock on bulk sewing threads and core notions.
11 Available Stock
Ready-to-issue inventory verified in racking bays A1-D12 cleared by Raw Material Quality Inspection.
12 Material Balance
Warehouse stock ledger balancing received goods, floor issues, returns, and physical balance reconciliations.
13 Line Feeding
Real-time feeding coverage across sewing and finishing units: 11 of 12 production lines actively fed with zero starvation.
| Line # | Style Fed | Fabric Status | Trims Status | Thread Stock | Buffer Run-out | Line Feeding State |
|---|---|---|---|---|---|---|
| Line 01 | LTX-POLO-01 | 100% Available | 100% Matched | 14 Days Safety | 48 Hours | Normal Feeding |
| Line 02 | LTX-POLO-02 | 100% Available | 100% Matched | 14 Days Safety | 48 Hours | Normal Feeding |
| Line 04 | LTX-TEE-04 | 100% Available | 100% Matched | 14 Days Safety | 36 Hours | Normal Feeding |
| Line 08 | LTX-POLO-88C | 100% Available | 100% Matched | 14 Days Safety | 32 Hours | Normal Feeding |
| Line 11 | LTX-JACK-11 | 100% Available | 96.3% Matched | 1.5h In-line Buffer | 1.5 Hours | Replenishing (ETA 42m) |
| Line 12 | LTX-JACK-12 | 100% Available | 100% Matched | 14 Days Safety | 28 Hours | Normal Feeding |
14 Feeding Schedule
Scheduled hourly material transit dispatches coordinating automated guided vehicles (AGVs) and manual carts.
15 Feeding Status
Status of feeding buffers per sewing line: Average 1.8 shifts buffer established ahead of line consumption.
16 Pending Material
Pending material requisitions staged in the dispatch staging area awaiting floor supervisor clearance.
17 Material Requirement
Bill of Materials (BOM) gross requirements calculated from active manufacturing orders across all styles.
18 Material Issue
Historical issuance log recording material issue notes (MINs), recipient line IDs, and issuing storekeeper sign-offs.
19 Material Consumption
Floor consumption tracking against standard BOM allowances with real-time waste and variance indicators.
20 Order-wise Materials
Material traceability matrix linked to Purchase Orders (PO-2026-8812, PO-2026-8815, PO-2026-8820).
21 Style-wise Materials
Style-level material allocation breakdown for LTX-POLO-88C, LTX-TEE-04, and LTX-HOOD-05.
22 Critical Shortage
Zero critical floor shutdown gaps: 0 critical material shortages threatening live production pacing.
23 Material Alerts
Active warehouse alerts: Thread #T-882 in transit (ETA 42 mins) & Line 11 trims buffer warning.
| Alert Code | Severity | Condition Description | Affected Area | Action Taken | Timestamp |
|---|---|---|---|---|---|
ALT-STR-01 |
Warning | Thread spool #T-882 pending delivery • Line 11 buffer at 1.5h | Line 11 Buffer Rack | Supplier courier tracked; ETA 42 minutes to Central Receiving | 17 Sep 2026 04:12 BST |
ALT-STR-02 |
Normal | Lot #FL-9023 French Terry trims delivery in transit; buffer at 1.8 shifts | Warehouse Receiving Dock 2 | Gate pass issued; offloading bay pre-assigned | 17 Sep 2026 04:30 BST |
24 Store & Materials Summary
Executive store health sign-off, inventory turnover metrics, and Central Store Dispatch contact ledger.
COMPLIANCE & HOUSEKEEPING INTELLIGENCE SYSTEM
Factory Social Compliance • 5S Housekeeping • Fire & Electrical Safety • CAP Management • Environmental Standards
Compliance & Housekeeping Overview
Factory-wide compliance score, housekeeping rating, safety posture, and CAP statusFactory-wide Status
Integrated plant summary across all operational zones and compliance criteria| FACILITY UNIT / ZONE | HEAD OF COMPLIANCE / POC | 5S RATING | FIRE / LIFE SAFETY | CHEMICAL MGMT | PPE ADHERENCE | ACTIVE FINDINGS | STATUS |
|---|---|---|---|---|---|---|---|
| Unit 01 โ Sewing & Assembly (Floors 2-3) | Engr. M. Haque | 96.8% | 100% PASS | N/A (Dry Line) | 99.4% | 1 Minor | COMPLIANT |
| Unit 02 โ Cutting & Spreading (Floor 1) | T. Ahmed | 95.4% | 100% PASS | Lubricants Inspected | 98.8% | 1 Minor | COMPLIANT |
| Unit 03 โ Finishing & Packing (Floor 4) | S. K. Paul | 97.2% | 100% PASS | Spot Lifter SDS Verif. | 99.6% | 0 Items | COMPLIANT |
| Unit 04 โ Fabric & Trims Warehouse | M. R. Karim | 94.8% | 100% PASS | Secondary Containment OK | 98.5% | 2 Minor | COMPLIANT |
| Central Utility & Substation | Engr. N. Islam | 98.1% | 100% PASS | Transformer Bunding OK | 100.0% | 0 Items | COMPLIANT |
Area-wise Status
Departmental breakdown of social standards, working conditions, and safety provisionsProduction & Sewing Halls
Ergonomic seating checks completed across all 24 production lines. Illumination tests confirm 620-750 Lux across sewing needles (exceeds 500 Lux standard). Ventilation rates verified at 8.2 air changes per hour with cross-breeze evaporative coolers operating within temperature range 24.5°C - 26.2°C.
Warehouse & Material Logistics
Roll fabric racks inspected for stacking limits (max 4 tiers compliant). Heavy-duty forklift lanes strictly demarcated with yellow zebra borders. Pallet loading safety margins verified with zero overhanging pallets in main transit corridors.
Section-wise Status
Granular evaluation of prep, spreading, cutting, sewing, washing, finishing, and QA zonesLine-wise Status
Micro-level audit records for Sewing Lines 01 through 24| LINE ID | LINE SUPERVISOR | FLOOR AUDITOR | 5S SCORE | SAFETY GUARDS | WASTE DISPOSAL | AISLE CLEARANCE | ACTION REQ. |
|---|---|---|---|---|---|---|---|
| Line 01 | K. Alam | R. Sultana | 98.5% | 100% OK | Color Bins Segregated | Clear (>1.6m) | None |
| Line 04 | J. Uddin | R. Sultana | 97.0% | 100% OK | Color Bins Segregated | Clear (>1.5m) | None |
| Line 07 | M. Rahman | S. Akhtar | 95.5% | 1 Eye Shield Adjusted | Minor thread waste on tray | Clear (>1.5m) | Tidied up |
| Line 12 | S. Islam | S. Akhtar | 98.0% | 100% OK | Color Bins Segregated | Clear (>1.5m) | None |
| Line 18 | A. Hossain | F. Begum | 96.5% | 100% OK | Color Bins Segregated | Clear (>1.5m) | None |
| Line 24 | H. Kabir | F. Begum | 97.5% | 100% OK | Color Bins Segregated | Clear (>1.5m) | None |
Housekeeping Status
Cleanliness standards, dust extraction, and floor sanitation monitoringFloor & Gangway Sanitation
Scrubber-drier scheduled cleaning executed at 06:00, 12:30, and 18:30 daily. Epoxy floor coating intact with zero oil patches or moisture hazards detected.
GRADE: EXCELLENT (98.2%)Lint & Dust Extraction
Central vacuum air filtration operational across spreading tables and overlock clusters. Ambient airborne particulate matter PM2.5 measured at 24 μg/m³ (well below WHO threshold).
GRADE: EXCELLENT (96.0%)Waste Stream Segregation
Color-coded waste bins (Fabric Scraps - Blue, General Trash - Green, Recyclable Plastic - Yellow, Oily Rags - Red Metal Bins) 100% compliant with lids secured.
GRADE: 100% CONFORMANTCompliance Status
Statutory compliance, labor law enforcement, and buyer code-of-conduct posture| STANDARDS FRAMEWORK | ACCREDITATION / AUDIT BODY | CURRENT SCORE / RATING | VALIDITY PERIOD | LAST AUDIT DATE | NEXT SURVEILLANCE | AUDIT VERDICT |
|---|---|---|---|---|---|---|
| BSCI Code of Conduct | amfori BSCI / SGS Bangladesh | Rating A (Excellent) | 24 Months | 14-Jan-2026 | 14-Jan-2028 | FULL COMPLIANCE |
| SMETA 4-Pillar Ethical Trade | Sedex / Intertek Bangladesh | 0 Critical Findings | 12 Months | 05-Nov-2025 | 05-Nov-2026 | CERTIFIED |
| Higg Facility Environmental Module | Sustainable Apparel Coalition | 94.2% FEM Score | Annual Cycle | 28-Feb-2026 | Feb-2027 | VERIFIED LEADER |
| RSC / Accord Fire & Building Safety | RMG Sustainability Council | 100% Remediation | Continuous Monitoring | 18-Dec-2025 | Quarterly Inspection | GREEN LISTED |
| OEKO-TEX Standard 100 Class I | Testex Zurich | Annex 4 Tested Pass | Annual Renewal | 12-Aug-2025 | 12-Aug-2026 | VALID |
Audit Checklist
Daily, weekly, and monthly verification protocol checklistInspection Status
Status of daily internal floor patrols, buyer spot inspections, and third-party evaluationsInternal EHS Floor Patrol Log
- Round 01 (Morning Shift Start โ 08:00): All exit paths clear, attendance facial scanners sanitised, floor walkways clean.
- Round 02 (Mid-Day Break โ 13:00): Dining hall hygiene audit completed; potable water UV filtration tests verified negative for coliforms.
- Round 03 (Afternoon Production โ 16:30): Spot check on iron boiler steam trap temperatures; ventilation extractors functioning normally.
Buyer Technical & Ethical Inspections
- H&M Sustainability Audit: Passed with zero CAP requirement on 12-Feb-2026. Next cycle Scheduled Q3.
- Inditex Social Audit: Grade A maintained; environmental discharge water tested through ZDHC gateway (100% MRSL compliant).
- Target Global Compliance: Completed annual security & C-TPAT supply chain verification.
Observation Summary
Aggregated findings from daily observations categorized by risk levelNon-compliance
Detailed breakdown of active non-compliant observations requiring mitigation| NC REF ID | SEVERITY | ZONE / LOCATION | DEFICIENCY DESCRIPTION | STANDARD REFERENCE | ASSIGNED OWNER | TARGET RESOLUTION | CURRENT STATUS |
|---|---|---|---|---|---|---|---|
| NC-2026-041 | WARNING | Floor 1 โ Sample Room Table 3 | Flexible iron cable outer sleeve showing micro-abrasion near base | NFPA 70 / Electrical Safety Sec. 4 | Elec. Engr. M. Kabir | Today 16:00 | IN PROGRESS (70%) |
| NC-2026-042 | MINOR | Floor 2 โ Line 07 End Table | Trimmings bin label peeling off corner; minor thread spillage | 5S Seiton Standard Visual Label | Supervisor M. Rahman | Today 18:00 | REPLACING LABEL |
| NC-2026-043 | MINOR | Warehouse โ Bay D4 | Roll fabric pallet placed 10cm past designated border marking | Internal Logistics SOP-08 | Asst. Store Mgr. B. Roy | Today 14:30 | CORRECTED |
| NC-2026-044 | MINOR | Floor 4 โ Finishing Carton Zone | Empty carton stack exceeded 1.8m height guideline by 15cm | OHSAS Warehouse Safety Guideline | Finishing Lead S. K. Paul | Today 15:00 | RESTACKED |
Compliance Score
Multidimensional scoring index measuring regulatory and social performanceSocial & Labor Standards
Working hours, overtime calculation, minimum wage disbursements, maternity benefits, and freedom of association committee documentation 100% compliant.
Occupational Health & Safety
Emergency lighting illumination lux levels, smoke detector sensitivity testing, sprinkler valve tamper monitoring, and machinery ergonomics fully validated.
Environmental Stewardship
Zero discharge of hazardous chemicals (ZDHC Level 3 conformity), rainwater harvesting facility operational, energy efficiency LED conversion at 100%.
Housekeeping Score
Standardized index for physical order, clean aisles, and tool shadowboardsCleanliness Status
Sanitary facilities, canteen hygiene, and production atmosphere metricsWorker Washrooms & Restrooms
Ratio: 1 toilet per 18 female workers, 1 per 22 male workers (exceeds statutory 1:25 ratio). Automated liquid soap dispensers, continuous running water, and hourly cleaning log verified.
STATUS: 100% SATISFACTORYCanteen & Meal Hall Hygiene
Stainless steel dining tables sanitized between meal batches. Food handlers certified with regular enteric health screenings. Food temperature hot-holding >65°C compliant.
STATUS: 100% SATISFACTORYCreche & Medical Centre
Licensed medical doctor and 3 certified nurses on duty. Infant feeding zone sanitized and isolated from industrial noise (<55 dB ambient acoustic rating).
STATUS: 100% SATISFACTORYSafety Condition
Fire protection systems, structural integrity, and life safety readinessFire Hydrant & Sprinkler Network
Jockey pump maintain continuous 7.2 Bar pressure in fire ring main. Diesel backup fire pump weekly automatic run-test successfully verified on Monday 07:00. Dedicated fire water reservoir at 100% capacity (450,000 Liters, sufficient for 4 hours continuous hydrant discharge).
Evacuation & Alarm Systems
Addressable fire alarm panel linked to 340 optical smoke sensors and manual call points. All illuminated exit directional sign batteries hold >90 minutes emergency charge. Last unannounced factory fire drill executed in 3 minutes 14 seconds (all 1,840 occupants safely assembled at designated assembly grounds).
Workplace Condition
Indoor environmental quality: temperature, humidity, noise, and lighting| ENVIRONMENTAL PARAMETER | STANDARD REQUIREMENT | ACTUAL MEASURED VALUE | SENSOR NETWORK STATUS | COMPLIANCE STATUS |
|---|---|---|---|---|
| Ambient Floor Temperature | ≤ 28.0 °C | 25.4 °C | 16 IoT Temperature Probes | OPTIMAL |
| Relative Humidity (RH) | 50% – 70% | 58.2% | Calibrated Digital Hygrometers | OPTIMAL |
| Sewing Needle Illumination | ≥ 500 Lux | 680 Lux Average | Photometric Light Meters | EXCEEDS STANDARD |
| Acoustic Noise Level | ≤ 85 dB (8-hour TWA) | 74.5 dB (A) | Continuous Noise Dosimeters | SAFE |
| Carbon Dioxide (CO2) Level | ≤ 1000 ppm | 620 ppm | NDIR CO2 Sensors | FRESH AIR VENTILATED |
5S Status
Execution status across the five Japanese workplace organization pillarsUnneeded materials red-tagged and removed. Zero clutter around machine pedals.
Shadowboards for mechanic tools, scissor holders, and bobbin trays strictly demarcated.
Machines wiped down at end of each shift. Oil collection pans clean and leak-free.
Color-coded floor zoning and standard visual operating SOP cards posted at all lines.
Daily 5S audits by floor committee; monthly inter-line 5S trophy competition active.
Pending Issues
Tracked open items awaiting physical replacement or verification closure- Issue #01: Replacement of thermal insulation jacket on Steam Header Valve #3 (Floor 4). Material requisitioned; installation scheduled for tonight during maintenance shutdown.
- Issue #02: Renewing laminated bilingual safety notices at secondary exit staircase south landing. Print shop delivering at 15:00.
- Issue #03: Spot-welding minor defect on scrap fabric cart wheel bearing. Maintenance workshop currently repairing.
Corrective Action
CAP root cause analysis and systemic engineering countermeasuresRoot Cause Analysis (5-Why Framework)
Defect: Frayed iron flex cord outer sheath in sample room.
Why 1: Cord rubs against table edge bracket.
Why 2: Cable swivel arm position was improperly tensioned.
Why 3: Operator repositioned ironing board without readjusting overhead cable support spring.
Root Solution: Installed heavy-duty flexible silicone cable sleeve plus mandatory swivel arm position lock.
Systemic Countermeasures Applied
Audited all 32 ironing tables factory-wide to ensure every iron cord has spring-balanced overhead suspension and rubber grommet protection at table passages. Preventive maintenance checklist updated to include mandatory insulation resistance testing for all irons every Monday.
Action Status
Live tracking of active Corrective Action Plans (CAP)| ACTION ID | ACTION ITEM | TARGET COMPLETION | PROGRESS | VERIFYING AUDITOR | STATUS |
|---|---|---|---|---|---|
| CAP-26-088 | Upgrade sample room iron suspension arm | Today 16:00 |
|
Engr. M. Kabir | IN PROGRESS |
| CAP-26-089 | Relabel 5S scrap bins on Line 07 | Today 18:00 |
|
Auditor R. Sultana | FINAL CHECK |
| CAP-26-090 | Re-align fabric pallet in Warehouse Bay D4 | Today 14:30 |
|
Asst. Mgr. B. Roy | COMPLETED |
Responsible Person
Designated department heads and compliance section officers| RESPONSIBLE LEAD | DESIGNATION / DEPARTMENT | DIRECT EXTENSION | CURRENT ASSIGNED ACTIONS | HISTORICAL CLOSURE RATE |
|---|---|---|---|---|
| Engr. Mozammel Haque | Head of Social Compliance & EHS | Ext. 401 | Overall Factory Oversight | 99.8% On-Time |
| Engr. Masum Kabir | Chief Electrical & Safety Engineer | Ext. 415 | 1 Action (Sample Iron) | 99.2% On-Time |
| Ms. Razia Sultana | Senior 5S Quality Auditor | Ext. 422 | 1 Action (Line 07 Bins) | 100.0% On-Time |
| Mr. B. Roy | Warehouse Safety Supervisor | Ext. 310 | 0 Actions (1 Closed) | 98.5% On-Time |
Due Date
Timeline deadlines, countdown milestones, and overdue alertsImmediate Term (< 24 Hours)
3 items targeted for closure before end of current working day (18:00 BST). Zero overdue tasks.
ALL ON SCHEDULEShort Term (≤ 7 Days)
Quarterly third-party air emissions stack testing for industrial boilers scheduled for 22-Mar-2026.
PREPAREDMedium Term (≤ 30 Days)
Annual refresher training for all 92 certified fire marshals and 45 first aiders with Fire Service and Civil Defence (FSCD).
ROSTER READYCritical Findings
Zero-tolerance compliance items and immediate shutdown risk monitoringZERO CRITICAL FINDINGS ACTIVE
There are currently 0 Critical Non-Conformances across all four production units, central warehouse, and boiler house. No locked emergency doors, no blocked fire equipment, no child or forced labor risks, and no unauthorized subcontracting detected. All statutory safety operating permits (Factory License, Fire License, Environmental Clearance Certificate, Boiler Certificates) are active and in full legal validity.
Warning Findings
Moderate risk items requiring prompt preventive correction before escalationLocation: Sample Room Ironing Board #3.
Observation: Outer woven textile sheath on iron electric flex cord showed minor friction wear.
Action Taken: Cord isolated and currently being swapped for certified heavy-duty heat-resistant silicone cable by Maintenance Team. Completion expected within 90 minutes.
Area Comparison
Comparative benchmarking across plant floors and operational divisions| OPERATING DEPARTMENT | OVERALL COMPLIANCE | 5S HOUSEKEEPING | FIRE / LIFE SAFETY | AIR QUALITY & LUX | OPERATOR PARTICIPATION | BENCHMARK RANK |
|---|---|---|---|---|---|---|
| Finishing & Packing (Floor 4) | 99.1% | 98.0% | 100% | Optimal (710 Lux) | 99.5% | RANK 1 (STAR) |
| Sewing Unit 1 (Floor 2) | 98.5% | 97.4% | 100% | Optimal (680 Lux) | 99.2% | RANK 2 |
| Cutting Section (Floor 1) | 97.8% | 96.8% | 100% | Optimal (695 Lux) | 98.8% | RANK 3 |
| Sewing Unit 2 (Floor 3) | 97.4% | 96.2% | 100% | Optimal (660 Lux) | 98.5% | RANK 4 |
| Fabric & Trims Warehouse | 96.8% | 94.8% | 100% | Optimal (540 Lux) | 98.0% | RANK 5 |
Daily Status
Chronological summary of today's compliance patrol and environmental readingsWeekly Trend
7-day rolling performance comparison across primary compliance indicators7-Day 5S Housekeeping Trend
Consistent performance maintained above the 95.0% threshold: Sat (96.1%) • Sun (96.4%) • Mon (96.8%) • Tue (96.3%) • Wed (96.5%) • Thu (96.7%) • Today (96.5%).
7-Day Incident & Near-Miss Log
Zero lost-time injuries (LTI) recorded for the consecutive 482nd day. Two minor near-misses reported and resolved via preventive engineering intervention without injury.
482 CONSECUTIVE LTI-FREE DAYSMonthly Trend
Monthly historical progression of social compliance, safety, and CAP cycle times| MONTH | OVERALL COMPLIANCE | HOUSEKEEPING INDEX | TOTAL AUDITS | CAPS RAISED | CAPS RESOLVED ≤24H | AVG CLOSURE TIME |
|---|---|---|---|---|---|---|
| March 2026 (MTD) | 98.4% | 96.5% | 42 Audits | 14 Items | 14 Items (100%) | 3.4 Hours |
| February 2026 | 98.1% | 96.2% | 78 Audits | 28 Items | 27 Items (96.4%) | 4.1 Hours |
| January 2026 | 97.9% | 95.8% | 84 Audits | 32 Items | 31 Items (96.8%) | 4.8 Hours |
Factory Summary
Executive compliance posture, buyer audit readiness, and certification statusStatutory & Buyer Audit Posture
The facility stands in full certified compliance with Bangladesh Labour Act 2006 (amended 2018), National Building Code, RSC Life Safety standards, amfori BSCI, and SMETA 4-Pillar ethical mandates. All fire escape corridors, life-safety alarms, illuminated directional signs, and ventilation systems operate at 100% functional readiness.
Continuous 5S Culture
Visual workplace standards are institutionalized across all 24 sewing lines, cutting halls, and warehouses. Floor demarcations, tool shadowboards, waste segregation, and daily audit patrols ensure immediate identification and rapid correction of housekeeping variances.
FACTORY PRODUCTION INTELLIGENCE CONSOLE
Consolidated Plant Output • Plan vs Actual • Process Telemetry • Line Pace • WIP • Order Traceability
Production Overview
Consolidated plant production overview across cutting, sewing, finishing, inspection, packing, and shipmentFactory Production Status
Real-time status breakdown across manufacturing divisions and major production facilities| PRODUCTION UNIT / DIVISION | FLOOR LOCATION | TARGET (PCS) | ACTUAL (PCS) | ACHIEVEMENT | VARIANCE | RUNNING STYLES | OPERATIONAL STATUS |
|---|---|---|---|---|---|---|---|
| Unit 01 — Sewing Module Hall A | Floor 2 (Lines 01-12) | 9,200 | 8,740 | 95.0% | -460 | 4 Styles (Knit Polo, T-Shirt) | RUNNING ON SCHEDULE |
| Unit 02 — Sewing Module Hall B | Floor 3 (Lines 13-24) | 9,200 | 8,550 | 92.9% | -650 | 3 Styles (French Terry Hoodie) | RUNNING ON SCHEDULE |
| Unit 03 — Cutting Section | Floor 1 | 22,250 | 19,450 | 87.4% | -2,800 | 7 Cut Orders Staged | FEEDING SEWING |
| Unit 04 — Finishing & Packing | Floor 4 | 18,000 | 16,920 | 94.0% | -1,080 | 5 POs in Carton Packing | INSPECTION CLEAR |
Production Plan
Master production schedule (MPS) targets, allocated line hours, and planned standard allowed minutes (SAM)Planned Daily Capacity
Scheduled for 18,400 standard garment units across 24 modular sewing lines operating on an 8.0-hour primary shift with 1.5 hours authorized overtime window.
Standard Allowed Minutes (SAM)
Weighted average style SAM across active buyer purchase orders: 14.8 minutes per basic t-shirt and 22.4 minutes per raglan fleece hoodie.
Line Balancing Planned Target
Calculated line efficiency target set at 85.0% with planned pitch time of 42.5 seconds per garment work station.
Plan vs Actual
Comparative analysis of planned milestones against real-time physical production outputTarget Achievement
Percentage of target achieved across lines, shifts, and individual work cellsOverall Plant Achievement
17,290 units completed out of 18,400 daily planned target. 18 of 24 lines operating ≥92% achievement.
Top Performing Line (Line 04)
Produced 1,808 units against 1,700 target rate. Operating speed 226 Pcs/Hr on single jersey crewneck.
Line Requiring Attention (Line 07)
Produced 1,392 units against 1,450 target. Minor collar rib feeding bottleneck currently resolved.
Hourly Production
Hour-by-hour output distribution, cadence curves, and hourly target achievement| PRODUCTION HOUR | TIME WINDOW | TARGET (PCS) | ACTUAL (PCS) | HOURLY VARIANCE | HOURLY PACE | CUMULATIVE OUTPUT |
|---|---|---|---|---|---|---|
| Hour 01 | 08:00 – 09:00 | 2,100 | 1,840 | -260 | 87.6% (Warm-up) | 1,840 Pcs |
| Hour 02 | 09:00 – 10:00 | 2,300 | 2,180 | -120 | 94.8% | 4,020 Pcs |
| Hour 03 | 10:00 – 11:00 | 2,300 | 2,290 | -10 | 99.6% | 6,310 Pcs |
| Hour 04 | 11:00 – 12:00 | 2,300 | 2,310 | +10 | 100.4% | 8,620 Pcs |
| Hour 05 (Post-Lunch) | 13:00 – 14:00 | 2,300 | 2,140 | -160 | 93.0% | 10,760 Pcs |
| Hour 06 | 14:00 – 15:00 | 2,300 | 2,260 | -40 | 98.3% | 13,020 Pcs |
| Hour 07 | 15:00 – 16:00 | 2,300 | 2,210 | -90 | 96.1% | 15,230 Pcs |
| Hour 08 (Current) | 16:00 – 17:00 | 2,500 | 2,060 | -440 | In Progress | 17,290 Pcs |
Shift Achievement
Aggregated performance indicators for Shift A and Shift BShift A (Morning • 08:00 – 16:30)
Shift output: 14,850 Pcs against 15,600 target (95.2% achievement). 24 lines staffed with 1,240 sewing machinists. Average line efficiency 79.1%.
Shift B (Evening / Overtime • 16:30 – 19:30)
Current evening output: 2,440 Pcs against 2,800 planned overtime target (87.1% progress). 12 critical path lines retained for priority export POs.
Shift Progress
Elapsed time vs production progress bar across operating shiftsFactory-wide Output
Gross factory output across the six verified manufacturing lifecycle stagesCutting Output
Fabric cut pieces released from auto-cutter and manual spreading tables19,450 garments cut today across Tables 01 to 06. Marker utilization averaged 86.4%. Spreading readiness 98.2% with 2,800 pieces staged in cutting queue ready for bundler sorting.
| TABLE ID | FABRIC TYPE | LAY LENGTH | PLANNED PLIES | ACTUAL CUT (PCS) | STATUS |
|---|---|---|---|---|---|
| Table 01 | Single Jersey 180 GSM | 42.5m | 80 Plies | 3,400 | COMPLETED |
| Table 02 | 100% Cotton Pique 220 GSM | 38.0m | 75 Plies | 3,250 | COMPLETED |
| Table 03 | French Terry 280 GSM | 36.0m | 60 Plies | 2,800 | COMPLETED |
Sewing Output
Assembly line output from Sewing Units 01 & 02 (Lines 01 to 24)17,290 assembled garments produced across 24 lines. Zero line stoppage incidents recorded. Shift target pacing running at 94.0% against 18,400 daily target.
Finishing Output
Thread sucking, stain removal, steam tunnel, and vacuum ironing output16,920 finished units pressed and treated. 32 industrial steam iron tables operating at continuous 4.5 Bar steam pressure with zero moisture staining detected.
Inspection Output
100% visual end-line inspection, needle detection, and AQL audit output16,780 garments cleared through 100% end-line inspection. 310 minor defects identified and reworked immediately on floor touch-up tables. Needle detector 9-point test passed at 1.0mm ferrous calibration.
Packing Output
Folding, hangtag attaching, individual polybagging, and master carton packing16,580 garments sealed into retail polybags and packed into 414 export master cartons. Barcode validation scan verified 100% label and size accuracy.
Shipment Output
Final audit clearance, container loading, and commercial invoice dispatches14,200 finished garments palletized in finished goods staging bay. 1x 40ft High-Cube container loaded for H&M Order #PO-88219 (Vessel ETD: Friday 20-Mar-2026).
Production Flow
Synchronized material velocity and handover pipeline across production stationsWIP Across Processes
Work-in-process inventory volume and buffer health at inter-process buffers| INTER-PROCESS BUFFER | CURRENT WIP (PCS) | BUFFER TARGET | BUFFER COVERAGE | BOTTLENECK RISK | STATUS |
|---|---|---|---|---|---|
| Cut Bundles to Sewing Input | 6,420 Pcs | 6,000 Pcs | 1.8 Shifts | LOW | BALANCED |
| Sewing Output to Finishing Line | 4,850 Pcs | 4,500 Pcs | 2.1 Shifts | LOW | HEALTHY |
| Finishing to Quality Inspection | 1,240 Pcs | 1,500 Pcs | 0.9 Shifts | LOW | FLOWING |
| Inspection to Final Packing | 860 Pcs | 1,000 Pcs | 0.4 Shifts | LOW | LEAN |
Line Output
Disaggregated output for primary sewing lines with hourly run rates| LINE ID | TARGET | ACTUAL | RUN RATE | OPERATORS | DHU | PERFORMANCE |
|---|---|---|---|---|---|---|
| Line 01 | 1,500 Pcs | 1,532 Pcs | 192 Pcs/Hr | 48 | 1.2% | 102.1% |
| Line 02 | 1,600 Pcs | 1,574 Pcs | 198 Pcs/Hr | 52 | 1.6% | 98.4% |
| Line 03 | 1,450 Pcs | 1,392 Pcs | 174 Pcs/Hr | 46 | 2.1% | 96.0% |
| Line 04 | 1,700 Pcs | 1,808 Pcs | 226 Pcs/Hr | 54 | 0.9% | 106.3% |
Capacity Utilization
Installed machine capacity vs active production loading across unitsSewing Capacity Utilization
980 active sewing machines of 1,040 installed machines deployed on live floor production lines.
Cutting Capacity Utilization
2 automatic NC cutters and 4 manual spreading tables operating at 87.4% scheduled load.
Finishing Capacity Utilization
Steam boiler load at 78% capacity supporting 32 vacuum press stations with 94.0% throughput.
Production Variance
Variance calculations comparing output deficit against standard production parametersCumulative daily variance stands at -1,110 Pcs (-6.0% against daily plan). 48% of variance occurred during Hour 01 warm-up and Hour 05 post-lunch ramp-up. Mitigated by authorized 1.5-hour overtime scheduled on 12 key lines.
Production Pace
Standard garments per minute run-rate and real-time takt time trackingPending Production
Unfulfilled order quantities remaining to complete current manufacturing PO contractsTotal pending balance across active export contracts: 48,200 Pcs scheduled for completion within the next 4 operational working days. Cutting WIP buffer guarantees continuous feed.
Order-wise Production
Disaggregated production progress by buyer purchase order number| PURCHASE ORDER | BUYER NAME | ORDER QTY | PRODUCED TO DATE | TODAY OUTPUT | BALANCE PENDING | EX-FACTORY DATE |
|---|---|---|---|---|---|---|
| PO-88219 | H&M Sweden | 25,000 Pcs | 21,400 Pcs | 4,200 Pcs | 3,600 Pcs | 24-Mar-2026 |
| PO-88220 | Zara / Inditex | 18,000 Pcs | 14,500 Pcs | 3,850 Pcs | 3,500 Pcs | 28-Mar-2026 |
| PO-88221 | Target USA | 32,000 Pcs | 24,800 Pcs | 5,420 Pcs | 7,200 Pcs | 02-Apr-2026 |
Style-wise Production
Production volume tracked by garment style code and fabric category| STYLE CODE | GARMENT DESCRIPTION | FABRIC COMPOSITION | SAM | TODAY OUTPUT | STYLE EFFICIENCY |
|---|---|---|---|---|---|
| ST-9912 | Men's Crewneck T-Shirt | 100% Combed Cotton 180 GSM | 14.8 Min | 6,840 Pcs | 82.4% |
| ST-9914 | Women's V-Neck Slim Tee | 95% Cotton 5% Spandex 190 GSM | 16.2 Min | 5,120 Pcs | 79.1% |
| ST-9920 | Pullover Hooded Sweatshirt | 80% Cotton 20% Poly Fleece 280 GSM | 22.4 Min | 5,330 Pcs | 74.5% |
Shift-wise Production
Detailed breakdown comparing Shift A vs Shift B contributionsShift A contributed 85.9% of total production volume (14,850 Pcs across 8 operating hours). Shift B overtime running with 2,440 Pcs completed to meet urgent PO-88219 export deadline.
Production Trend
7-day rolling performance curve of daily output and efficiency ratesConsistent performance maintained above the 16,500 Pcs daily threshold: Sat (16,840) • Sun (17,120) • Mon (17,450) • Tue (17,210) • Wed (17,380) • Thu (17,520) • Today (17,290).
Critical Alerts
Real-time bottleneck notifications, starvation risks, and machine alertsZERO CRITICAL PRODUCTION STOPPAGES
No lines starved for fabric or trims. Cutting buffer stands at 1.8 shifts ahead of sewing consumption. Sewing machine breakdown rate 0.42% (well within 2.0% SLA threshold). All 24 lines actively producing.
Production Summary
Executive operational synthesis, cumulative daily results, and dispatch readinessDaily Manufacturing Performance
Factory operations achieved 17,290 Pcs finished garments across 24 production lines (94.0% target achievement). Process integration verified across cutting (19,450 Pcs), finishing (16,920 Pcs), and inspection (16,780 Pcs).
Export Readiness & Shipment
16,580 garments securely packed in master cartons. Export shipment of 14,200 units cleared for container loading and customs transit dispatch with zero open non-conformances.
๐ฌ QMS Report Level-2 Enterprise Quality Console
Enterprise Total Quality Management • 14 Consolidated Modules • 66 Standard Quality Verification Parameters
QMS Overview
Item 01Enterprise total quality management overview integrating 24 sewing lines, fabric inspection, cutting precision, finishing steam treatment, and final packaging conformity.
Quality KPI Dashboard
Item 02Consolidated scorecard benchmarking quality metrics across production lines, fabric inspection rolls, trims verification, and packaging boxes.
Quality Status
Item 03Current plant-wide quality operational condition: GREEN • AQL CONFORMANT. Zero critical stop-shipment defects recorded across active shifts.
Inline Quality Inspection
Item 04Roving QC checkpoints verifying needle stitch tension, seam alignment, and SPI (Stitches Per Inch) conformity at operational sewing stations.
End-line Quality Inspection
Item 05100% visual and dimensional verification at the end of each sewing line prior to hand-over to the finishing floor.
Final Inspection
Item 06Pre-shipment internal quality audit verifying packed export cartons against buyer tech-packs, folding guidelines, and packaging specifications.
AQL Inspection
Item 07Statistical sampling per ISO 2859-1 (Level II Normal Sampling): AQL 1.5 for Major defects (Max Allowed: 7, Actual: 1), AQL 4.0 for Minor defects (Max Allowed: 14, Actual: 4).
Inspection Checklist
Item 08Standardized 32-point inspection checklist verifying fabric symmetry, shade matching, labeling accuracy, button pull strength (โฅ 90 N for 10 sec), and needle safety.
Inspection Finding
Item 09Granular log of verified anomalies during shift inspections: 1x skipped stitch on bottom hem, 2x minor loose thread ends, 1x slight collar asymmetry.
Quality Hold Report
Item 10Quarantine holding area report: 0 production lots currently under critical quality hold. 1 sample bundle held for shade verification.
Quality Release Status
Item 11Formal quality assurance sign-off releasing completed purchase orders for container loading and warehouse export transfer.
Defect Report
Item 12Aggregated defect count across all inspection gates: 318 defect instances recorded out of 17,290 garments inspected (1.84% DHU).
Defect Category Analysis
Item 13Categorization: Workmanship/Stitching (68.2%), Measurement/Tolerance (14.5%), Fabric Material (11.3%), Trims & Notions (6.0%).
DHU / Defect Rate
Item 14Defects per Hundred Units: (318 Defects รท 17,290 Units Inspected) ร 100 = 1.84% DHU.
First Pass Yield (FPY)
Item 15Units passed on first inspection without requiring touch-up or alteration: 16,972 of 17,290 units = 98.16% FPY.
Critical Defect Report
Item 16Critical defects (sharp points, broken needles, hazardous chemicals, incorrect care label): 0 Critical Defects Active.
Major Defect Report
Item 17Defects affecting garment saleability or fit: 28 major defects logged plant-wide (0.16% occurrence rate).
Minor Defect Report
Item 18Superficial cosmetic imperfections: 290 minor loose thread and removable chalk mark issues cleared by trimmer assistants.
Defect Pareto Analysis
Item 19Top 3 defect types account for 78.4% of all rework: 1. Skipped Stitches (38.2%), 2. Seam Puckering (24.1%), 3. Uneven Placket (16.1%).
Rework Report
Item 20Rework tracking system: 318 garments routed for floor re-stitching; 310 units repaired and returned to regular packaging.
Reject Report
Item 21Irreparable cut/sewing damage: 8 units rejected (0.046% scrap rate โ well below 0.5% contractual buyer allowance).
Alter / Repair Report
Item 22Touch-up station operations: 8 certified rework specialists operating specialized single-needle and feed-off-arm repair machines.
Broken Needle Report
Item 23Broken needle protocol: 2 broken needles recorded today; 100% of broken pieces retrieved, matched, and taped to log sheet prior to reissue.
Sharp Tools Report
Item 24Inventory of trimmers, scissors, tag guns; all 148 floor clippers secured with metal chain lanyards directly anchored to tables.
Needle & Sharp Tools Control
Item 25Locked needle storage cabinet with authorized QMS officer signature required for any needle transaction.
Metal Detection / Needle Detection
Item 269-point calibration test every 2 hours with 1.0mm ferrous sphere; 100% sensitivity pass verified on conveyor metal detector.
Needle Replacement & Disposal
Item 27Worn and damaged needles disposed into sealed puncture-proof sharp containers with tamper-evident serial bands.
Needle Register / Needle Traceability
Item 28Traceability ledger matching needle batch code, operator machine ID, line number, and supervisor sign-off.
Root Cause Analysis
Item 29Fishbone and 5-Why analysis on seam puckering on Style ST-9914 (solved with silicon oil thread cooler and needle size decrease).
Corrective Action (CAPA)
Item 30Immediate corrective actions logged and implemented across 6 lines to recalibrate differential feed ratios on overlock machines.
Preventive Action
Item 31Updated mechanic pre-shift setup standard for lycra blend fabrics; included thread tension gauge verification before daily production start.
Corrective Action Status
Item 325 actions opened this week, 5 actions closed and verified by Quality Manager (100% on-time closure).
Quality Incident Report
Item 33Zero catastrophic quality incidents or bulk lot rejections recorded during the past 90 production days.
Quality Alert
Item 34Visual Quality Alert #QA-26-08: Caution on needle thread tension when switching from 100% cotton to cotton/poly fleece.
Non-Conformance Report (NCR)
Item 38Active formal NCRs: 0 Major NCRs, 1 Minor NCR (Thread color shade variation resolved via lot isolation).
Quality Deviation Report
Item 39Logged process deviations: Minor stitch margin variance (+0.5mm on hem fold) documented and approved under tolerance.
Quality Waiver / Approval
Item 40Buyer technical waiver log: Buyer technical representative approved 0.5cm polybag dimension concession due to eco-film supplier switch.
Process Quality Audit
Item 35Hourly technical process audit scoring line compliance with standard operating procedures (Score: 97.4%).
Product Quality Audit
Item 36Finished product physical parameters verified against approved golden samples and tech-pack specs.
Factory Quality Audit
Item 37Annual comprehensive ISO 9001:2015 quality management system audit score: 98.4% (Bureau Veritas Certified).
Buyer Quality Requirement
Item 41Customer tech manuals and quality charters digitized into shopfloor tablet terminals across all QA checkpoints.
Customer Complaint
Item 42Official retail customer complaints register: 0 active open complaints, 0 chargeback notices.
Customer Complaint Analysis
Item 43Trend analysis across 1.4 million garments shipped: Defect feedback ratio sustained below 0.01%.
Supplier Quality
Item 44Supplier quality rating evaluating yarn spinners, fabric knitters, dyehouses, and trims manufacturers.
Incoming Material Quality
Item 45Receiving dock QC: Barcode verification, shade continuity, shrinkage testing, and packaging integrity tests.
Fabric Quality
Item 46Automated fabric inspection using ASTM D5430 4-Point System (Standard limit: โค 28 points per 100 sq yds).
Trims & Accessories Quality
Item 47Safety torque test for snap buttons, eyelets, zippers, drawcords, and heat transfer care labels.
Cutting Quality
Item 48Top-Middle-Bottom ply measurement comparison verifying automated CNC Gerber cutters.
Sewing Quality
Item 49Sewing process fidelity: Needle size monitoring, thread tension calibration, and seam stretchability conformity.
Finishing Quality
Item 50Appearance and steam pressing audit: Checking for thermal shine, water spots, and moisture content (safe limit โค 12%).
Packing Quality
Item 51Carton packaging verification: Carton bursting strength (ECT 44), barcode scannability, polybag vent holes, and silica packs.
Shipment Quality
Item 52Container cleanliness, dry floor check (moisture < 14%), door seal integrity, and moisture desiccant hanging poles.
Style-wise Quality
Item 53Quality performance broken down by active garment styles: Crew Neck Tee (1.4% DHU), Fleece Hoodie (1.9% DHU), Tech Polo (1.6% DHU).
Order-wise Quality
Item 54PO-level compliance tracking: H&M PO-88219 (99.2% FPY), Zara PO-88220 (98.4% FPY), Target PO-88221 (98.1% FPY).
Line-wise Quality
Item 55Quality ranking across all 24 sewing lines: Top performer Line 03 (0.8% DHU), Line 14 under focus training (2.2% DHU).
Section-wise Quality
Item 56Divisional DHU breakdown: Cutting (0.24%), Sewing (1.84%), Finishing (0.42%), Packaging (0.12%).
Operator / Quality Inspector Performance
Item 57QC inspector appraisal: Repeatability & Reproducibility (Gage R&R) audit verified at 96.4% consistency.
Quality Training Status
Item 58Weekly quality refresher curriculum: Critical defect identification, AQL sampling math, and sewing machine tension diagnostics.
Quality SOP / Document Control
Item 59Document control registry: 48 Standard Operating Procedures maintained with digital version control and revision histories.
Quality Record & Traceability
Item 60Digital quality thread: Barcode scans link raw fabric roll ID, cutting marker, operator machine ID, and export carton barcode.
Quality Trend
Item 61Rolling 7-day DHU trend: 2.14% โ 2.05% โ 1.94% โ 1.92% โ 1.88% โ 1.85% โ 1.84% (demonstrates continuous quality improvement).
Daily Quality Summary
Item 62Today's consolidated quality audit: 17,290 garments audited, 318 defects identified, 310 reworked and cleared, 8 rejected, final pass rate 99.4%.
Weekly Quality Trend
Item 63Weekly quality performance: 104,200 garments audited across Week 38 with zero major audit findings.
Monthly Quality Trend
Item 64Quarterly quality trajectory: January MTD (2.42% DHU) โ February MTD (2.12% DHU) โ March MTD (1.84% DHU). Continuous positive improvement.
Factory QMS Summary
Item 65The facility operates in full accredited quality conformity under ISO 9001:2015, AQL 1.5 export guidelines, and buyer technical charters. Zero critical defects, zero needle security breaches, and 98.16% First Pass Yield confirm optimal factory quality posture.
Customer-Focused | Continuous Improvement
Item 66Structured PDCA (Plan-Do-Check-Act) and Kaizen initiatives driving customer satisfaction index (CSI: 98.6%) and continuous process capability improvement (Cpk: 1.48).
FINISHING OPERATIONS & PACKING READINESS CONSOLE
Thread Trimming • Vacuum Steam Pressing • Hand-Feel Treatment • Folding • Final Carton Preparation
Finishing Overview
Consolidated plant finishing operations, input intake, output throughput, and packing readinessFinishing Input
Garments received from sewing assembly lines into Floor 4 finishing receiving bay17,290 assembled garment units received today across 24 sewing lines. Handover trolley digital barcode scans confirm 100% lot number and shade matching with zero transit loss.
Finishing Output
Garments pressed, thread-sucked, inspected, and handed over to carton packing16,920 finished units completed today. 32 industrial steam vacuum tables operated with average cycle time of 32.4 seconds per garment. Zero steam moisture marks or thermal shine defects logged.
Process Progress
Flow progress across thread trimming, stain inspection, steam pressing, and foldingTarget vs Actual
Planned hourly and daily finishing quotas against real-time throughputPlanned Daily Target
Scheduled across 32 pressing tables at standard target of 70 Pcs/Hr per pressing station.
Actual Realized Output
Actual output realized: 94.0% daily quota fulfilled with 1.5 hours remaining in overtime window.
Variance / Deficit
Variance on track to be absorbed by automated folding station during evening shift closure.
Pending Quantity
Garments in staging buffer awaiting steam tunnel and final touch-up pressingCurrent pending in finishing staging: 1,240 Pcs. All pending garments staged in numbered rolling trolleys with style and size tickets clearly visible.
Output Performance
Run-rate metrics and pressing velocity across pressing table operator clustersPressing line speed averaged 66.1 Pcs/Hr per station. Peak hourly speed achieved between 14:00 – 15:00 at 74.2 Pcs/Hr following pre-heating cycle stabilization.
Efficiency Status
Calculated finishing floor efficiency vs Industrial Engineering standard SAMOverall Finishing Efficiency
Achieved against standard finishing SAM allowance of 2.4 minutes per t-shirt and 3.8 minutes per hoodie.
Steam Boiler Thermal Efficiency
Operating pressure stable at 4.5 Bar with automated condensate recovery at 82% efficiency.
Folding Status
Cardboard insert folding, tissue wrapping, and automated folding machine status16,750 garments folded and polybagged. Automatic folding machines #FM-01 & #FM-02 operated at 100% mechanical uptime with laser alignment sensors active.
Packing Preparation
Barcode price ticket scanning, hangtag attachment, and carton staging100% verification of UPC/EAN barcode stickers against buyer packing manifest. Zero mixed-size or incorrect ratio cartons detected.
Packing Readiness
Master carton assembly readiness score and warehouse loading authorizationReady for Shipment Handover
414 export cartons taped, strapped, and weighed with tolerance compliance ±0.2 kg.
Moisture Content Test
Digital pinless moisture meters confirm average 9.4% (well below 12.0% mould risk limit).
Backlog Status
Unfinished bundles exceeding 4-hour WIP threshold on Floor 4Backlog volume: 370 Pcs held for specialized rubber badge heat transfer curing. Zero aging backlog past 8 hours.
Order-wise Pending
Finishing backlog disaggregated by buyer purchase order| PURCHASE ORDER | BUYER | TOTAL ORDER | FINISHED TODAY | FINISHING PENDING | STATUS |
|---|---|---|---|---|---|
| PO-88219 | H&M Sweden | 25,000 | 4,120 | 480 Pcs | ON SCHEDULE |
| PO-88220 | Zara / Inditex | 18,000 | 3,780 | 390 Pcs | ON SCHEDULE |
| PO-88221 | Target USA | 32,000 | 5,310 | 370 Pcs | ON SCHEDULE |
Style-wise Status
Throughput segmented by garment category and construction styleST-9912 Basic Crew T-Shirt (6,700 Pcs • 98.0%), ST-9914 Women's Slim Tee (5,010 Pcs • 97.8%), ST-9920 Pullover Hoodie (5,210 Pcs • 97.7%).
Finishing Line Status
Operational status of Finishing Line 01 (Tops) and Line 02 (Fleece/Heavy)Finishing Line 01: 16 tables active, 8,920 Pcs completed. Finishing Line 02: 16 tables active, 8,000 Pcs completed. Both lines operating at 100% capacity.
Delay Status
Finishing delay log, root cause tracking, and mitigation measuresCurrent delay status: 0 Critical Delays. Minor 15-minute steam pressure stabilization pause occurred at 11:30 during boiler blowdown; absorbed without affecting dispatch.
Bottleneck Status
WIP choke points between pressing tables and manual folding stationsZero physical bottlenecking. Buffer ratio between pressing and folding maintained at healthy 1.2:1 with rolling transfer racks.
Priority Queue
Urgent purchase order sequences prioritized for early cargo cut-offPriority 1: PO-88219 (H&M Sweden • 4,200 units container loading tonight). Priority 2: PO-88220 (Zara Spain • Vessel loading Friday).
Critical Alerts
Live alerts for steam pressure, heat levels, stain risks, and packing bottlenecksZERO CRITICAL FINISHING ALERTS
All 32 steam tables operating normally. Boiler pressure nominal at 4.5 Bar. Moisture readings conformant. Zero stain contamination incidents logged.
Finishing Summary
Executive operational synthesis, cumulative daily results, and dispatch clearanceFinishing operations achieved 16,920 units today (94.0% daily target). 16,580 garments sealed and boxed into 414 export master cartons. Priority export PO-88219 container loading is 100% prepared and authorized for port transit.
Packing Report — Level-2 Factory Operations
End-of-line packaging, cartonization verification, dispatch readiness & export shipment staging
| Time Window | Floor 1 (Knit) | Floor 2 (Woven) | Floor 3 (Denim) | Floor 4 (Outerwear) | Hourly Total | Cumulative Output | Status |
|---|---|---|---|---|---|---|---|
| 08:00 — 09:00 | 580 Pcs | 420 Pcs | 390 Pcs | 210 Pcs | 1,600 Pcs | 1,600 Pcs | On Schedule |
| 09:00 — 10:00 | 740 Pcs | 510 Pcs | 460 Pcs | 280 Pcs | 1,990 Pcs | 3,590 Pcs | Peak Rate |
| 10:00 — 11:00 | 720 Pcs | 495 Pcs | 450 Pcs | 265 Pcs | 1,930 Pcs | 5,520 Pcs | Target Met |
| 11:00 — 12:00 | 710 Pcs | 525 Pcs | 440 Pcs | 270 Pcs | 1,945 Pcs | 7,465 Pcs | Target Met |
| 12:00 — 13:00 | Factory Lunch & Maintenance Staggered Interval | 7,465 Pcs | Lunch Break | ||||
| 13:00 — 14:00 | 760 Pcs | 530 Pcs | 480 Pcs | 290 Pcs | 2,060 Pcs | 9,525 Pcs | Peak Output |
| 14:00 — 15:00 | 735 Pcs | 505 Pcs | 465 Pcs | 275 Pcs | 1,980 Pcs | 11,505 Pcs | Steady Flow |
| 15:00 — 16:00 | 750 Pcs | 515 Pcs | 470 Pcs | 280 Pcs | 2,015 Pcs | 13,520 Pcs | Target Met |
| 16:00 — 17:00 | 780 Pcs | 540 Pcs | 490 Pcs | 295 Pcs | 2,105 Pcs | 15,625 Pcs | Peak Final |
| 17:00 — 17:30 (Partial) | 350 Pcs | 250 Pcs | 225 Pcs | 130 Pcs | 955 Pcs | 16,580 Pcs | Shift Closing |
| Production Floor | Target (Pcs) | Actual (Pcs) | Variance (Pcs) | Achievement % | Variance Explanation |
|---|---|---|---|---|---|
| Floor 1: Knit Tops | 6,800 | 6,490 | -310 | 95.4% | Minor size-sticker mismatch on Line 3 resolved in 15 mins |
| Floor 2: Woven Shirts | 4,800 | 4,545 | -255 | 94.7% | Cardboard collar insert batch replenishment delay |
| Floor 3: Denim Bottoms | 3,800 | 3,640 | -160 | 95.8% | Heavy waist tag gun pin replacement downtime |
| Floor 4: Outerwear | 2,100 | 1,905 | -195 | 90.7% | Hanger loop folding complexity on down jacket PO-7740 |
| Carton Spec / Code | Dimensions (L x W x H cm) | Pcs / Carton | Cartons Completed | Total Garments | Gross Weight (Kg) | Total CBM |
|---|---|---|---|---|---|---|
| CTN-A (T-Shirts Flat) | 60 x 40 x 30 | 48 Pcs | 142 Ctn | 6,816 Pcs | 1,988 Kg | 10.22 CBM |
| CTN-B (Polo Shirts Solid) | 60 x 40 x 35 | 36 Pcs | 110 Ctn | 3,960 Pcs | 1,540 Kg | 9.24 CBM |
| CTN-C (Woven Dress Shirts) | 65 x 45 x 30 | 24 Pcs | 86 Ctn | 2,064 Pcs | 1,204 Kg | 7.55 CBM |
| CTN-D (Denim Jeans Fold) | 60 x 40 x 40 | 20 Pcs | 52 Ctn | 1,040 Pcs | 1,144 Kg | 4.99 CBM |
| CTN-E (Jackets & Outerwear) | 70 x 50 x 45 | 12 Pcs | 24 Ctn | 288 Pcs | 672 Kg | 3.78 CBM |
| PO Number | Buyer | Style Name | Total PO Qty | Packed Today | Pending Today | Target Completion |
|---|---|---|---|---|---|---|
| PO-88219 | H&M Group | Regular Crew Neck Tee | 25,000 Pcs | 4,200 Pcs | 300 Pcs | 18:15 Today |
| PO-88340 | Inditex (Zara) | Slim Fit Oxford Shirt | 18,000 Pcs | 2,850 Pcs | 250 Pcs | 18:30 Today |
| PO-89105 | Target Sourcing | Stretch Chino Trouser | 15,000 Pcs | 2,100 Pcs | 210 Pcs | 18:45 Today |
| PO-89240 | Gap Inc. | Fleece Zip Hoodie | 12,000 Pcs | 1,800 Pcs | 160 Pcs | 18:00 Today |
| Line ID | Product Category | Allocated SAM (Min) | Actual Avg Cycle (Min) | Labor Efficiency % | Rework % | Operator Rating |
|---|---|---|---|---|---|---|
| PACK-L01 | Basic Knit Crew Tees | 0.45 | 0.47 | 95.7% | 0.2% | Grade A |
| PACK-L02 | Woven Long Sleeve Shirts | 0.85 | 0.92 | 92.4% | 0.4% | Grade A |
| PACK-L03 | 5-Pocket Denim Jeans | 0.70 | 0.78 | 89.7% | 0.3% | Grade B+ |
| PACK-L04 | Technical Hoodies & Jackets | 1.10 | 1.24 | 88.7% | 0.5% | Grade B+ |
| PO # | Buyer | Total Order (Pcs) | Packed to Date | Packed Today | Balance Left | Contract Fulfillment |
|---|---|---|---|---|---|---|
| PO-88219 | H&M Group | 25,000 | 21,800 | 4,200 | 3,200 | 87.2% |
| PO-88340 | Inditex (Zara) | 18,000 | 16,200 | 2,850 | 1,800 | 90.0% |
| PO-89105 | Target Sourcing | 15,000 | 13,500 | 2,100 | 1,500 | 90.0% |
| PO-89240 | Gap Inc. | 12,000 | 10,400 | 1,800 | 1,600 | 86.7% |
| Style No | Garment Description | Fabric Spec | Colorways | Assortment Type | Cartons Finished |
|---|---|---|---|---|---|
| STY-8821 | Essential Crew Neck Tee | 100% Organic BCI Cotton (160 GSM) | Black, White, Navy | Solid Size / Solid Color | 142 Ctn |
| STY-5420 | Tailored Oxford Button-Down | 60/40 CVC Yarn Dye (120 GSM) | Sky Blue, White, Pink | Ratio Pack (S:1 M:2 L:2 XL:1) | 110 Ctn |
| STY-9011 | Straight Fit 5-Pocket Denim | 12.5 oz Ring Spun Denim 2% Spandex | Vintage Dark Wash, Indigo | Solid Waist / Length Assorted | 86 Ctn |
| STY-7740 | Brushed Fleece Heavy Zip Hoodie | 80/20 Cotton-Poly French Terry (320 GSM) | Heather Grey, Forest Green | Flat Pack / Heavy Polybag | 52 Ctn |
| Queue Lot ID | Source Finishing Line | Garment Item | Queue Qty (Pcs) | Wait Time (Mins) | Priority Level | Next Assigned Station |
|---|---|---|---|---|---|---|
| Q-LOT-441 | Finishing Line F-01 (Ironing) | Crew Neck Tees (Navy) | 420 Pcs | 12 Mins | Normal | Packing Belt 01 |
| Q-LOT-442 | Finishing Line F-03 (Tunnel Finisher) | Oxford Shirts (White) | 360 Pcs | 18 Mins | Normal | Packing Belt 02 |
| Q-LOT-443 | Finishing Line F-02 (Button/Snap) | Stretch Denim (Indigo) | 280 Pcs | 24 Mins | Expedited | Packing Belt 03 |
| Q-LOT-444 | Finishing Line F-04 (Steam Dolly) | Heavy Zip Hoodies (Grey) | 180 Pcs | 9 Mins | Normal | Packing Belt 04 |
| PO # | Buyer | Forwarder / Carrier | Pending Qty (Pcs) | Pending Reason | Scheduled Release | Action Required |
|---|---|---|---|---|---|---|
| PO-88219 | H&M Group | Maersk Logistics (Chittagong Port) | 3,200 Pcs | Final 59 Cartons in sealing tunnel | Today 19:30 | Complete final strapping batch |
| PO-88340 | Inditex (Zara) | Kuehne+Nagel Air Freight (DAC) | 1,800 Pcs | Awaiting Buyer SGS Certificate sign-off | Tomorrow 08:00 | Upload digital QA stamp to portal |
| Incident ID | Line / Area | Delay Category | Downtime (Mins) | Impact (Pcs) | Root Cause | Corrective Action Taken |
|---|---|---|---|---|---|---|
| INC-PK-01 | Pack Line 02 | Packaging Material | 18 Mins | 60 Pcs | Cardboard collar band size L temporary stockout | Auxiliary store buffer stock retrieved immediately |
| INC-PK-02 | Pack Line 04 | Machinery / Tooling | 12 Mins | 35 Pcs | Semi-automatic carton sealer heating element tripped | Electrician reset thermal circuit; standby unit deployed |
Shift Handover & Packaging Department Sign-Off
Engr. K. Rahman • ID #LIRF-PK-08
Md. Zahid Hasan • ID #LIRF-QA-14
Al-Amin Hossain • ID #LIRF-WH-03
Inspection Report — Level-2 Quality Assurance Console
In-line quality gates, roving audits, end-line stations, AQL statistical sampling & defect categorization
| Time Window | Inline Sewing Check | Endline 100% Check | Finishing QC Gate | Final AQL Room | Hourly Total | Cumulative Output | Status |
|---|---|---|---|---|---|---|---|
| 08:00 — 09:00 | 520 Pcs | 610 Pcs | 390 Pcs | 180 Pcs | 1,700 Pcs | 1,700 Pcs | Nominal |
| 09:00 — 10:00 | 640 Pcs | 730 Pcs | 480 Pcs | 220 Pcs | 2,070 Pcs | 3,770 Pcs | Peak Rate |
| 10:00 — 11:00 | 610 Pcs | 710 Pcs | 460 Pcs | 210 Pcs | 1,990 Pcs | 5,760 Pcs | Target Met |
| 11:00 — 12:00 | 630 Pcs | 725 Pcs | 475 Pcs | 230 Pcs | 2,060 Pcs | 7,820 Pcs | Target Met |
| 12:00 — 13:00 | Staggered Factory Lunch Interval & Sensor Calibration | 7,820 Pcs | Lunch Break | ||||
| 13:00 — 14:00 | 650 Pcs | 750 Pcs | 490 Pcs | 240 Pcs | 2,130 Pcs | 9,950 Pcs | Peak Flow |
| 14:00 — 15:00 | 620 Pcs | 720 Pcs | 470 Pcs | 225 Pcs | 2,035 Pcs | 11,985 Pcs | Target Met |
| 15:00 — 16:00 | 640 Pcs | 740 Pcs | 480 Pcs | 235 Pcs | 2,095 Pcs | 14,080 Pcs | Target Met |
| 16:00 — 17:00 | 660 Pcs | 760 Pcs | 510 Pcs | 250 Pcs | 2,180 Pcs | 16,260 Pcs | Peak Final |
| 17:00 — 17:30 (Partial) | 310 Pcs | 360 Pcs | 240 Pcs | 110 Pcs | 1,020 Pcs | 17,280 Pcs | Shift Closing |
| Inspection Division | Planned Target (Pcs) | Actual Inspected (Pcs) | Variance (Pcs) | Achievement Rate | Audit Condition |
|---|---|---|---|---|---|
| Floor 1: Fabric & Cutting QA | 2,200 | 2,150 | -50 | 97.7% | 4-Point Fabric Roll Verification Completed |
| Floor 2: Sewing Assembly Inline | 7,500 | 7,240 | -260 | 96.5% | Minor skip-stitch adjustment on Line 5 |
| Floor 3: Sewing Assembly Endline | 5,500 | 5,280 | -220 | 96.0% | 100% Table Inspection Passing Rate High |
| Floor 4: Finishing & AQL Room | 2,800 | 2,610 | -190 | 93.2% | Statistical AQL 1.5 Sampling Passed |
| Defect Code | Defect Description | Severity Level | Defect Count | % of Total | Corrective Action Taken | Status |
|---|---|---|---|---|---|---|
| DEF-01 | Loose / Untrimmed Thread Ends | Minor | 112 | 35.2% | Trimming scissors batch re-sharpening | Resolved |
| DEF-02 | Skipped Stitches on Hem Seam | Major | 64 | 20.1% | Needle timing adjusted on Line 4 | Resolved |
| DEF-03 | Uneven Stitch Density / SPI Mismatch | Major | 48 | 15.1% | Differential feed dog calibrated | Resolved |
| DEF-04 | Puckering at Armhole Seam | Major | 38 | 11.9% | Thread tension eased by mechanic | Resolved |
| DEF-05 | Washable Spot / Removable Dirt | Minor | 32 | 10.1% | Spot cleaning gun applied with approved solvent | Cleaned |
| DEF-06 | Size Spec Measurement Out of Tol (>1/4") | Major | 14 | 4.4% | Pattern alignment re-checked in Spreading | Monitored |
| DEF-07 | Fabric Tear / Broken Needle Hole | Critical | 10 | 3.1% | Machine quarantined; needles audited | Scrapped |
| Lot ID | PO # | Buyer | Style Name | Lot Qty (Pcs) | Sampling Standard | Target Release Time |
|---|---|---|---|---|---|---|
| LOT-8821-B | PO-88219 | H&M Group | Regular Crew Neck Tee | 2,400 Pcs | ISO 2859-1 Level II (125 Pcs) | Today 18:15 |
| LOT-5420-C | PO-88340 | Inditex (Zara) | Slim Fit Oxford Shirt | 1,800 Pcs | ISO 2859-1 Level II (125 Pcs) | Today 18:30 |
| LOT-9011-A | PO-89105 | Target Sourcing | Stretch Chino Trouser | 1,500 Pcs | ISO 2859-1 Level II (125 Pcs) | Today 18:45 |
| Lot ID | Style # | Buyer | Quantity | Sample Tested | Found Defects | AQL Result | Lot Disposition |
|---|---|---|---|---|---|---|---|
| LOT-8821-A | STY-8821 | H&M Group | 5,000 Pcs | 200 Pcs | 2 Minor | PASSED | Released to Packaging |
| LOT-5420-A | STY-5420 | Inditex (Zara) | 4,200 Pcs | 200 Pcs | 1 Major, 1 Minor | PASSED | Released to Packaging |
| LOT-5420-B | STY-5420 | Inditex (Zara) | 3,800 Pcs | 200 Pcs | 3 Minor | PASSED | Released to Packaging |
| LOT-9011-P | STY-9011 | Target Sourcing | 3,500 Pcs | 125 Pcs | 2 Major | PASSED | Released to Packaging |
| Bundle / Lot ID | Original Defect | Alteration Operator | Re-Inspecting Auditor | Re-Audit Verdict | Sign-Off Timestamp |
|---|---|---|---|---|---|
| BDL-441-09 | Skipped stitch on sleeve hem | Op. Nasreen Akter | QA Lead M. Hasan | CLEARED | 16:42 Today |
| BDL-442-14 | Loose thread on buttonhole | Op. Farida Begum | QA Lead S. Parveen | CLEARED | 16:55 Today |
| BDL-443-02 | Puckered pocket flap seam | Op. Rokeya Sultana | QA Lead M. Hasan | CLEARED | 17:10 Today |
| Hold ID | PO # | Buyer | Hold Category | Held Qty | Hold Reason | Resolution Plan | Status |
|---|---|---|---|---|---|---|---|
| HLD-QA-08 | PO-88219 | H&M Group | Shade Variation Check | 180 Pcs | Roll end slight shade tone variation under D65 light box | Buyer technical QA digital spectrometer review | Under Lab Review |
| Style No | Garment Category | Fabric Spec | Inspected (Pcs) | Pass Rate % | DHU % | Top Recorded Defect |
|---|---|---|---|---|---|---|
| STY-8821 | Essential Crew Neck Tee | 100% Organic BCI Cotton (160 GSM) | 6,800 | 98.9% | 1.12% | Loose thread on bottom hem |
| STY-5420 | Tailored Oxford Button-Down | 60/40 CVC Yarn Dye (120 GSM) | 4,800 | 97.8% | 2.05% | Collar point symmetry mismatch |
| STY-9011 | Straight Fit 5-Pocket Denim | 12.5 oz Ring Spun Denim 2% Spandex | 3,680 | 98.1% | 1.75% | Waistband chainstitch tension |
| STY-7740 | Brushed Fleece Heavy Zip Hoodie | 80/20 Cotton-Poly French Terry (320 GSM) | 2,000 | 97.2% | 2.45% | Zipper waviness / seam puckering |
| PO # | Buyer | Total PO Qty | Total Inspected | Pass Rate | Current AQL Posture | Shipment Clearance |
|---|---|---|---|---|---|---|
| PO-88219 | H&M Group | 25,000 Pcs | 22,100 Pcs | 98.6% | AQL 1.5 Conformant (Passed) | Cleared for Staging |
| PO-88340 | Inditex (Zara) | 18,000 Pcs | 16,500 Pcs | 98.2% | AQL 1.5 Conformant (Passed) | Cleared for Staging |
| PO-89105 | Target Sourcing | 15,000 Pcs | 13,800 Pcs | 98.0% | AQL 1.5 Conformant (Passed) | Cleared for Staging |
| PO-89240 | Gap Inc. | 12,000 Pcs | 10,600 Pcs | 97.6% | AQL 1.5 Conformant (Passed) | Cleared for Staging |
| Auditor Name | ID # | Assigned Station | Units Audited | Defects Caught | Audit Accuracy % | Inspector Grade |
|---|---|---|---|---|---|---|
| Md. Zahid Hasan | LIRF-QA-01 | Final AQL Audit Room | 680 Pcs | 14 | 99.4% | Master Lead |
| Shahana Parveen | LIRF-QA-08 | Sewing Line 04 (Endline) | 820 Pcs | 22 | 98.8% | Senior Auditor |
| Tariqul Islam | LIRF-QA-15 | Sewing Line 08 (Inline) | 740 Pcs | 18 | 98.2% | Senior Auditor |
| Nusrat Jahan | LIRF-QA-24 | Finishing Table 02 | 790 Pcs | 16 | 97.9% | Auditor |
| Performance Dimension | Factory Standard Target | Actual Performance Today | Variance | Risk Rating | Evaluation Verdict |
|---|---|---|---|---|---|
| Endline Inspection Cycle Time | 28 Sec / Garment | 26 Sec / Garment | -2 Sec (Faster) | Low | Optimal Efficiency |
| Defect Escape Probability | ≤ 0.20% | 0.08% | -0.12% (Better) | Low | High Accuracy |
| Auditor Repeatability (Gauge R&R) | ≥ 92.0% | 96.4% | +4.4% (Higher) | Low | Excellent Consistency |
| Customer AQL Rejection Risk | ≤ 1.0% | 0.00% | Zero Risk | Zero | Pre-Shipment Guaranteed |
QA Department Executive Certification & Release Sign-Off
Engr. Mahbubul Haque • Lead Auditor ISO 9001
Md. Zahid Hasan • ID #LIRF-QA-01
K. M. Ashraful Alam • ID #LIRF-DIR-04
Overall KPI Status — Level-2 Factory Performance Scorecard
Executive scorecard, multi-tier weighted KPI metrics, departmental efficiency, and operational benchmarks
| Pillar Domain | Primary Metric | Benchmark Target | Actual Today | Weight | Weighted Score | Health Status |
|---|---|---|---|---|---|---|
| Production Volume | Daily Garments Produced | 18,000 Pcs | 17,290 Pcs | 25% | 24.01 pts | Target Met |
| Plant Efficiency | Labor & Line Efficiency | 68.0% | 71.4% | 20% | 20.00 pts | Exceeded |
| Quality Assurance | End-of-Line DHU | ≤ 2.20% | 1.84% | 20% | 19.65 pts | Exceeded |
| Equipment OEE | Overall Equipment Effectiveness | 85.0% | 87.4% | 15% | 14.85 pts | Exceeded |
| On-Time Delivery (OTD) | Shipment Dispatch Schedule | 98.0% | 99.2% | 10% | 10.00 pts | Exceeded |
| Compliance & 5S | Audit Conformance Rating | 95.0% | 98.4% | 10% | 9.84 pts | Exceeded |
| Performance Metric | Planned Target | Actual Performance | Absolute Variance | Relative Variance % | Direction |
|---|---|---|---|---|---|
| Sewing Daily Output | 18,000 Pcs | 17,290 Pcs | -710 Pcs | -3.9% | Slight Deficit |
| Factory Overall Efficiency | 68.0% | 71.4% | +3.4% | +5.0% | Favorable |
| Quality DHU Rate | 2.20% | 1.84% | -0.36% | -16.4% | Favorable (Lower) |
| Non-Productive Time (NPT) | ≤ 5.0% | 3.4% | -1.6% | -32.0% | Favorable (Lower) |
| Category | Weight % | Strategic Priority | Rationale |
|---|---|---|---|
| Production Volume | 25.0% | High | Fulfillment of contractual buyer delivery quantities |
| Labor & Line Efficiency | 20.0% | High | Direct impact on cost per garment (CM) profitability |
| Quality Assurance & DHU | 20.0% | High | Protection against chargebacks, AQL rejection, and buyer penalties |
| Equipment Reliability (OEE) | 15.0% | Medium | Machine uptime and maintenance prevention |
| On-Time Delivery (OTD) | 10.0% | High | Customer satisfaction and freight forwarder coordination |
| Compliance & Housekeeping | 10.0% | Mandatory | Social compliance, buyer audits (WRAP, BSCI), and 5S protocols |
Evaluated under ISO 9001:2015, HIGG FEM 3.0, and Buyer Quality Charter Standards.
| Line ID | Style Item | Hourly Run Rate | Shift Output | Efficiency % | DHU % | Status |
|---|---|---|---|---|---|---|
| Line 01 | Crew Neck Tee | 110 Pcs/hr | 980 Pcs | 78.2% | 1.12% | Exceeded |
| Line 04 | Polo Shirt | 95 Pcs/hr | 850 Pcs | 74.5% | 1.45% | Target Met |
| Line 08 | Oxford Shirt | 88 Pcs/hr | 790 Pcs | 71.8% | 1.85% | Target Met |
| Line 12 | Denim Trouser | 80 Pcs/hr | 710 Pcs | 69.4% | 1.95% | Nominal |
| Department | Head of Section | Target Score | Actual Score | Efficiency Rating | Cost Variance | Overall Grade |
|---|---|---|---|---|---|---|
| Raw Materials Store | M. R. Karim | 90.0 | 94.8 | 95.4% | -1.2% (Savings) | Grade A |
| Cutting & Spreading | T. Ahmed | 92.0 | 96.8 | 82.4% | -2.1% (Savings) | Grade A+ |
| Sewing & Assembly | Engr. M. Haque | 92.0 | 94.2 | 71.4% | +0.4% | Grade A |
| Finishing & Pressing | S. K. Paul | 90.0 | 95.0 | 88.6% | -0.8% | Grade A |
| Rank | Line Name | Supervisor | Target (Pcs) | Actual (Pcs) | Efficiency % | DHU % | OEE % |
|---|---|---|---|---|---|---|---|
| #1 | Line 01 (Knit Tops) | Md. Rafiqul Islam | 950 | 980 | 78.2% | 1.12% | 91.4% |
| #2 | Line 02 (Knit Tops) | Abdul Mannan | 950 | 965 | 76.8% | 1.24% | 89.6% |
| #3 | Line 05 (Woven Shirts) | K. M. Ashraful | 800 | 820 | 75.4% | 1.38% | 88.2% |
| #4 | Line 10 (Denim Bottoms) | Nurul Huda | 700 | 715 | 73.2% | 1.65% | 87.0% |
| Metric Name | Day -6 | Day -5 | Day -4 | Day -3 | Day -2 | Yesterday | Today | Trend Direction |
|---|---|---|---|---|---|---|---|---|
| Plant Efficiency % | 68.4% | 69.1% | 69.8% | 70.2% | 70.8% | 71.1% | 71.4% | ↑ Steady Improvement |
| DHU % (Quality) | 2.14% | 2.05% | 1.98% | 1.94% | 1.90% | 1.88% | 1.84% | ↓ Favorable Drop |
| Output Volume | 16,840 | 17,010 | 17,150 | 17,190 | 17,220 | 17,250 | 17,290 | ↑ Volume Climbing |
| Strategic Indicator | Current Month (MTD) | Last Month | Same Month Last Year | YoY Growth |
|---|---|---|---|---|
| Factory Overall Efficiency | 71.4% | 69.2% | 64.5% | +6.9% YoY |
| Garment DHU Rate | 1.84% | 2.05% | 2.48% | -0.64% YoY (Favorable) |
| Average Machine OEE | 87.4% | 85.8% | 81.2% | +6.2% YoY |
| Factory Production Volume | 348,200 Pcs | 332,000 Pcs | 298,000 Pcs | +16.8% YoY |
| Metric Name | Budget Target | Current Value | Variance Value | Tolerance Limit | Risk Classification |
|---|---|---|---|---|---|
| Sewing Daily Volume | 18,000 Pcs | 17,290 Pcs | -710 Pcs | ± 5.0% (±900) | Within Limit (Low) |
| Sewing Line Efficiency | 68.0% | 71.4% | +3.4% | ± 3.0% | Favorable Overperformance |
| Quality DHU % | 2.20% | 1.84% | -0.36% | Max 2.50% | Controlled (Optimal) |
Executive Operations Director Sign-Off
Engr. Tariqul Islam • COO Division
Dr. K. R. Chowdhury • Lead IE Specialist
Mahbubul Haque • Lead QMS Auditor
OPT Skill Matrix Floor Solution Level 2
Master operator for critical collar attach & cuff setting. Zero quality defects recorded in past 45 days.
Critical shortage in 2-needle flatlock chainstitch operators across Lines 04 & 05. 3 lines currently running at reduced pace due to sleeve hem bottleneck.
Active cross-skilling program pairing Grade A operators with Grade B learners for collar placket and overlock profile switching.
Takt time variance minimized across 12 lines. Operator reallocation recommended on Line 03 to alleviate back yoke lag.
Predicted 4.2% output dip if 2 key multi-skill operators on Line 02 are absent simultaneously without designated floaters.
Pool of 64 certified floater operators ready for immediate deployment to cover leave, unplanned downtime, or surge requirements.
18 Grade B+ operators have passed 3-month quality thresholds (>90% efficiency, <0.5% DHU) and are approved for Grade A promotion.
On-demand correlation analysis between operator SMV performance, ergonomic station setups, and fabric weight elasticity.
| Item # | Operator Code | Operator Name | Assigned Line | Grade | Skill Level | Efficiency | Attendance | Score | Experience | Certified Operations |
|---|---|---|---|---|---|---|---|---|---|---|
| #28 | OP-001 | Fatima Begum | Line 01 | Grade A+ | Expert | 96.4% | 98.5% | 96/100 | 5.5 yrs | Collar Join, Cuff Attach, Overlock |
| #29 | OP-002 | Mohammad Rafiq | Line 01 | Grade A | Expert | 91.8% | 95.0% | 92/100 | 4.2 yrs | Sleeve Attach, Side Seam |
| #30 | OP-003 | Nasrin Akhtar | Line 02 | Grade A | Skilled | 89.2% | 94.2% | 89/100 | 3.8 yrs | Front Placket, Button Hole |
| #31 | OP-004 | Kamal Hossain | Line 02 | Grade B+ | Skilled | 84.5% | 92.0% | 85/100 | 2.9 yrs | Pocket Setting, Top Stitch |
| #32 | OP-005 | Rokeya Khatun | Line 03 | Grade B | Skilled | 79.8% | 91.5% | 80/100 | 2.4 yrs | Bottom Hemming, Flatlock |
| #33 | OP-006 | Shahidul Islam | Line 03 | Grade B | Learning | 77.3% | 88.0% | 77/100 | 1.8 yrs | Back Yoke, Shoulder Join |
| #34 | OP-007 | Jasmine Ara | Line 04 | Grade B- | Learning | 73.2% | 89.5% | 73/100 | 1.3 yrs | Armhole Binding, Neck Rib |
| #35 | OP-008 | Anwar Hossain | Line 04 | Grade C+ | Learning | 68.9% | 86.0% | 69/100 | 1.0 yr | Label Attach, Care Tag |
| #36 | OP-009 | Salma Parvin | Line 05 | Grade C | Under Training | 62.4% | 85.0% | 62/100 | 0.6 yr | Single Needle Prep, Bar Tack |
| #37 | OP-010 | Tarun Mia | Line 05 | Grade C | Under Training | 59.8% | 82.5% | 60/100 | 0.4 yr | Thread Trimming, Helper Seam |
| #38 | OP-011 | Bilkis Banu | Line 06 | Grade D | Under Training | 48.5% | 78.0% | 49/100 | 0.2 yr | Bundle Moving, Tagging |
| #39 | OP-012 | Mizanur Rahman | Line 06 | Grade N/Q | Not Qualified | 41.2% | 71.5% | 41/100 | 0.1 yr | Under Evaluation (Induction) |
Total identified gap: 42 operation positions. 28 positions currently compensated through overtime and floater reassignment.
Need 35 operators for 2-week fast-track curve stitch training and 18 for computer-controlled eyelet buttonhole machines.
12 pending resignation and maternity replacement requisitions approved by HR for onboarding by Monday.
- Line 01: Operating at 96.4% peak efficiency with complete Grade A operator staffing. No bottlenecks observed. Optimal
- Line 02: Pocket setting cycle time +1.8s above target; junior operator paired with master operator Rafiq for coaching. Under Review
- Line 03: Style changeover underway (Polo to Crew Neck). 6 multi-skilled floaters deployed to assist line loading. In Progress
- Line 04: Armhole binding operator deficit flagged. Immediate floater transfer recommended by AI Skill Advisor. Action Needed
OPT Yearly Evaluation Floor Solution Level 2
| Date | Operation | Target | Actual | Achieve % | Alter Pcs | Alter % | Daily Eval | Attendance |
|---|---|---|---|---|---|---|---|---|
| 15-Mar-2026 | Collar Join | 480 | 485 | 101.0% | 4 | 0.82% | 98.4% | Present |
| 14-Mar-2026 | Collar Join | 480 | 492 | 102.5% | 3 | 0.61% | 99.1% | Present |
| 13-Mar-2026 | Collar Join | 480 | 478 | 99.6% | 5 | 1.05% | 97.2% | Present |
| 12-Mar-2026 | Cuff Attach | 500 | 510 | 102.0% | 2 | 0.39% | 99.5% | Present |
| 11-Mar-2026 | Collar Join | 480 | 0 | 0.0% | 0 | 0.00% | 0.0% | Absent (Leave) |
| 10-Mar-2026 | Collar Join | 480 | 488 | 101.7% | 4 | 0.82% | 98.5% | Present |
| 09-Mar-2026 | Collar Join | 480 | 472 | 98.3% | 6 | 1.27% | 96.0% | Present |
LX AI Insights Floor Solution Level 2
| Timestamp | Category | Impacted Area | Detected Anomaly | LX Intelligence Recommendation | Assigned Owner | Status |
|---|---|---|---|---|---|---|
14:22:15 |
Machine Problem | Line 04 ยท M/C #108 | Feed dog slippage & skip stitches | Replace feed dog with fine-tooth silicon model | Tariqul Islam | In Progress |
13:45:00 |
Production Drop | Line 02 ยท Placket | Cycle time +2.1s above pitch | Pair junior operator with master sewer OP-001 | Jahangir Alam | Resolved |
12:10:30 |
Quality Anomaly | Line 06 ยท Bottom Hem | Needle puckering on knit jersey | Lower thread tension by 0.5cN; switch ballpoint needle | Fatema QC | Resolved |
11:30:45 |
NPT Loss | Line 01 ยท Collar Attach | Thread breakage cluster (3 breaks / 10m) | Swap thread spool lot; lubricate hook race | Mechanic Rafiq | Resolved |
10:15:20 |
Material Shortage | Line 03 ยท Binding | Rib fabric bundle delay from store | Expedite batch #RB-402 via smart material runner | Store Supervisor | Resolved |
09:05:10 |
Manpower Shortage | Line 05 ยท Overlock | Operator absence on 2-needle machine | Reallocate cross-skilled floater OP-003 | Line Leader | Resolved |
Factory Improvement Idea | Suggestions Floor Solution Level 2
Manual bundle tagging causes 4.2 min search lag per cart during style changeover at sewing loading.
Implement QR-coded smart RFID bin clips linked to Leadirftex Floor Tracker for instant cart discovery.
Bi-weekly Kaizen Steering Committee reviewed 27 submissions. 14 fast-tracked for immediate floor deployment.
Annualized productivity gains: +6.8% line efficiency, -14% alteration frequency across 12 sewing lines.
| ID | Date | Submitter | Area | Category | Suggested Solution | Priority | Review Status | Owner |
|---|---|---|---|---|---|---|---|---|
| IDEA-101 | 16-Mar-2026 | Rafiqul Islam | Line 04 | Efficiency | Pre-wound magnetic bobbin cases for fast changeover | High | Under Review | Mahfuzur Rahman |
| IDEA-098 | 14-Mar-2026 | Fatima Begum | Line 01 | Quality | Needle cooling air-jet to prevent polyester puckering | High | Accepted | Tariqul Islam |
| IDEA-095 | 10-Mar-2026 | Kamal Hossain | Cutting | Cost Reduction | End-bit nesting template to salvage 1.8% fabric waste | Medium | Accepted | Jahangir Alam |
| IDEA-091 | 07-Mar-2026 | Nasrin Akhtar | Finishing | Safety | Ergonomic steam iron grip sleeve to reduce wrist strain | Medium | Accepted | Safety Officer |
| IDEA-088 | 03-Mar-2026 | Shahidul Islam | Line 03 | Machine | Quick-release presser foot bracket on Overlock machines | Low | Under Review | Tariqul Islam |
| IDEA-082 | 26-Feb-2026 | Anwar Hossain | Warehouse | Process | Eliminate cardboard separators between bundle trays | Low | Rejected | Store Head |
๐ข Shipment Report Level-2 Executive Logistics
DO IT RIGHT THE FIRST TIME.
Empowering frontline manufacturing associates, technical specialists, certified fabric mills, and global brands with lean digitalization, verified audits, and real-time execution.
Social Account Cover Studio
Cinematic corporate cover design communicating brand identity, business positioning, textile & apparel technology, and the connected industrial ecosystem from sourcing to dispatch.
Social Post & Feed Content Studio
Multi-format social post generator adapting campaign and technical feed posts across LinkedIn, Instagram, X/Twitter, and Facebook feeds. (Preserved for content publishing workflows).
Leadirftex B2B Network Inquiry
Connect with our centralized merchandising and production management desk for capacity booking and technical dossiers.
Privacy & Data Protection Policy
Effective Date: September 18, 2026 • Domain: leadirftex.com • Version 2.4-Enterprise
1. Foundational Commitment & Zero-Data-Monetization
Leadirftex (“Leadirftex Interchain”, “we”, “us”, or “our”) operates as an authoritative industrial B2B intelligence and supply chain orchestration network under planned domain https://leadirftex.com. Our fundamental operating principleโ“Do It Right the First Time”โapplies equally to data governance, manufacturing confidentiality, and intellectual property protection. Leadirftex does not sell, rent, monetize, or lease factory, supplier, or brand data to any third party.
2. Operational Scope of Data Ingestion
To enable real-time floor intelligence, automated machine integration, and supply chain transparency, Leadirftex processes:
- Production Floor & QA Telemetry: Machine telemetry, IoT sensor feeds, NPT stoppage diagnostics, sewing throughput matrices, and AQL 1.5 / 2.5 inspection logs.
- Enterprise Identity & Compliance Credentials: Audited tax/trade registrations, factory social compliance certifications (WRAP, BSCI, SEDEX, OEKO-TEX), and verified export dossiers.
- Talent Layer Matching Data: Technical operator competencies, verified skill assessments, and CV credentials managed under user-permitted zero-cost placement protocols.
3. LX Intelligence & Isolated Enclave Processing
Telemetry analyzed by LX Intelligence is processed strictly inside isolated, compartmentalized execution enclaves to optimize line balancing and eliminate bottlenecks. Proprietary garment tech-packs, CAD vector patterns, and private bill-of-materials (BOM) are never exposed to public AI models or used for third-party foundation model training.
4. Strict Private Price & Commercial Enclave Protection
All manufacturer price quotes, FOB target matrices, escrow agreements, and commercial margins are treated as cryptographically sealed commercial secrets. Price negotiations are visible solely to the designated counterparty and are structurally shielded from competing suppliers and marketplace brokers.
5. Enterprise Infrastructure & Security Standards (FIPS 140-3 HSM & mTLS)
Leadirftex enforces rigorous Zero-Trust architecture across all nodes: TLS 1.3 encryption in-transit, hardware security module (FIPS 140-3 HSM) root-of-trust, AES-256 encryption at-rest, and mutual TLS (mTLS) for all industrial IoT and automated machine telemetry endpoints. Cryptographic audit trails are immutably logged for transparent dispute mediation.
6. Zero-Cost Talent Layer Data Rights
Technical jobseekers and factory professionals retain full sovereign ownership over their profile data. Candidate dossiers, CV builders, and verification badges are never paywalled, and talent records are never brokered to recruiters without explicit, granular consent.
7. Data Retention, Portability & Deletion Rights
Participating garment factories, fabric mills, and brand accounts maintain complete data portability rights. Verified authorized administrators can request structured JSON/CSV data archives or initiate permanent record de-provisioning upon off-boarding, subject to statutory multi-sig audit archival mandates.
8. Contact & Data Protection Officer (DPO)
For inquiries, compliance audits, or formal data subject rights requests, reach out directly to our corporate data governance desk:
Leadirftex Enterprise Data Governance • Attn: Legal OfficerTerms & Conditions of Service
Effective Date: September 18, 2026 • Domain: leadirftex.com • Version 2.4-Enterprise
1. Operational Agreement & Enterprise Scope
By accessing or interacting with Leadirftex (“Leadirftex Interchain”, “the Platform”, https://leadirftex.com), manufacturing facilities, brand sourcing representatives, fabric mills, and registered professionals agree to be bound by these Terms & Conditions. These provisions establish authoritative standards governing B2B procurement workflows, factory telemetry integration, and multi-tier supply chain orchestration.
2. Core Operational Principle: “Do It Right the First Time”
Leadirftex operates upon verified frontline craftsmanship, personal accountability, and process discipline. Facilities onboarding to the Leadirftex network commit to embedding self-inspection standards, proactive error mitigation, and continuous quality calibration into daily operations. Inspection benchmarks must be maintained consistently across all production shifts, not merely staged for scheduled audits.
3. Zero-Trust Commercial Transparency & Non-Retaliation (Rule 59)
All procurement evaluations, factory performance indexes, and milestone settlements are governed by immutable ground-truth audit trails. In accordance with platform governance, commercial disagreements or quality defect claims are adjudicated strictly on verified data (ISO 2859-1 AQL inspection seals, spectrophotometer lab dips, and signed auditor records). Submitting an audit discrepancy claim will never result in retaliatory blacklisting or arbitrary reputation degradation.
4. Intellectual Property, CAD Assets & Tech-Pack Protections
All design dossiers, vector pattern files (Clo3D, Gerber, Lectra), grade rules, and buyer Bill of Materials (BOM) uploaded to Leadirftex remain the exclusive intellectual property of the originating client. Participating suppliers and garment factories receive a strictly limited, single-order production license. Unauthorized replication, cross-facility design dissemination, or utilization of proprietary patterns for machine learning model training is strictly prohibited.
5. Platform Disclaimers & Industrial Telemetry Standards
Telemetry harvested through machine line sensors, digital QMS consoles, and NPT stoppage monitors provides real-time operational visibility via LX Intelligence. Participating facilities agree to maintain accurate telemetry sensor calibrations and agree not to simulate, fabricate, or manipulate IoT metrics. While Leadirftex provides rigorous algorithmic insights, final manufacturing execution and ex-factory ship dates remain the direct contractual responsibility of transacting parties.
6. Zero-Cost Talent Layer Guidelines
The Leadirftex talent matching layer and CV Builder service are structured as accessible, barrier-free infrastructure for apparel technicians, mechanics, and floor supervisors. Participating factories, recruitment agencies, and third-party intermediaries are strictly prohibited from charging placement fees, deductions, or mandatory recruiter commissions from applicants placed through this ecosystem.
7. Escrow, Order Settlement & Dispute Resolution
Commercial B2B transactions executed via Leadirftex Interchain escrow vaults are released conditionally based on predefined stage gates (fabric lab dip approval, inline AQL 1.5 audit pass, final container loading inspection). Any commercial disputes, quantity shortages, or specification variances are arbitrated through verified multi-sig audit logs and formal inspection certificates.
8. Jurisdiction & Legal Inquiries
These terms and all commercial interactions mediated by the platform are governed by international commercial trade law and standard ICC arbitration practices. For formal legal notices, contract interpretations, or arbitration filings, contact our Legal Operations Group:
Leadirftex Enterprise Legal Framework • Attn: General Counsel